

Submitted:
09 October 2026
Posted:
10 October 2026
You are already at the latest version
Abstract
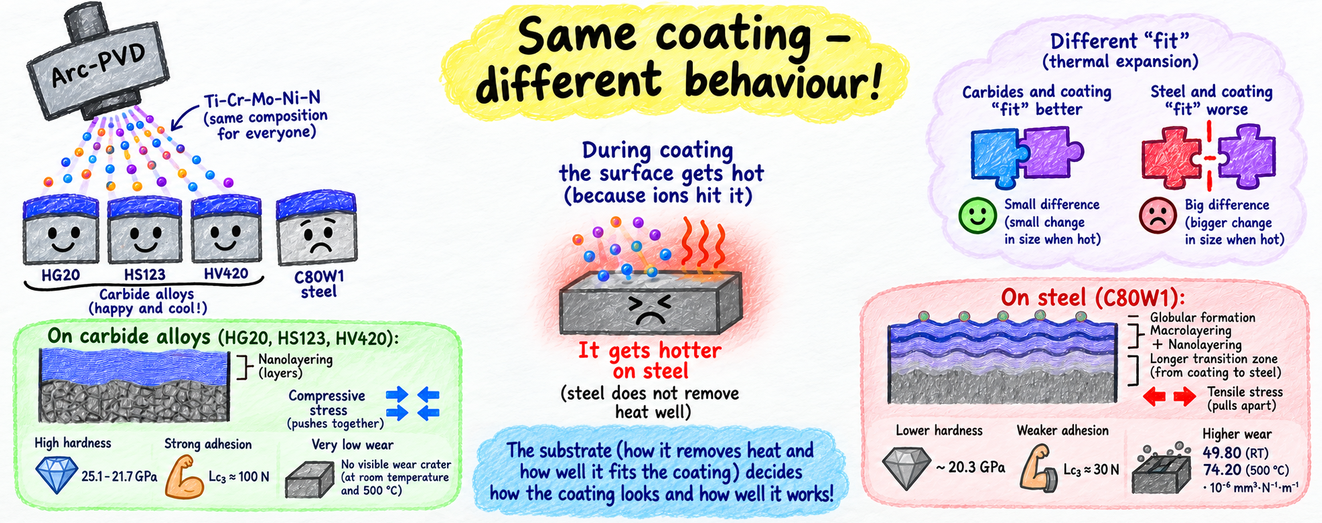
The arc-PVD Ti–Cr–Mo–Ni–N coatings on HG20, HS123, HV420 carbide alloys and C80W1 tool steel, while having approximately the same elemental and phase compositions, differ in morphology, macrostructure, and level of macrostresses. When deposited on steel, the coating exhibits macrolayering, a more extended coating–substrate transition zone, and develops tensile macrostresses, in contrast to the coatings on carbide alloys, which develop compressive macrostresses. The behaviour can be explained by the overheating of the coating during deposition, which results from ion bombardment and is more pronounced on steel due to its poorer thermal diffusivity relative to carbide alloys. The CLTE difference between steel and the coating is significantly larger than that between the carbides and the coating, further contributing to the effect. It was found that, considering these features, the Ti–Cr–Mo–Ni–N coating on steel exhibits lower hardness (~20.3GPa), lower adhesion strength to the substrate (Lc3≈30N, the indenter load at scratch testing corresponding to the onset of coating wear), and a higher wear intensity at room temperature and 500°C (49.80 and 74.20·10−6 mm3·N−1·m−1, respectively), as compared with the hardness values of 25.1–21.7GPa, Lc3≈100N, and wear intensity (corresponding to the absence of a visible wear crater) for the Ti–Cr–Mo–Ni–N coatings on the aforementioned carbide alloys.
Keywords:
Arc-PVD coating
; Ti-Cr-Mo-Ni-N system
; carbide substrates
; steel C80W1
; macrostresses
; wear
1. Introduction
Coatings based on Cr, Mo and Ti nitrides exhibit high physico-mechanical properties, which ensure their relatively high wear resistance [1,2,3,4,5]. However, single-phase coatings of these systems have significant drawbacks that limit their application:
- The relatively low hardness of Cr–N-based coatings, combined with a high friction coefficient, promotes greater heat generation in the contact zone, thereby reducing the performance efficiency and service life of components [9].
- These coatings are characterised by a columnar structure. Along the boundaries of columnar crystallites, oxygen rapidly diffuses towards the substrate surface, lowering their heat resistance. Moreover, the columnar morphology is more conducive to crack propagation into the coating depth than an equiaxed (isomorphic) structure, thus reducing the adhesion strength of the substrate–coating composite [10,11,12].
The use of ternary Me–Me′–N systems, in which both metallic elements form nitrides with a face-centered cubic (FCC) lattice that are mutually soluble, significantly improves the coating properties. For example, reference [6] demonstrated that ion-plasma vacuum-arc Ti–Cr–N coatings with chromium concentrations ranging from 10.1 to 25.2 at.% exhibit higher hardness than CrN coatings. At the same time, chromium-rich coatings show better wear resistance in aggressive environments. According to the findings in [13], alloying with chromium raises the oxidation resistance temperature of TiN coatings by over 100 °C. Another example of ternary coatings based on mutually soluble nitride phases is the Cr–Mo–N system. According to [14], the maximum molybdenum concentration at which a (Cr,Mo)N solid solution forms is 30.4 at.%; upon dissolution of molybdenum in chromium nitride, hardness increases due to solid-solution strengthening and an increase in residual macrostresses in the coating, reaching a maximum of 34 GPa at 21 at.% Mo. The system attracts considerable attention due to the excellent tribological properties of molybdenum nitride. Indeed, when a (Cr,Mo)N solid solution forms, the friction coefficient declines as the molybdenum fraction increases. For CrN/Mo2N multilayers, raising the temperature from ambient to 300 °C causes the friction coefficient to approximately double, a phenomenon attributed to the generation of hard wear debris, including CrN, Mo2N, and Cr2O3 particles. At 600 °C, however, the friction coefficient drops to 0.53, which is ascribed to the appearance of a Magnéli phase (MoO3) that provides solid-lubricant action. Moreover, these coatings exhibit a 300 °C improvement in thermal resistance relative to single-phase Mo2N coatings, thanks to the protective CrN layers that act as an oxidation barrier for molybdenum nitride. In some instances, the wear resistance of CrN/Mo2N coatings is six-fold greater than that of CrN and double that of Mo2N.
One effective alternative for enhancing surface functionality is to replace the TiN system with Ti–Mo–N. It has been shown [15] that they have a lower friction coefficient and wear rate than single-phase TiN. The increase in hardness is associated with the refinement of nitride grains – it is known that titanium and molybdenum nitrides are practically insoluble in each other [16]; accordingly, during coating deposition, competitive growth of TiN and Mo2N grains occurs, which block each other. Introducing into the system a nitride-forming metal that does not tend to form nitrides is one of the effective and well-known methods for synthesising “superhard” coatings [17,18,19,20,21]. Such coatings include the ZrN–Ni(Cu), Cr2N–Ni, TiN–Ni(Cu) systems, etc. The presence of a metallic component in such systems leads not only to an increase in hardness due to the refinement of nitride grains down to several nanometres in size, but also to an increase in impact toughness. As the concentration of the metallic component increases, the columnar structure characteristic of nitride coatings becomes finer, up to the formation of an equiaxed structure – with a thin metallic or amorphous interlayer formed around the nitrides. Thereby, a dispersion-strengthened structure is realised, where the matrix is a soft and ductile metal. In the Ti-N-Ni system, the hardness increases by more than a factor of two at 12 at.% Ni, with a grain size of 15–18 nm, compared with single-phase TiN coatings [22]. A significant synergistic effect in improving coating properties is observed for five-component coatings based on the Ti–Cr–Ni–Mo–N system. Thus, the study found a substantial increase in the wear resistance of coatings of this system on the nickel alloy ÉK61 and on silicon, compared with Ti–Cr–N and Ti–Cr–N–Ni coatings [23]. [24] showed that Cr–Ti–Al–Mo–N coatings exhibited higher hardness (29.3 GPa) and better wear resistance (1.2 × 10⁻¹⁶ m3/(N·m)) than CrTiMoN, TiMoN and CrTiAlN coatings. In work [25], the authors, when investigating Al–Ti–N and Al–Ti–Cr–Mo–N coatings deposited by cathodic arc evaporation (CAE) on carbide alloy (WC–Co, 7 wt.% Co), found that at high hardness values (35.6 ± 1.5 GPa), the coatings of the first system had significantly lower H/E and H3/E2 parameters (0.059 and 0.124 GPa, respectively) than the coatings of the second system (0.071 and 0.157 GPa, respectively). These differences resulted in an almost three-fold increase in the wear resistance of the Al–Ti–Cr–Mo–N coatings compared with the Al–Ti–N coatings. The above indicates a considerable effectiveness of five-component coatings based on the Ti–Cr–Mo–N system with the addition of Ni and Al as strengthening elements under various friction conditions. At the same time, when choosing strengthening coatings for different materials, as individual studies show, one should take into account that the nature of the substrate can significantly affect the properties of both the coatings and the coating–substrate composite as a whole. [26] demonstrated the influence of different grades of carbide alloys with different cobalt contents on the processes of crack initiation and propagation was established, due to different macro-stress values arising in them. The effect of carbide alloy compositions on abrasive erosion resistance and on coating wear resistance was confirmed by the authors of [27, 28]. The aim of this study is to determine the influence of substrate materials made of different grades of carbide alloy and tool steel on the structure and properties of Ti–Cr–Ni–Mo–N coatings.
2. Materials and Experiments
The Ti–Cr–Mo–Ni–N coatings were produced by ion-plasma vacuum-arc evaporation using a three-cathode system. The cathodes were prepared from a Ti–Ni alloy (50 at.%), Mo, and Cr, which were installed in evaporators C1, C2, and PI (Figure 1), respectively (C1 and C2 are evaporable cathodes with droplet phase separators, while PI is a direct-flow evaporable cathode).
The deposition time was 90 minutes. Nitrogen served as the reactive gas. Substrate heating to 400 °C was performed indirectly. The coated substrates rotated around both the evaporating cathodes and their own axes. The reactive gas pressure (PN2 was approximately 3 · 10−1 Pa. The current on the Ti–Ni and Mo cathodes (Ia) was about 100 A, and about 90 A on the Cr cathode. The bias voltage applied to the substrates (Uc) was about 120 V. Prior to deposition, the substrate materials were ion-etched. The resulting coating thickness was 4 ± 0.1 μm. Deposition parameters for all substrates were selected to maximise the deposition rate while minimising the droplet phase content in the coatings
Three carbide alloys grades were selected as substrate materials: WC–Co (6 wt.%) (HG20); WC–TiC (15 wt.%)–Co (6 wt.%) (HS123); and WC–TiC (4 wt.%)–TaC (6 wt.%)–Co (8 wt.%) (HV420) – the grades most widely used for tool and structural applications – together with carbon tool steel C80W1 (C: 0.81–0.89; Si: 0.17–0.33; Mn: 0.33–0.58; Ni: up to 0.25; S: up to 0.028; P: up to 0.03; Cr: up to 0.2; Cu: up to 0.25 wt.%).
Coating thicknesses on various substrates ranged between 3.9 and 4.1 µm.
Morphological features were assessed using a Vega 3SB scanning electron microscope (Tescan, Czech Republic) equipped with an X-ACT SDD energy-dispersive X-ray spectrometer (Oxford Instruments, UK). Microstructure was examined with a JEM-2100 transmission electron microscope (JEOL, Japan) operating in microdiffraction mode, which provided electron diffraction patterns for phase identification. For this purpose, lamellae were prepared from the coatings by ion thinning. Chemical states and elemental compositions were determined by X-ray photoelectron spectroscopy on a Versa Probe II spectrometer (Physical Electronics, USA). Phase composition was further verified by X-ray diffraction on an Ultima IV diffractometer (Rigaku Corporation, Japan) with Cu Kα radiation and a graphite monochromator, using an asymmetric scanning geometry (5° incidence angle). Coherent scattering domain sizes (D), lattice microstrains (ε), and the complex nitride lattice parameter were calculated from (111) and (222) reflections recorded in symmetric geometry. Physical peak broadening was extracted by jointly fitting the specimen against a reference germanium powder (10–20 µm) using pseudo-Voigt functions.
Hardness and elastic modulus for the Ti–Cr–Ni–Mo–N coatings were determined by the Oliver–Pharr method [29] using a Micro-Hardness Tester (CSM Instruments, Switzerland) at a 25 mN load. The plastic deformation work fraction, derived from load–displacement curves, served as a fracture toughness indicator [30]. Indentation depth never exceeded 10 % coating thickness to avoid substrate interference, in line with ISO/CD 14577.
Tribological properties were studied with a Tribometer (Nanovea, USA) in a pin-on-disk configuration at 20 °C and 500 °C in air. The counterbody was an alumina ball; the normal load was 5 N, sliding speed 10 cm/s, sliding distance 100 m, and track radius 3 mm. Wear rates were measured by optical profilometry using a WYKO NT1100 instrument (Veeco, USA).
Coating adhesion and cohesive strength were evaluated by progressive-load scratch testing up to 100 N on a Revetest instrument (CSM Instruments, Switzerland). Acoustic emission, tangential force, and friction coefficient were recorded to determine critical loads Lc1, Lc2, and Lc3 – corresponding to first cracking, adhesive delamination, and substrate exposure under cohesive failure, respectively [31]. Substrate exposure was additionally confirmed by colour changes at the scratch-track bottom and by a sudden friction-force jump; failure morphology was examined by optical microscopy.
Macrostresses arising from differential thermal expansion and structural inhomogeneities were calculated using the Stoney equation [32,33,34]. Substrate curvature radii before and after deposition were measured with an optical profilometer. Layer thicknesses were determined from cross-sectional SEM images. The curvature radius was computed as:
where L – the specimen length and b – the deflection sagitta.
3. Results and Discussion
1. Structure and substructure characteristics, elemental and phase composition – for coatings deposited on carbide alloys and tool steel substrates.
Figure 2 presents Ti–Cr–Mo–Ni–N coating micrographs grown on various substrate compositions.
Morphological analysis shows that coatings deposited on carbide alloy and steel substrates exhibit a reticulated surface texture. The so-called reticulated texture consists of numerous cells. This texture results from the deposited layer replicating substrate roughness created during sandblasting prior to deposition. On steel substrates (Figure 2d), however, globular formations appear along cell ridges, which can be explained by steel’s much lower thermal diffusivity (13 m2·s−1·106) versus that of carbide alloy substrates (32, 23, and 19 m2·s−1·106 for HG20, HS123, and HV420, respectively) [35,36,37,38]. This leads to a lower cooling rate for the growing coating on steel and thus a possible vapour–liquid–solid phase transition, whereas on carbide alloy substrates coating formation proceeds via a vapour–solid transition. The globule formation on cell ridges is predetermined by more restricted heat removal from these surface regions compared with that from cell sidewalls. Additionally, step-like surface areas appear on steel substrates, indicating a macro-layered coating structure. This feature can be attributed to the steel substrate’s coefficient of linear thermal expansion (CLTE) (14.3·10−6 K−1) [39] being roughly twice that of the Ti–Cr–Mo–Ni–N coating (8.3·10−6 K−1, estimated by the rule of mixtures [40,41]). Notably, the differences between the coating’s CLTE and those of the carbide substrates are much smaller: 3.6–5.0, 5.5–6.0, and 5.5–6.0·10−6 K−1 for HG20, HS123, and HV420, respectively [42,43]. This contrasts with the carbide substrates, where the coating’s CLTE exceeds the substrate’s.
Such CLTE mismatch between the coating and the steel substrate can generate tensile thermal stresses [44], which, at a certain growth stage, rupture the growing layer. This rupture exposes fresh surface where new coating phase nuclei form and grow, producing a new layer.
Table 1 presents EDX chemical composition data for the Ti–Cr–Mo–Ni–N coatings. The results indicate that the coating elemental composition is essentially substrate-independent, within the experimental error.
X-ray phase analysis data (Figure 3, refined by XPS, indicate that the Ti–Cr–Mo–Ni–N coating composition includes Ti1₋ₓCrₓN nitride, γ-Mo2N, and Ni.
Molybdenum in the γ-Mo2N form is confirmed by two independent methods. First, the diffraction pattern (Figure 3) shows peak asymmetry indicating this compound. Second, XPS (Figure 4) places Mo3d5/2 and N1s binding energies at 228.1 and 397.4 eV, characteristic of the γ-Mo2N nitride phase [45].
Titanium and chromium nitride sublayers with cubic lattice, deposited prior to the molybdenum-containing layer, stabilise the γ-Mo2N phase. The Ti2p3/2 binding energy (Figure 5) across the ~170 nm profile remains at 455.3 eV, which is 1.1 eV below the tabulated value for stoichiometric TiN (456.4 eV) [46].
Redistributed ionic–covalent–metallic bonds point to a complex (Ti,Cr)N nitride with B1 structure, typical for TiN and CrN. XPS spectra (Figure 5) exhibit two Cr2p lines: Cr2p3/2 at 574.9 eV and Cr2p1/2 at 584.4 eV. This confirms CrN phase [45,46] – formed as substrates pass the chromium cathode – and (Ti,Cr)N, which forms as overlapping vapor fluxes from TiNi and Cr cathodes condense.
Although X-ray diffraction detects no Ni-bearing phases in Ti–Cr–Mo–N–Ni coatings, XPS (Figure 6) shows a Ni binding energy near 852.4 eV, characteristic solely of metallic Ni [47].
The observed features are attributed to nickel’s much lower thermodynamic probability for bonding with nitrogen compared with the other coating elements [48,49,50,51]. Combined with nickel’s extremely low solubility in nitrides and the absence of clear diffraction peaks, this supports the view that nickel exists as an X-ray amorphous component – consistent with results reported in [22].
Ti–Cr–Mo–Ni–N coating substructure characteristics for the titanium-based nitride phase are listed in Table 2. A notable lattice parameter decrease is observed for the titanium nitride-based phase on all substrates, compared with stoichiometric TiN [52].
This confirms solid solution formation – chromium in titanium nitride – during coating deposition, where the lattice parameter should decrease given the Ti and Cr atomic radii ratio. Moreover, the determined average nitride phase lattice parameters match literature data [53] for Cr-in-TiN solid solutions at concentrations corresponding to those elements in our coatings. Simultaneously, the titanium-nitride-based phase exhibits large microstrains, whose origin lies in structural defects and compositional inhomogeneity. Their lowest values occur for coatings deposited on HG20 carbide alloy. As Table 2 shows, microstrain growth accompanies lattice parameter increases for the corresponding phases, consistent with published data. Significant microstrains alongside relatively small CSD sizes rather suggest that most strain arises from nonuniform component distribution. If crystal structure defects were the sole strain source, their density would have to exceed 1012 cm−2, which is physically improbable.
TEM structure studies reveal that Ti–Cr–Mo–Ni–N coatings on all tool material substrates form multilayer structures with a ~70 nm modulation period (Figure 7). Individual crystallites grow through several layers.
Owing to the substrate–coating thermal expansion mismatch noted above, together with possible compositional and structural heterogeneities arising in growing PVD coatings [54,55], compressive or tensile macrostresses typically develop [56], noticeably affecting the overall coating–substrate composite properties [57,58,59,60]. Accordingly, their values were estimated by the Stoney method. Table 3 lists the obtained results.
σcalc – calculated macrostress;
R0 – substrate curvature radius before deposition;
R – coating–substrate composite curvature radius;
tₛ – substrate thickness;
tf – coating thickness;
νₛ – substrate Poisson’s ratio;
Eₛ – substrate elastic modulus.
The results show tensile stresses developing in the coating on steel substrate. Compressive stresses, roughly equal in magnitude, occur in coatings on carbide alloy substrates. The calculated tensile macrostress values for the Cr–Ti–Ni–Mo–N coating on tool steel confirm the earlier inference that such stresses are likely here, given the substrate CLTE substantially exceeding the coating CLTE, and this factor’s effect on coating morphology – manifesting as macrolayering.
To assess how compositional inhomogeneity at the coating–substrate interface – arising from mutual diffusion between coating and substrate components – might affect structural stresses and their contribution to the integral macrostress value, a study was performed on the diffusion transition zone. TEM imaging of near-interface regions and local X-ray microanalysis were employed. Depth determination error corresponded to half the local analysis zone diameter. For the Cr–Ti–Ni–Mo–N coating on carbide alloys, the transition zone was defined by the diffusion depth for Cr, Ni, and Mo (coating elements) into the substrate and for W (substrate element) into the coating; on C80W1 steel, by the diffusion depth for Cr, Ni, and Mo into the substrate and for Fe into the coating. The resulting TEM images and local elemental microanalysis data for the coating–substrate transition zones are presented in Figure 8.
Estimated values for the coating–substrate diffusion transition zones were obtained by processing the experimental data. These are listed in Table 4. As the results show, the largest zone corresponds to C80W1 steel substrates
This is attributed both to the higher diffusion mobility (diffusion coefficients D at temperatures reached in the coating–substrate contact zone) for iron atoms in the carbide alloy phases and coating elements in iron, compared with the mutual diffusion mobility for the marker elements (listed above) in Ti–Cr–Mo–Ni–N coatings and carbide substrates [61,62,63,64,65], and to local interface heating during deposition. This is also due to more efficient heat accumulation in the growth zone, since steel removes heat less effectively than carbide alloy substrates. Evidence for this effect comes from the temperature field simulation results presented in [28] for analogous-composition substrates and growing coatings under high-energy particle flux during arc-PVD Ti–Al–Ni–N deposition. Those simulations showed that the highest surface and coating-interior temperatures occur for the lower-thermal-diffusivity material – C80W1 steel. For the Ti–Cr–Mo–Ni–N coating, this effect may be even stronger, given the presence of heavy molybdenum particles bombarding the substrate and the correspondingly greater energy transferred to the growing coating, according to:
where Z – the mean particle charge in the plasma flux; U – the substrate bias potential; e – the electron charge; U0 (eV) – the initial ion energy in the arc-generated plasma used for cathode evaporation [66,67]. For Mo ions, U0 and Z exceed those for Al and Ti – the main Ti–Al–Ni–N coating constituents [68,69].
E(U) = U∙Z∙e + Uo eV
2. Physical–mechanical, tribological, and adhesion to substrate properties for Ti–Cr–Mo–Ni–N coatings deposited on different substrates.
The values for hardness (H), elastic modulus (E), relative plastic deformation work (Wₚ), and the H/E and H3/E2 ratios – which characterise material resistance to elastic and plastic deformation [70, 71] – are listed in Table 5.
The results show that coatings on carbide alloy substrates exhibited higher H and E values than those on C80W1 steel. At the same time, the H/E and H3/E2 ratios for coatings on tool steel were maximal. The Wₚ value, which serves as a fracture toughness indicator [30], shows that this property is more pronounced for Ti–Cr–Mo–Ni–N coatings formed on carbide alloy substrates. The lower hardness on tool steel may stem from tensile macrostresses in this substrate – due to the substrate CLTE being nearly twice that of the coating, as noted above – as well as from compositional inhomogeneities in the substrate–coating near-interface regions, which arise depending on the deposited material and substrate nature [1, 57, 58].
Investigations into adhesion strength for Ti–Cr–Mo–Ni–N ceramic-metal coatings on various tool materials revealed a cohesive failure mode for all coating–substrate composites studied. Since the processes during abrasive particle penetration resemble those in controlled scratch testing with an indenter [72,73], this method is regarded as a model for hard abrasive sliding over a surface under increasing load. Figure 9 and Figure 10 present typical scratch-test results for Ti–Cr–Mo–Ni–N coatings on various tool substrates: friction force (Ff), friction coefficient (μ), and acoustic emission (AE) curves, along with scratch micrographs produced by indenter sliding under increasing load.
At room temperature, all Ti–Cr–Mo–Ni–N coatings on every substrate exhibited a similar friction coefficient (~0.5), but they differed in wear rate. Coatings deposited on carbide alloys showed wear craters whose profile allowed wear depth estimation; this depth was comparable to the initial coating surface roughness (Figure 11a). In contrast, the coating on steel exhibited a substantially higher wear rate (Figure 11b).
The obtained tribological test results are somewhat at odds with several studies showing that high H/E and H3/E2 values govern enhanced coating wear resistance [77,78,79]. Indeed, the highest wear rate belongs to the C80W1-coating composite, which exhibits maximum H/E and H3/E2 values (Table 5). This apparent contradiction likely stems from different wear failure mechanisms for this composite versus the carbide alloy–Ti–Cr–Mo–Ni–N coating composites. For the coating on steel substrate, failure proceeds via delamination of the macrolayers present in the coating structure, as revealed by morphology studies. The likelihood of such a structure forming on this substrate was discussed above. Wear track examination for carbide alloys specimens with the Ti–Cr–Mo–Ni–N coating confirms that wear occurs by small fragment detachment from the coating within the track and along its edges (Figure 12a). In contrast, the wear track for the coating deposited on steel (12b) shows features indicative of wear through plastic deformation via macrolayer displacement within the coating structure.
At 500 °C, Ti–Cr–Mo–Ni–N coatings on carbide alloys show some increase and similar friction coefficients ~0.54–0.59 (Table 6), with noticeable wear debris transfer from the counterbody onto the track surface, hindering wear rate measurement. The coating on steel shows a slight friction coefficient decrease at 500 °C (to 0.47 vs. 0.53) accompanied by a higher wear rate (Figure 11b, d). The lower friction coefficient for Ti–Cr–Mo–Ni–N coatings on steel stems from their macrolayered structure, described earlier when discussing coating morphology on this substrate, and the resulting decrease in their shear strength due to poor interlayer adhesion, which reduces friction force [75]. The higher friction coefficients for Ti–Cr–Mo–Ni–N coatings on carbide alloy substrates at high temperature can be explained by chromium being the main coating element; its oxidation in air during high-temperature tribological tests forms Cr2O3-based wear debris, which acts as an abrasive in the contact zone and raises friction force [80]. Molybdenum present in the coating, which according to our and others’ studies should improve tribological performance at high temperature through MoO3 lubricious phase formation [81,82,83,84,85], here has no significant effect due to its low content (~4 at.%) against high chromium (~35 at.%).
4. Conclusions
Analysis of structure and properties for Ti–Cr–Mo–Ni–N ceramic-metal coatings on various tool substrates revealed a difference in coating morphology on tool steel versus carbide-based substrates – namely, the appearance of globular formations. This is attributed to hindered heat removal from the ion flux bombarding the substrate, due to steel’s lower thermal diffusivity compared with the carbide alloys used. This leads to a lower cooling rate for the growing coating on steel and thus a possible vapour-liquid-solid phase transition, whereas on carbide alloy substrates coating formation proceeds via a vapour-solid transition. Additionally, these coatings show stepped surface areas, indicating a macrolayered structure. This difference likely results from tensile thermal stresses (in contrast to coatings on carbide alloys), which at a certain growth stage rupture the growing layer, exposing fresh surface where new coating phase nuclei form and grow, producing a new layer. The same reason may explain the relatively lower hardness for the coating on steel (20.3 ± 1.1 GPa) compared with coatings on carbide substrates (25.1 ± 2.2 – 21.7 ± 1.1 GPa).
Relatively low adhesion strength was found for the coating on tool steel versus coatings on carbide alloy substrates. This effect stems from tensile macrostresses in the former case and from the coating morphology on tool steel – its macromultilayer nature, which reduces shear strength. At the same time, the latter may account for the relatively lower friction coefficient for this coating compared with carbide-based coatings.
The studied coatings exhibit good tribological performance both at room and elevated temperatures – relatively low wear rates, with the highest wear rate for the coating on tool steel.
Considering the functional property study for Ti–Cr–Mo–Ni–N coatings on various tool substrates, it can be concluded that they may be effectively used as strengthening coatings on carbide alloys belonging to the HG20, HS123, and HV420 groups. Their effectiveness on carbon tool steel would be reduced due to lower hardness, weaker substrate adhesion, and higher wear rate.
Declaration: of competing interest
The authors declare that they have no known competing financial interests or personal relationships that could have appeared to influence the work reported in this paper.
Acknowledgments
This work was supported by the Ministry of Science and Higher Education of the Russian Federation (state assignment, project no. FSME-2026-0008).
Data availability
Data will be made available on request.
References
- D. Dinesh Kumar, N. Kumar, S. Kalaiselvam, S. Dash, R. Jayavel, Substrate effect on wear resistant transition metal nitride hard coatings: microstructure and tribomechanical properties, Ceram. Int. 41 (2015) 9849–9861. [CrossRef]
- V.N. Zhitomirsky, I. Grimberg, L. Rapoport, R.L. Boxman, N.A. Travitzky, S. Goldsmith, B.Z. Weiss, Bias voltage and incidence angle effects on the structure and properties of vacuum arc deposited TiN coatings, Surf. Coat. Technol. 133–134 (2000) 114–120. [CrossRef]
- C. Lorenzo-Martin, O. Ajayi, A. Erdemir, G.R. Fenske, R. Wei, Effect of microstructure and thickness on the friction and wear behavior of CrN coatings, Wear 302 (2013) 963–971. [CrossRef]
- F. Ferreira, J.C. Oliveira, A. Cavaleiro, CrN thin films deposited by HiPIMS in DOMS mode, Surf. Coat. Technol. 291 (2016) 365–375. [CrossRef]
- Jauberteau, A. Bessaudou, R. Mayet, J. Cornette, J. Jauberteau, P. Carles, T. Merle-Méjean, Molybdenum nitride films: crystal structures, synthesis, mechanical, electrical and some other properties, Coatings 5 (2015) 656–687. [CrossRef]
- M. Akbarzadeh, A. Shafyei, H.R. Salimijazi, Characterization of TiN, CrN and (Ti,Cr)N coatings deposited by cathodic arc evaporation, Int. J. Eng. 27 (2014) 1127–1132. [CrossRef]
- N. Solak, F. Ustel, M. Urgen, S. Aydin, A.F. Cakir, Oxidation behavior of molybdenum nitride coatings, Surf. Coat. Technol. 174–175 (2003) 713–719. [CrossRef]
- G. Gassner, P.H. Mayrhofer, K. Kutschej, C. Mitterer, M. Kathrein, Magnéli phase formation of PVD Mo–N and W–N coatings, Surf. Coat. Technol. 201 (2006) 3335–3341. [CrossRef]
- Z.K. Chang, X.S. Wan, Z.L. Pei, J. Gong, C. Sun, Microstructure and mechanical properties of CrN coating deposited by arc ion plating on Ti6Al4V substrate, Surf. Coat. Technol. 205 (2011) 4690–4696. [CrossRef]
- Y.H. Yoo, D.P. Le, J.G. Kim, S.K. Kim, P.V. Vinh, Corrosion behavior of TiN, TiAlN, TiAlSiN thin films deposited on tool steel in the 3.5 wt.% NaCl solution, Thin Solid Films 516 (2008) 3544–3548. [CrossRef]
- N.D. Nam, M. Vaka, N.T. Hung, Corrosion behavior of TiN, TiAlN, TiAlSiN-coated 316L stainless steel in simulated proton exchange membrane fuel cell environment, J. Power Sources 268 (2014) 240–245. [CrossRef]
- A.S.M.A. Haseeb, M.M. Rahman, M.A. Maleque, Coating and surface modification of metals, in: Handbook of Materials Failure Analysis with Case Studies from the Chemicals, Concrete, and Power Industries, Elsevier, 2016, pp. 289–304. [CrossRef]
- H. Chen, G. Yuan, High-temperature oxidation behavior of (Ti,Cr)N coating deposited on 4Cr13 stainless steel by multi-arc ion plating, Rare Met. Mater. Eng. 43 (2014) 1084–1087. [CrossRef]
- K.H. Kim, E.Y. Choi, S.G. Hong, B.G. Park, J.H. Kim, Syntheses and mechanical properties of Cr–Mo–N coatings by a hybrid coating system, Surf. Coat. Technol. 201 (2006) 4068–4072. [CrossRef]
- K.V. Chauhan, S.K. Rawal, A review paper on tribological and mechanical properties of ternary nitrides base coatings, Procedia Technol. 14 (2014) 430–437. [CrossRef]
- Scientific Group Thermodata Europe (SGTE), Ternary Alloy Systems, Springer, Berlin, 2010.
- J. Musil, P. Karvankova, J. Kasl, Hard and superhard Zr–Ni–N nanocomposite films, Surf. Coat. Technol. 139 (2001) 101–109. [CrossRef]
- S. Veprek, G.J. Veprek-Heijman, P. Karvankova, J. Prochazka, Different approaches to superhard coatings and nanocomposites, Thin Solid Films 476 (2005) 1–29. [CrossRef]
- P. Karvaňková, H.-D. Männling, C. Eggs, S. Veprek, Thermal stability of ZrN–Ni and CrN–Ni superhard nanocomposite coatings, Surf. Coat. Technol. 146–147 (2001) 280–285. [CrossRef]
- L. Zhang, G.J. Ma, G.Q. Lin, K.C. Han, H. Ma, Synthesis of Cu doped TiN composite films deposited by pulsed bias arc ion plating, Nucl. Instrum. Methods Phys. Res. B 320 (2014) 17–21. [CrossRef]
- Akbari, J.P. Riviere, C. Templier, E. Le Bourhis, Structural and mechanical properties of IBAD deposited nanocomposite Ti–Ni–N coatings, Surf. Coat. Technol. 200 (2006) 6298–6302. [CrossRef]
- D.S. Belov, I.V. Blinkov, A.O. Volkhonskii, The effect of Cu and Ni on the nanostructure and properties of arc-PVD coatings based on titanium nitride, Surf. Coat. Technol. 260 (2014) 186–197. [CrossRef]
- Chernogor, F. Klimashin, A. Volkhonskii, I. Blinkov, P. Mayrhofer, The impact of Ni and Mo on growth-morphology and mechanical properties of arc evaporated Ti–Cr–N hard coatings, Surf. Coat. Technol. 377 (2019) 124917. [CrossRef]
- T. Wang, G. Zhang, B. Jiang, Comparison in mechanical and tribological properties of CrTiAlMoN and CrTiAlN nano-multilayer coatings deposited by magnetron sputtering, Appl. Surf. Sci. 363 (2016) 217–224. [CrossRef]
- Y.-Y. Chang, C.-C. Chuang, Deposition of multicomponent AlTiCrMoN protective coatings for metal cutting applications, Coatings 10 (2020) 605. [CrossRef]
- R. Stylianou, D. Velic, W. Daves, W. Ecker, A. Stark, N. Schell, M. Tkadletz, N. Schalk, C. Czettl, C. Mitterer, Stress relaxation through thermal crack formation in CVD TiCN coatings grown on WC–Co with different Co contents, Int. J. Refract. Met. Hard Mater. 86 (2020) 105102. [CrossRef]
- M.Š. Musa, M. Sakoman, D. Ćorić, T. Aleksandrov Fabijanić, Exploitation and wear properties of nanostructured WC–Co tool modified with plasma-assisted chemical vapor deposition TiBN coating, Metals 11 (2021) 333. [CrossRef]
- D.S. Belov, A.P. Demirov, I.V. Blinkov, V.S. Sergevnin, A.V. Chernogor, P.V. Kiryukhantsev-Korneev, V.N. Anikin, Structure and properties features of CA-PVD Ti–Al–Ni–N coatings deposited on carbide alloys and tool steel substrates, Surf. Coat. Technol. 494 (2024) 131348. [CrossRef]
- W.C. Oliver, G.M. Pharr, An improved technique for determining hardness and elastic modulus using load and displacement sensing indentation experiments, J. Mater. Res. 7 (1992) 1564–1583. [CrossRef]
- Y. Zhou, R. Asaki, W.-H. Soe, R. Yamamoto, R. Chen, A. Iwabuchi, Hardness anomaly, plastic deformation work and fretting wear properties of polycrystalline TiN/CrN multilayers, Wear 236 (1999) 159–164. [CrossRef]
- P. Henry, M.-J. Pac, C. Rousselot, M.-H. Tuilier, Wear mechanisms of titanium and aluminium nitride coatings: a microtribological approach, Surf. Coat. Technol. 223 (2013) 79–86. [CrossRef]
- G.G. Stoney, The tension of metallic films deposited by electrolysis, Proc. R. Soc. Lond. Ser. A 82 (1909) 172–175.
- Y. Zhao, S. Chen, Y. Chen, S. Wu, W. Xie, W. Yan, S. Wang, B. Liao, S. Zhang, Super-hard and anti-corrosion (AlCrMoSiTi)Nx high entropy nitride coatings by multi-arc cathodic vacuum magnetic filtration deposition, Vacuum 195 (2022) 110685. [CrossRef]
- L. Zhang, H. Yang, X. Pang, K. Gao, A.A. Volinsky, Microstructure, residual stress, and fracture of sputtered TiN films, Surf. Coat. Technol. 224 (2013) 120–125. [CrossRef]
- J.R. Davis (Ed.), ASM Specialty Handbook: Tool Materials, ASM International, Materials Park, OH, 1995.
- B. Schultrich, W. Poeßnecker, Thermal conductivity of cemented carbides, J. Therm. Anal. 33 (1988) 305–310. [CrossRef]
- S. Wen, Y. Du, J. Tan, Y. Liu, P. Zhou, J. Long, et al., A novel physical model for describing thermal conductivity of composite materials: application to the measured values in a two-phase WC–Co system, Acta Mater. (2020). [CrossRef]
- S. Wen, Y. Du, J. Tan, Y. Liu, P. Zhou, J. Long, et al., A new model for thermal conductivity of “continuous matrix/dispersed and separated 3D-particles” type composite materials and its application to WC–M (M = Co, Ag) systems, J. Mater. Sci. Technol. 97 (2022) 123–133. [CrossRef]
- K. Hirukawa, K. Akita, S. Tobe, T.A. Stolarski, S. Ohya, X-ray residual stress measurements on plasma sprayed molybdenum coatings, WIT Trans. Built Environ. 85 (2006) 7. [CrossRef]
- Y. Hirata, T. Shimonosono, Mixing rules of Young’s modulus, thermal expansion coefficient and thermal conductivity of solid material with particulate inclusion, J. Korean Ceram. Soc. 53 (2016) 43–49. [CrossRef]
- R.A. Schapery, Thermal expansion coefficients of composite materials based on energy principles, J. Compos. Mater. 2 (1968) 380–404. [CrossRef]
- S.A. Humphry-Baker, J.M. Marshall, G.D.W. Smith, W.E. Lee, Thermophysical properties of Co-free WC–FeCr hardmetals, in: Proc. 19th Plansee Seminar, Reutte, Austria, 2017.
- B. Roebuck, M. Gee, E. Bennett, Mechanical tests for hardmetals, National Physical Laboratory, Teddington, UK, 1999.
- H. Oettel, R. Wiedemann, S. Preißer, Residual stresses in nitride hard coatings prepared by magnetron sputtering and arc evaporation, Surf. Coat. Technol. 74–75 (1995) 273–278. [CrossRef]
- D. Qi, H. Lei, T. Wang, Z. Pei, J. Gong, C. Sun, Mechanical, microstructural and tribological properties of reactive magnetron sputtered Cr–Mo–N films, J. Mater. Sci. Technol. 31 (2015) 55–64. [CrossRef]
- Bertóti, Characterization of nitride coatings by XPS, Surf. Coat. Technol. 151–152 (2002) 194–203. [CrossRef]
- C. He, L. Xie, J. Zhang, G. Ma, Z. Du, J. Wang, D. Zhao, Microstructure and mechanical properties of reactive sputtered nanocrystalline Ti–Al–Ni–N thin films, Surf. Coat. Technol. 320 (2017) 472–477. [CrossRef]
- J. Hermann, Molybdenum and Nitrogen, Gmelin Handbook of Inorganic Chemistry, 8th ed., vol. B5, Springer, Berlin, 1989, pp. 1–66.
- H. Okamoto, N–Ti (Nitrogen–Titanium), J. Phase Equilib. Diffus. 34 (2013) 151–152. [CrossRef]
- T. Mills, Thermodynamic relations in the chromium–nitrogen system, J. Less-Common Met. 26 (1972) 223–234. [CrossRef]
- A.F. Guillermet, K. Frisk, Thermodynamic properties of Ni nitrides and phase stability in the Ni–N system, Int. J. Thermophys. 12 (1991) 417–431. [CrossRef]
- I.A. Abrikosov, A. Knutsson, B. Alling, F. Tasnádi, H. Lind, L. Hultman, M. Odén, Phase stability and elasticity of TiAlN, Materials 4 (2011) 1599–1618. [CrossRef]
- C. Paksunchai, S. Denchitcharoen, S. Chaiyakun, P. Limsuwan, Effect of sputtering current on structure and morphology of (Ti1–xCrx)N thin films deposited by reactive unbalanced magnetron co-sputtering, Procedia Eng. 32 (2012) 875–881. [CrossRef]
- M. Jaros, J. Musil, S. Haviar, Interrelationships among macrostress, microstructure and mechanical behavior of sputtered hard Ti(Al,V)N films, Mater. Lett. 235 (2019) 92–96. [CrossRef]
- J.A. Thornton, D.W. Hoffman, Stress-related effects in thin films, Thin Solid Films 171 (1989) 5–31. [CrossRef]
- J. Musil, M. Jaros, R. Cerstvy, S. Haviar, Evolution of macrostress in sputtered hard films, J. Vac. Sci. Technol. A 35 (2017) 020601. [CrossRef]
- C.T. Wang, T.J. Hakala, A. Laukkanen, H. Ronkainen, K. Holmberg, N. Gao, R.J.K. Wood, T.G. Langdon, An investigation into the effect of substrate on the load-bearing capacity of thin hard coatings, J. Mater. Sci. 51 (2016) 4390–4398. [CrossRef]
- M. Lepick, M. Gradzka-Dahlke, D. Pieniak, K. Pasierbiewicz, K. Krynsk, A. Niewczas, Tribological performance of titanium nitride coatings: a comparative study on TiN-coated stainless steel and titanium alloy, Wear 422–423 (2019) 68–80. [CrossRef]
- Q. Wang, F. Zhou, Z. Zhou, L.K.-Y. Li, J. Yan, An investigation on the crack resistance of CrN, CrBN and CrTiBN coatings via nanoindentation, Vacuum 145 (2017) 186–193. [CrossRef]
- A.A. Vereschaka, S.N. Grigoriev, Study of cracking mechanisms in multi-layered composite nano-structured coatings, Wear 378–379 (2017) 43–57. [CrossRef]
- P. Kumar, M.A. Jithin, S. Mohan, S. Avasthi, Hundred-fold reduction in iron diffusivity in titanium nitride diffusion barrier on steel by microstructure engineering, Thin Solid Films 716 (2020) 138416. [CrossRef]
- C. Sabitzer, C. Steinkellner, C.M. Koller, P. Polcik, R. Rachbauer, P.H. Mayrhofer, Diffusion behavior of C, Cr, and Fe in arc evaporated TiN- and CrN-based coatings and their influence on thermal stability and hardness, Surf. Coat. Technol. 275 (2015) 185–192. [CrossRef]
- Dahan, U. Admon, N. Frage, J. Sariel, M.P. Dariel, Diffusion in Ti/TiC multilayer coatings, Thin Solid Films 377–378 (2000) 687–693. [CrossRef]
- H. Nitta, T. Yamamoto, R. Kanno, K. Takasawa, T. Iida, Y. Yamazaki, S. Ogu, Y. Iijima, Diffusion of molybdenum in α-iron, Acta Mater. 50 (2002) 4117–4125. [CrossRef]
- K. Hirano, M. Cohen, B. Averbach, Diffusion of nickel into iron, Acta Metall. 9 (1961) 440–445. [CrossRef]
- Anders, Cathodic Arcs: From Fractal Spots to Energetic Condensation, Springer, New York, 2008. [CrossRef]
- Zhirkov, E. Oks, J. Rosen, Effect of N2 and Ar gas on DC arc plasma generation and film composition from Ti–Al compound cathodes, J. Appl. Phys. 117 (2015) 213301. [CrossRef]
- I.G. Brown, Vacuum arc ion sources, Rev. Sci. Instrum. 65 (1994) 3061–3081. [CrossRef]
- G.Yu. Yushkov, A. Anders, E.M. Oks, I.G. Brown, Ion velocities in vacuum arc plasmas, J. Appl. Phys. 88 (2000) 5618–5622. [CrossRef]
- H.S. Nalwa (Ed.), Handbook of Thin Film Materials, vol. 1: Deposition and Processing of Thin Films, Academic Press, San Diego, 2002.
- Leyland, A. Matthews, On the significance of the H/E ratio in wear control: a nanocomposite coating approach to optimized tribological behavior, Wear 246 (2000) 1–11. [CrossRef]
- B.R. Lawn, T.R. Wilshaw, Indentation fracture: principles and applications, J. Mater. Sci. 10 (1975) 1049–1081. [CrossRef]
- A.G. Evans, T.R. Wilshaw, Quasi-static solid particle damage in brittle solids – I. Observations, analysis and implications, Acta Mater. 24 (1976) 939–956. [CrossRef]
- M. Jaroš, J. Musil, R. Čerstvý, S. Haviar, Effect of energy on macrostress in Ti(Al,V)N films prepared by magnetron sputtering, Vacuum 158 (2018) 52–59. [CrossRef]
- B. Bhushan (Ed.), Modern Tribology Handbook, CRC Press, Boca Raton, FL, 2001.
- J.C.A. Batista, A. Matthews, C. Godoy, Micro-abrasive wear of PVD duplex and single-layered coatings, Surf. Coat. Technol. 142–144 (2001) 1137–1143. [CrossRef]
- Z.R. Liu, B. Peng, Y.X. Xu, Q. Zhang, Q. Wang, L. Chen, Influence of Ni-addition on mechanical, tribological properties and oxidation resistance of AlCrSiN coatings, Ceram. Int. 45 (2019) 3735–3742. [CrossRef]
- S. Adamiak, W. Bochnowski, A. Dziedzic, Ł. Szyller, D. Adamiak, Characteristics of the structure, mechanical, and tribological properties of a Mo–Mo2N nanocomposite coating deposited on the Ti6Al4V alloy by magnetron sputtering, Materials 14 (2021) 6819. [CrossRef]
- T. Wang, G. Zhang, S. Ren, B. Jiang, Effect of nitrogen flow rate on structure and properties of MoNx coatings deposited by facing target sputtering, J. Alloys Compd. 701 (2017) 1–8. [CrossRef]
- C. Wang, B. Xu, Z. Wang, H. Li, L. Wang, R. Chen, A. Wang, P. Ke, Tribological mechanism of (Cr,V)N coating in the temperature range of 500–900 °C, Tribol. Int. 159 (2021) 106952. [CrossRef]
- V.S. Sergevnin, I.V. Blinkov, A.O. Volkhonskii, D.S. Belov, D.V. Kuznetsov, M.V. Gorshenkov, E.A. Skryleva, Wear behaviour of wear-resistant adaptive nano-multilayered Ti–Al–Mo–N coatings, Appl. Surf. Sci. 388 (2016) 13–23. [CrossRef]
- V.S. Sergevnin, I.V. Blinkov, D.S. Belov, A.O. Volkhonskii, K.A. Kuptsov, N.I. Smirnov, Wear and erosion of arc-PVD multilayer Ti–Al–Mo–N coatings under various conditions of friction and loading, Int. J. Adv. Manuf. Technol. 98 (2018) 593–601. [CrossRef]
- K. Yang, G. Xian, H. Zhao, H. Fan, J. Wang, H. Wang, H. Du, Effect of Mo content on the structure and mechanical properties of TiAlMoN films deposited on WC–Co cemented carbide substrate by magnetron sputtering, Int. J. Refract. Met. Hard Mater. 52 (2015) 29–35. [CrossRef]
- S.A. Glatz, C.M. Koller, H. Bolvardi, S. Kolozsvári, H. Riedl, P.H. Mayrhofer, Influence of Mo on the structure and the tribomechanical properties of arc evaporated Ti–Al–N, Surf. Coat. Technol. 311 (2017) 330–336. [CrossRef]
- Q. Yang, Wear resistance and solid lubricity of molybdenum-containing nitride coatings deposited by cathodic arc evaporation, Surf. Coat. Technol. 332 (2017) 283–295. [CrossRef]
Figure 1.
Schematic diagram of the ion-plasma vacuum-arc evaporation setup showing the evaporator configuration. C1, C2 – cathodes with droplet separators; C3 – direct-flow evaporator.
Figure 1.
Schematic diagram of the ion-plasma vacuum-arc evaporation setup showing the evaporator configuration. C1, C2 – cathodes with droplet separators; C3 – direct-flow evaporator.
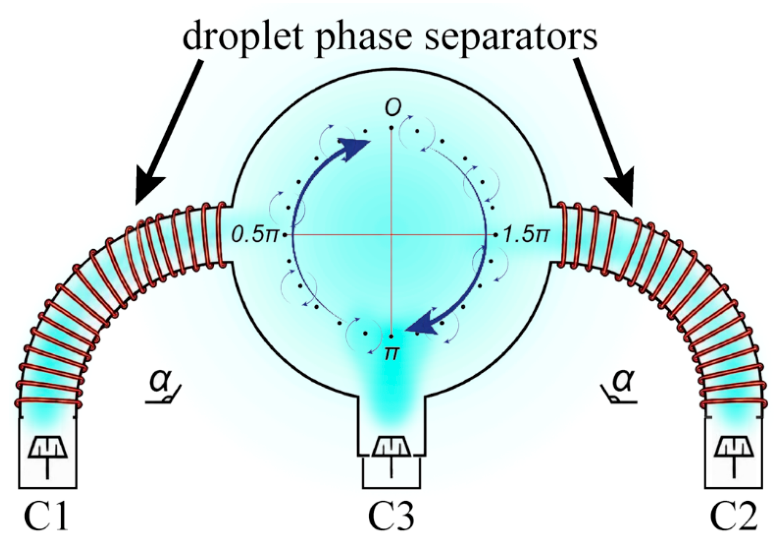
Figure 2.
Ti–Cr–Mo–Ni–N coating morphology on various tool materials: (a) HG20; (b) HS123; (c) HV420; (d) C80W1.
Figure 2.
Ti–Cr–Mo–Ni–N coating morphology on various tool materials: (a) HG20; (b) HS123; (c) HV420; (d) C80W1.
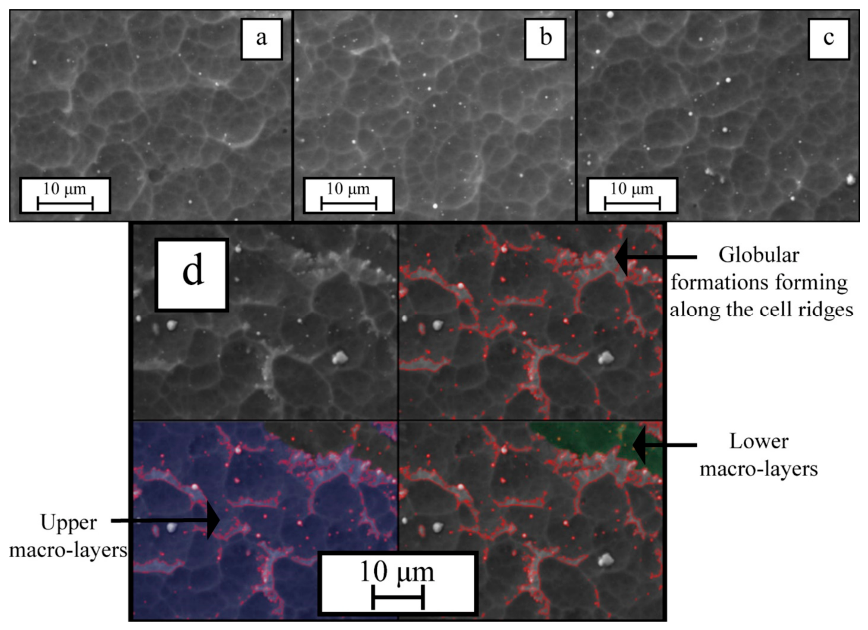
Figure 3.
Typical XRD patterns for Ti–Cr–Mo–Ni–N coatings deposited.
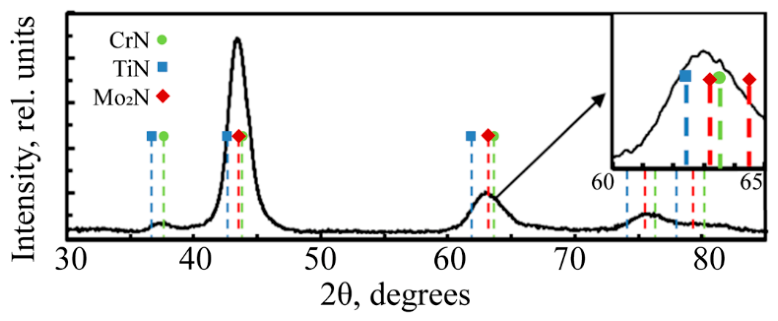
Figure 4.
Typical XPS spectra (N1s, Mo3p, and Mo3d) for Ti–Cr–Mo–N–Ni coatings.
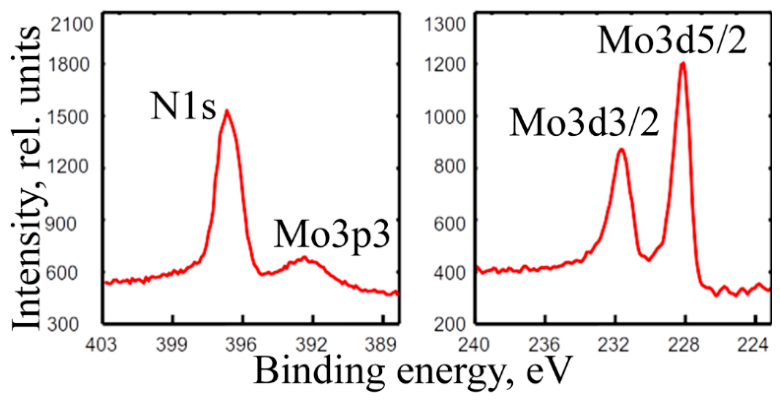
Figure 5.
Typical XPS spectra (Cr2p and Ti2p) for Ti–Cr–Mo–Ni–N coatings.
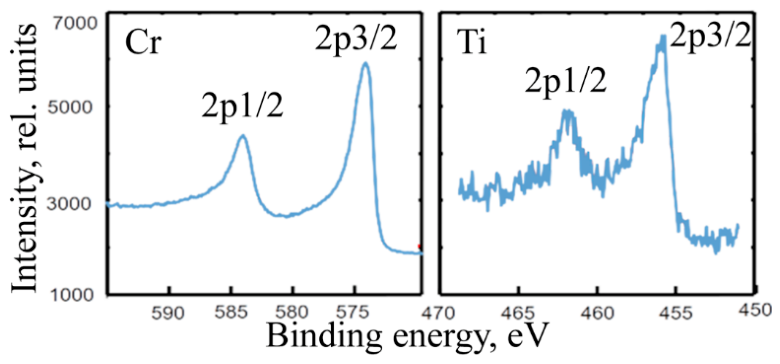
Figure 6.
Typical Ni2p3/2 XPS spectrum for Ti–Cr–Mo–N–Ni coatings.
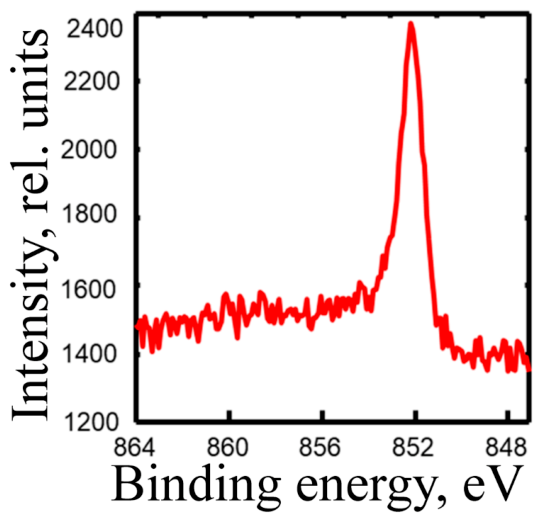
Figure 7.
TEM images for Ti–Cr–Mo–N–Ni coatings on HG20 (a,b); HS123 (c,d); HV420 (e,f); and C80W1 (g,h) substrates.
Figure 7.
TEM images for Ti–Cr–Mo–N–Ni coatings on HG20 (a,b); HS123 (c,d); HV420 (e,f); and C80W1 (g,h) substrates.
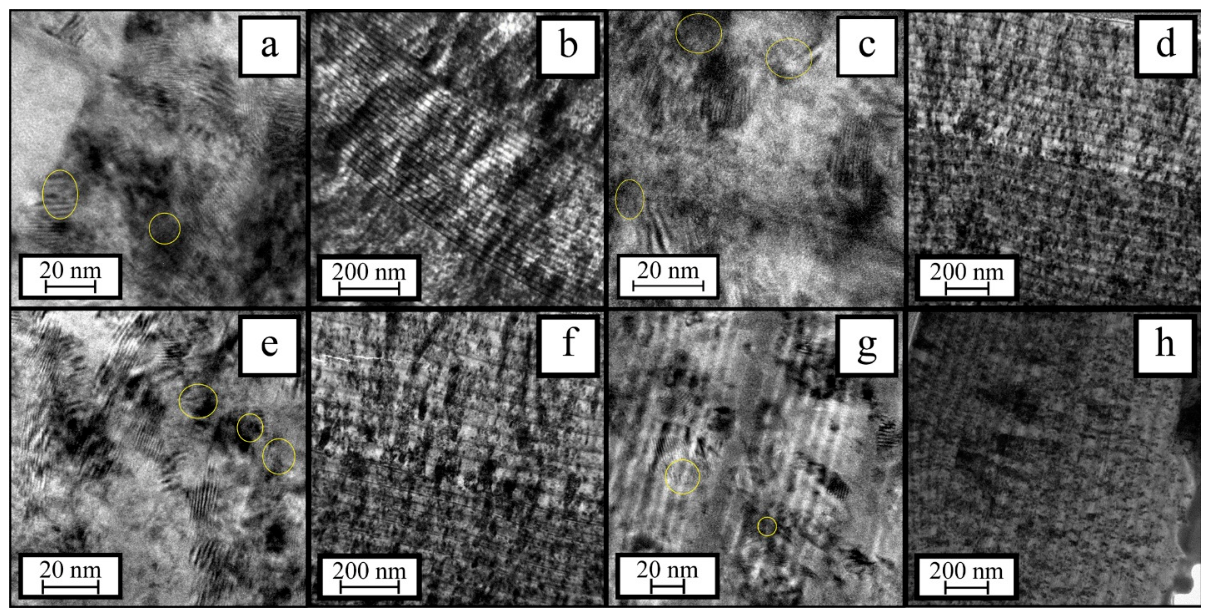
Figure 8.
TEM images for the Cr–Ti–Ni–Mo–N coating/substrate interface on (a) HG20, (b) HS123, (c) HV420, and (d) C80W1, with local elemental compositions at the marked analysis points (spectrum numbers).
Figure 8.
TEM images for the Cr–Ti–Ni–Mo–N coating/substrate interface on (a) HG20, (b) HS123, (c) HV420, and (d) C80W1, with local elemental compositions at the marked analysis points (spectrum numbers).
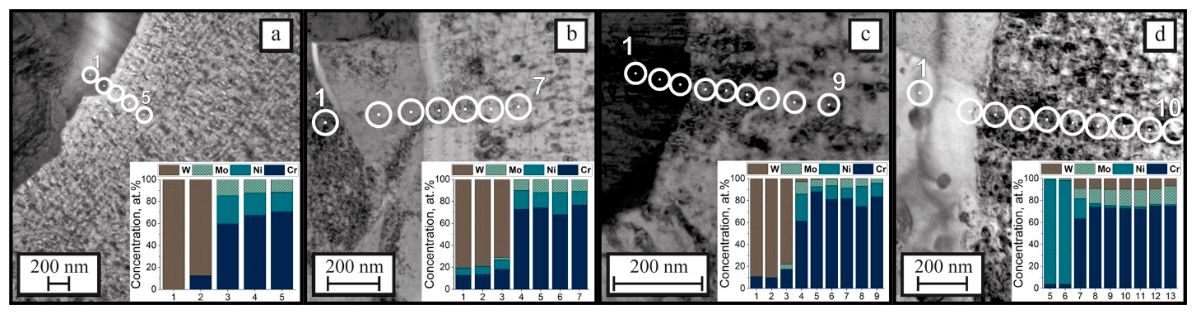
Figure 9.
Typical AE, μ, and Ff variation during scratch testing for Ti–Cr–Mo–Ni–N coatings (curves shown for HG20).
Figure 9.
Typical AE, μ, and Ff variation during scratch testing for Ti–Cr–Mo–Ni–N coatings (curves shown for HG20).
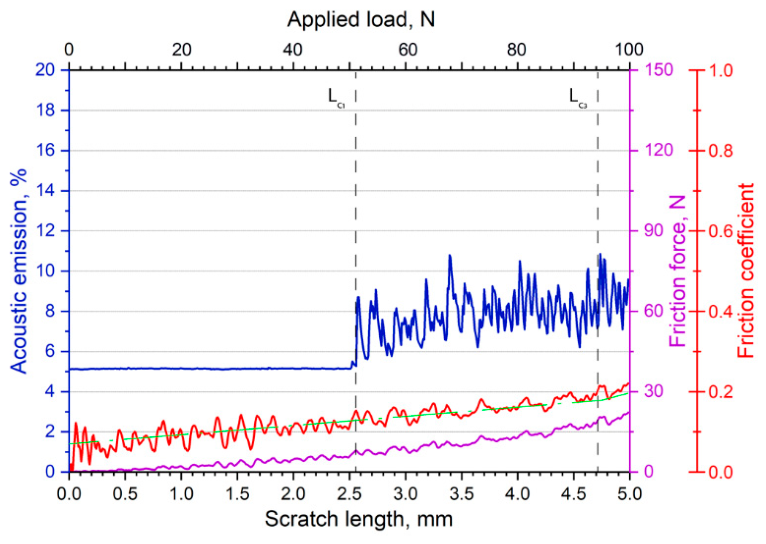
Figure 10.
Typical scratch image for Ti–Cr–Mo–Ni–N coatings during adhesion tests on various tool materials (shown for HG20).
Figure 10.
Typical scratch image for Ti–Cr–Mo–Ni–N coatings during adhesion tests on various tool materials (shown for HG20).
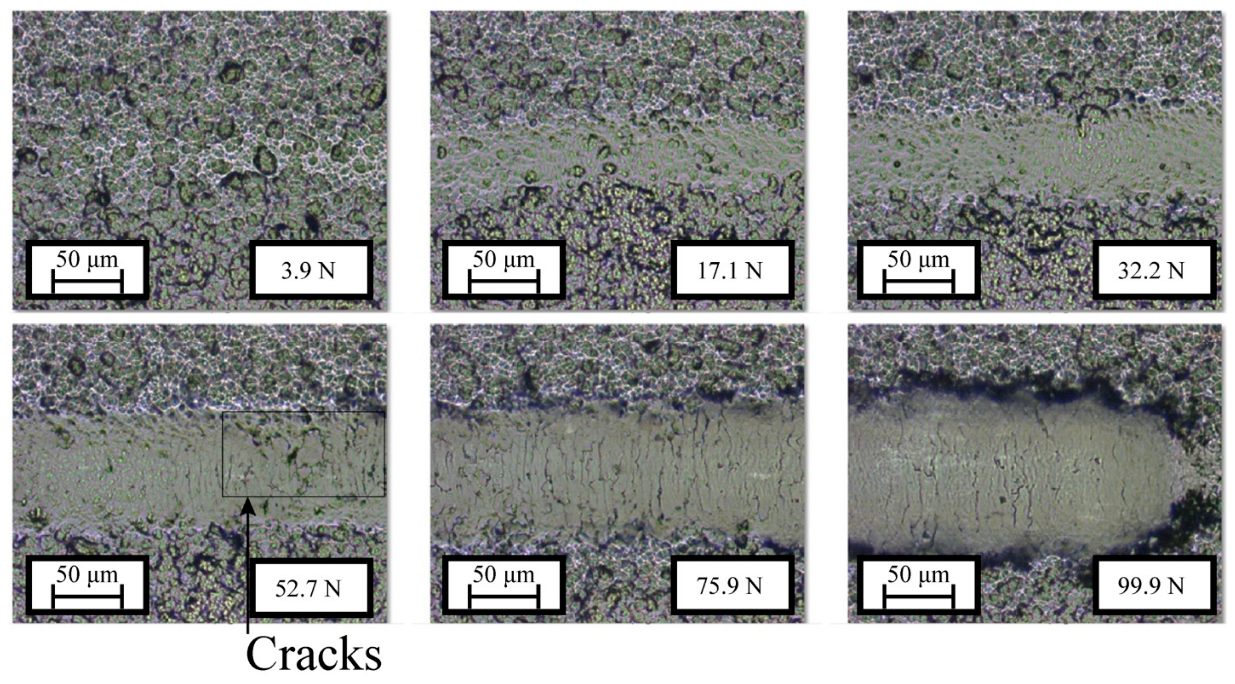
Figure 11.
Typical wear track profiles for Ti–Cr–Mo–Ni–N coated specimens on carbide alloys (shown for HV420) (a, c) and tool steel (b, d) substrates after tribological testing at 20 (a, b) and 500 °C (c, d).
Figure 11.
Typical wear track profiles for Ti–Cr–Mo–Ni–N coated specimens on carbide alloys (shown for HV420) (a, c) and tool steel (b, d) substrates after tribological testing at 20 (a, b) and 500 °C (c, d).
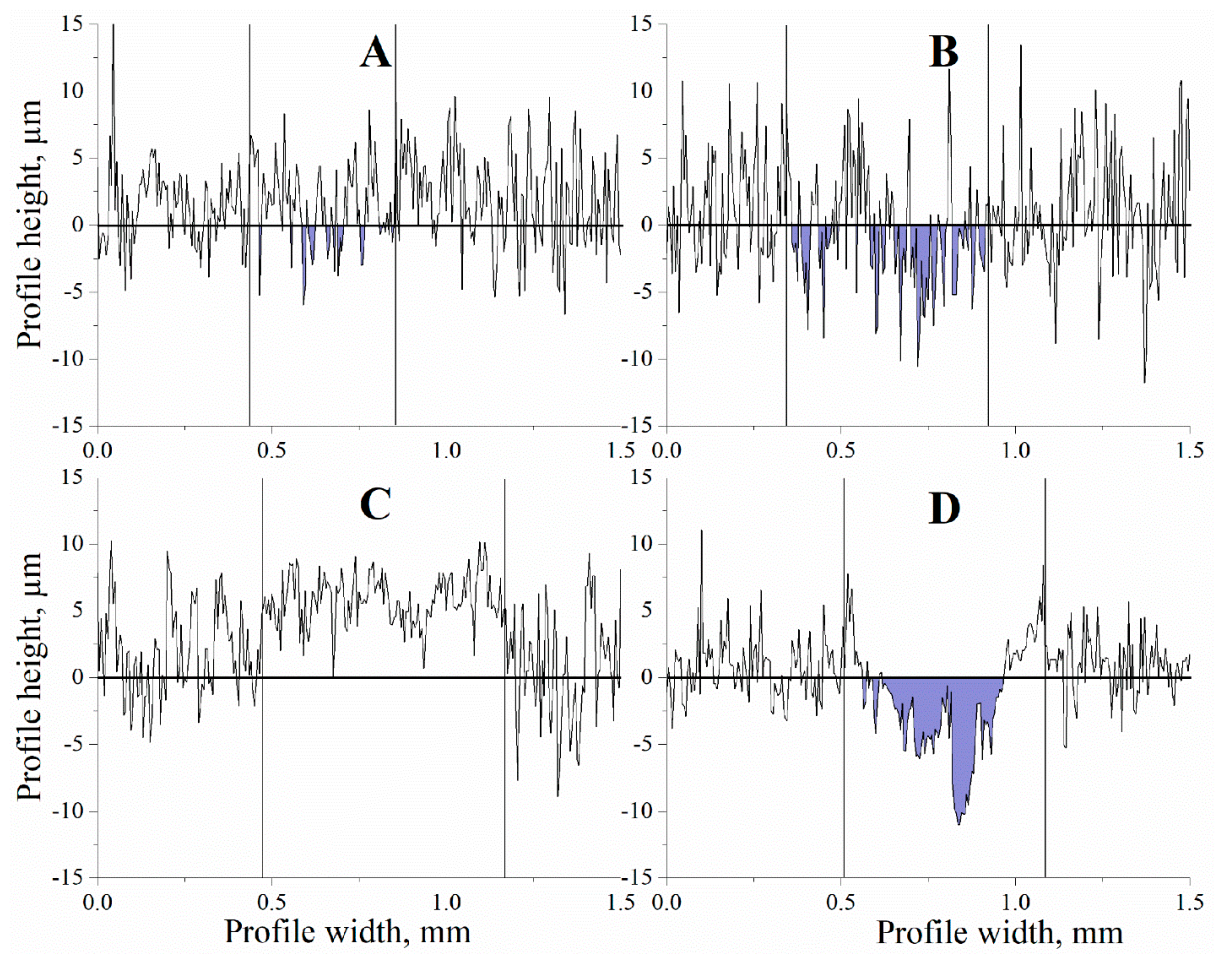
Figure 12.
Wear track morphology for the Ti–Cr–Mo–Ni–N coating on carbide alloy (a) and on tool steel (b).
Figure 12.
Wear track morphology for the Ti–Cr–Mo–Ni–N coating on carbide alloy (a) and on tool steel (b).
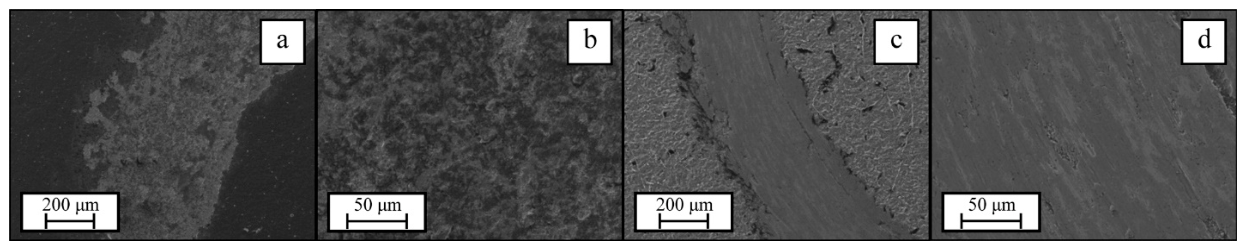

Table 1.
Ti–Cr–Mo–Ni–N coating chemical and phase composition.
| Substrate | Element content, at.% | Phase composition | ||||
| Ti | Cr | Mo | Ni | N | ||
| HG20 | 8.1 | 34.0 | 4.1 | 4.4 | 49.4 | TixCr1-xN; γ – Mo2N; Ni |
| HS123 | 7.6 | 36.2 | 3.4 | 4.3 | 48.5 | TixCr1-xN; γ – Mo2N; Ni |
| HV420 | 7.3 | 36.3 | 4.0 | 3.8 | 48.6 | TixCr1-xN; γ – Mo2N; Ni |
| C80W1 | 7.0 | 36.3 | 4.3 | 3.7 | 48.7 | TixCr1-xN; γ – Mo2N; Ni |
Table 2.
Substructure characteristics for the titanium-nitride-based phase in Ti–Cr–Mo–Ni–N coatings.
Table 2.
Substructure characteristics for the titanium-nitride-based phase in Ti–Cr–Mo–Ni–N coatings.
| Substrate | Lattice parameter (a), Å | Coherent scattering domain size, nm | Microstrain (ɛ), % |
| HG20 | 4.1558 | 37.1 | 0.26 |
| HS123 | 4.1759 | 38.3 | 0.50 |
| HV420 | 4.1666 | 61.5 | 0.55 |
| C80W1 | 4.1764 | 115.7 | 0.77 |
Table 3.
Macrostress values estimated by the Stoney method for Cr–Ti–Ni–Mo–N coatings on various tool substrates.
Table 3.
Macrostress values estimated by the Stoney method for Cr–Ti–Ni–Mo–N coatings on various tool substrates.
| Substrate | σcalc, GPa | R, m | R0, m | ts, 10–4·m | tf, 10–6·m | νs | Es, GPa |
| HG20 | -2.71 | 10.80 | 5.58 | 4.29 | 0.80 | 0.22 | 638 |
| HS123 | -2.56 | 0.90 | 0.76 | 3.06 | 0.88 | 0.22 | 550 |
| HV420 | -2.68 | 0.26 | 0.22 | 2.21 | 1.33 | 0.22 | 490 |
| C80W1 | +1.44 | -1.47 | -0.78 | 1.89 | 0.67 | 0.22 | 210 |
Table 4.
Diffusion zone width at the Ti–Cr–Mo–Ni–N coating/substrate interface versus substrate thermal diffusivity.
Table 4.
Diffusion zone width at the Ti–Cr–Mo–Ni–N coating/substrate interface versus substrate thermal diffusivity.
| Substrate | Diffusion zone width, nm | Thermal diffusivity, m2·s−1·106 |
| HG20 | 120 ± 6 | 32 |
| HS123 | 280 ± 40 | 23 |
| HV420 | 200 ± 40 | 19 |
| C80W1 | 340 ± 40 | 13 |
Table 5.
Ti–Cr–Mo–Ni–N coating physical–mechanical properties on tool substrates.
| Substrate | Microhardness (H), GPa |
Elastic modulus, (E), GPa |
Elastic deformation resistance, (H/E) | Plastic deformation resistance, (H3/E2), GPa | Relative plastic deformation work (Wₚ), % |
| HG20 | 25.1 +/- 2.2 | 481 +/- 36 | 0.052 | 0.068 | 57 |
| HS123 | 21.7 +/- 1.1 | 427 +/- 9 | 0z.051 | 0.056 | 56 |
| HV420 | 22.4 +/- 1.2 | 401 +/- 42 | 0.056 | 0.070 | 56 |
| C80W1 | 20.3 +/- 1.1 | 292 +/- 16 | 0.070 | 0.098 | 49 |
Table 6.
lists critical loads Lc1 and Lc3 derived from scratch test data, showing high adhesion strength for coatings on carbide alloy substrates and relatively low values on C80W1 steel (Lc2 was not determined, given the cohesive failure mode and no delamination). This is explained by the greater fracture toughness for these coatings (relative plastic deformation work 56–57% vs. 49%, Table 5) and by larger compressive macrostresses, which retard crack initiation and growth (Table 3) [74]. These results, together with the above considerations, may also indicate low abrasive wear resistance for coatings on C80W1 steel. This can be attributed to the relatively lower hardness for coatings on these substrates compared with those on carbide alloys (Table 5), since hardness is the key factor determining material resistance to such wear [75, 76].Table 6. Tribological and adhesion properties for Ti–Cr–Mo–Ni–N coatings.
| Substrate | Lc1, N | Lc3, N | μ20/μ500* | K20/K500** |
| HG20 | 52 | > 100 N | 0.53/0.56 | ****/*** |
| HS123 | 100 | > 100 N | 0.52/0.54 | ****/*** |
| HV420 | 39 | > 100 N | 0.49/0.59 | ****/*** |
| C80W1 | 11 | 30 | 0.49/0.47 | 49.80/74.20 |
* μ20 and μ500 – friction coefficients determined in a pin-on-disk configuration at 5 N load, Al2O3 counterbody ball (6 mm diameter), sliding speed 10 cm/s, total sliding distance 3200 revolutions, at test temperatures 20 °C and 500 °C. ** K20 and K500 (10−6 mm3·N−1·m−1) – wear rates for coating specimens during tribological testing at 20 °C and 500 °C. *** – wear rate determination was hindered by counterbody wear debris adhesion to the specimen surface in the contact zone. **** – wear rate determination was hindered because the wear track depth was comparable to the surface roughness.
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (http://creativecommons.org/licenses/by/4.0/).
Copyright: This open access article is published under a Creative Commons CC BY 4.0 license, which permit the free download, distribution, and reuse, provided that the author and preprint are cited in any reuse.