

Submitted:
24 December 2024
Posted:
25 December 2024
You are already at the latest version
Abstract
Rapid prototyping has advanced into additive manufacturing (AM), enabling direct production of functional components through a hybrid approach combining additive and subtractive processes. In metal-wire AM, arc and laser energy sources are common, with geometry complexity influencing kinematic choices (3/4/5 axis) and necessitating tailored slicing techniques. Whereas this paper explores various levels of hybridization, essential for creating functional components using the metal-wire AM process. These levels encompass process hybridization (addition/subtraction), energy source hybridization (arc/laser), kinematics hybridization (3/4/5 axis), and slicing technique hybridization (planar/conformal). A unified system was designed to accommodate all levels of hybridization on a single machine with a single setup that minimizes the time and improves accuracy. The study presents a detailed exploration of these hybridization levels through the fabrication of a complex 5-axis geometry—an impeller. The impeller was manufactured with hybridization using various levels and subsequently compared with manufacturing processes like additive manufacturing with interlayer machining and traditional machining methods. The hybrid approach significantly reduced the manufacturing time for the selected impeller geometry from 3536 minutes to 792 minutes (saving 77.6% manufacturing time) and minimized material waste to 9.3%, compared to 74.07% in traditional machining. This demonstrates a more efficient, precise, and cost-effective method for producing complex metal components. Furthermore, it offers critical insights into the effectiveness of this hybrid method by optimizing metal-wire AM processes for intricate geometries, thereby advancing the capabilities and applications of metal-wire AM technology.
Keywords:
1. Introduction
2. Materials and Methods
2.1. Materials
2.2. Approach for Deposition
2.3. Fixture
2.4. Test Methods
2.5. Slicing and Deposition Methodology
3. Results and Discussion
3.1. Process Hybridization
3.2. Energy Hybridization
3.3. Kinematic and Slicing Hybridization
3.4. Time and material wastage comparison
4. Conclusions
References
- Karunakaran, K.P.; Kamal Gupta, N.; Kumar Patel, A.; Rakeshkumar, K.; Ganesan, G.; Siddhartha; Sealy, M.; Bernard, A. Multi-Station Multi-Axis Hybrid Layered Manufacturing (MSMA-HLM). Manuf Lett 2022, 33, 630–639. [CrossRef]
- Gupta, N.K.; Ganesan, G.; Siddhartha, S.; Karade, S.R.; Singh, S.D.; Karunakaran, K.P. A Dual-Side Deposition Technique to Mitigate Deformation in Wire Arc Additive Manufacturing. Transactions of the Indian Institute of Metals 2024, 77, 3425–3434. [CrossRef]
- Sealy, M.P.; Madireddy, G.; Williams, R.E.; Rao, P.; Toursangsaraki, M. Hybrid Processes in Additive Manufacturing. Journal of Manufacturing Science and Engineering, Transactions of the ASME 2018, 140. [CrossRef]
- Flynn, J.M.; Shokrani, A.; Newman, S.T.; Dhokia, V. Hybrid Additive and Subtractive Machine Tools - Research and Industrial Developments. International Journal of Machine Tools and Manufacture 2016, 101, 79–101. [CrossRef]
- Strong, D.; Sirichakwal, I.; Manogharan, G.P.; Wakefield, T. Current State and Potential of Additive - Hybrid Manufacturing for Metal Parts. Rapid Prototyping Journal 2017, 23, 577–588. [CrossRef]
- Suryakumar, S.; Karunakaran, K.P.; Bernard, A.; Chandrasekhar, U.; Raghavender, N.; Sharma, D. Weld Bead Modeling and Process Optimization in Hybrid Layered Manufacturing. CAD Computer Aided Design 2011, 43, 331–344. [CrossRef]
- Park, S.H.; Son, S.J.; Lee, S.B.; Yu, J.H.; Ahn, S.J.; Choi, Y.S. Surface Machining Effect on Material Behavior of Additive Manufactured SUS 316L. Journal of Materials Research and Technology 2021, 13, 38–47. [CrossRef]
- Kaynak, Y.; Kitay, O. Porosity, Surface Quality, Microhardness and Microstructure of Selective Laser Melted 316l Stainless Steel Resulting from Finish Machining. Journal of Manufacturing and Materials Processing 2018, 2. [CrossRef]
- Yang, Y.; Gong, Y.; Qu, S.; Yin, G.; Liang, C.; Li, P. Additive and Subtractive Hybrid Manufacturing (ASHM) of 316L Stainless Steel: Single-Track Specimens, Microstructure, and Mechanical Properties. Jom 2021, 73, 759–769. [CrossRef]
- Xinhong, X.; Haiou, Z.; Guilan, W.; Guoxian, W. Hybrid Plasma Deposition and Milling for an Aeroengine Double Helix Integral Impeller Made of Superalloy. Robotics and Computer-Integrated Manufacturing 2010, 26, 291–295. [CrossRef]
- Chen, C.; Feng, T.; Zhang, Y.; Ren, B.; Hao wang; Zhao, X. Improvement of Microstructure and Mechanical Properties of TC4 Titanium Alloy GTAW Based Wire Arc Additive Manufacturing by Using Interpass Milling. Journal of Materials Research and Technology 2023, 27, 1428–1445. [CrossRef]
- Karunakaran, R.; Sotelo, L.D.; Maharaja, H.; Nez, C.; Ramoni, M.; Halliday, S.; Mishra, S.; Karunakaran, K.P.; Turner, J.A.; Sealy, M.P. Increased Ductility of Ti-6Al-4V by Interlayer Milling during Directed Energy Deposition. Additive Manufacturing 2023, 78, 103818. [CrossRef]
- Sadeh, S.; Mathews, R.; Zhang, R.; Sunny, S.; Marais, D.; Venter, A.M.; Li, W.; Malik, A. Interlayer Machining Effects on Microstructure and Residual Stress in Directed Energy Deposition of Stainless Steel 316L. Journal of Manufacturing Processes 2023, 94, 69–78. [CrossRef]
- Ivántabernero; Paskual, A.; Álvarez, P.; Suárez, A. Study on Arc Welding Processes for High Deposition Rate Additive Manufacturing. In Proceedings of the Procedia CIRP; Elsevier B.V., 2018; Vol. 68, pp. 358–362.
- Gupta, N.K.; Ganesan, G.; Siddhartha, S.; Karade, S.R.; Paul, A.K.; Dubey, S.; Ely, R.H.; Karunakaran, K.P. In Situ Pre-Heating in Wire Arc Additive Manufacturing: Design, Development, and Experimental Investigation on Residual Stresses and Metallurgical and Mechanical Properties. J Mater Eng Perform 2024. [CrossRef]
- Chuang, L.C.; Young, H.T. Integrated Rough Machining Methodology for Centrifugal Impeller Manufacturing. International Journal of Advanced Manufacturing Technology 2007, 34, 1062–1071. [CrossRef]
- Fan, H.Z.; Wang, W.; Xi, G. A Novel Five-Axis Rough Machining Method for Efficient Manufacturing of Centrifugal Impeller with Free-Form Blades. International Journal of Advanced Manufacturing Technology 2013, 68, 1219–1229. [CrossRef]
- Zhu, Q.; Midson, S.P.; Chng, W.M.; Atkinson, H. V. Casting and Heat Treatment of Turbocharger Impellers Thixocast from Alloy 201. Solid State Phenomena 2013, 192–193, 556–561. [CrossRef]
- Adiaconitei, A.; Vintila, I.S.; Mihalache, R.; Paraschiv, A.; Frigioescu, T.; Vladut, M.; Pambaguian, L. A Study on Using the Additive Manufacturing Process for the Development of a Closed Pump Impeller for Mechanically Pumped Fluid Loop Systems. Materials 2021, 14, 1–17. [CrossRef]
- Gupta, Neel Kamal, G, Ganesan, Siddhartha, Karade Shahu, Mehta, Avinash Kumar, KP, Karunakaran Effect of Multiple Technologies on Minimizing the Residual Stresses in Additive Manufacturing. In Proceedings of the ICRS 11 - The 11th International Conference of Residual Stresses, SF2M; IJL, Mar 2022, Nancy, France.; 2022; Vol. hal-040150.
- Jacob, K.; Yadav, D.; Dixit, S.; Hohenwarter, A.; Jaya, B.N. High Pressure Torsion Processing of Maraging Steel 250: Microstructure and Mechanical Behaviour Evolution. Materials Science and Engineering: A 2021, 802, 140665. [CrossRef]
- Farias, F.W.C.; da Cruz Payão Filho, J.; Moraes e Oliveira, V.H.P. Prediction of the Interpass Temperature of a Wire Arc Additive Manufactured Wall: FEM Simulations and Artificial Neural Network. Additive Manufacturing 2021, 48. [CrossRef]
- Paul, S.; Liu, J.; Strayer, S.T.; Zhao, Y.; Sridar, S.; Klecka, M.A.; Xiong, W.; To, A.C. A Discrete Dendrite Dynamics Model for Epitaxial Columnar Grain Growth in Metal Additive Manufacturing with Application to Inconel. Additive Manufacturing 2020, 36, 101611. [CrossRef]
- Wang, J.; Lin, X.; Wang, J.; Yang, H.; Zhou, Y.; Wang, C.; Li, Q.; Huang, W. Grain Morphology Evolution and Texture Characterization of Wire and Arc Additive Manufactured Ti-6Al-4V. Journal of Alloys and Compounds 2018, 768, 97–113. [CrossRef]
- Rodrigues, T.A.; Duarte, V.; Miranda, R.M.; Santos, T.G.; Oliveira, J.P. Current Status and Perspectives on Wire and Arc Additive Manufacturing (WAAM). Materials 2019, 12. [CrossRef]
- Londhe, M.P.; Chilwant, /; Mumbai, K.N. Optimization of Cutting Parameters in Milling Operation To Improve Surface Finish of EN 31. International Journal of Engineering Sciences & Management Research 2016, 3, 1–9. [CrossRef]
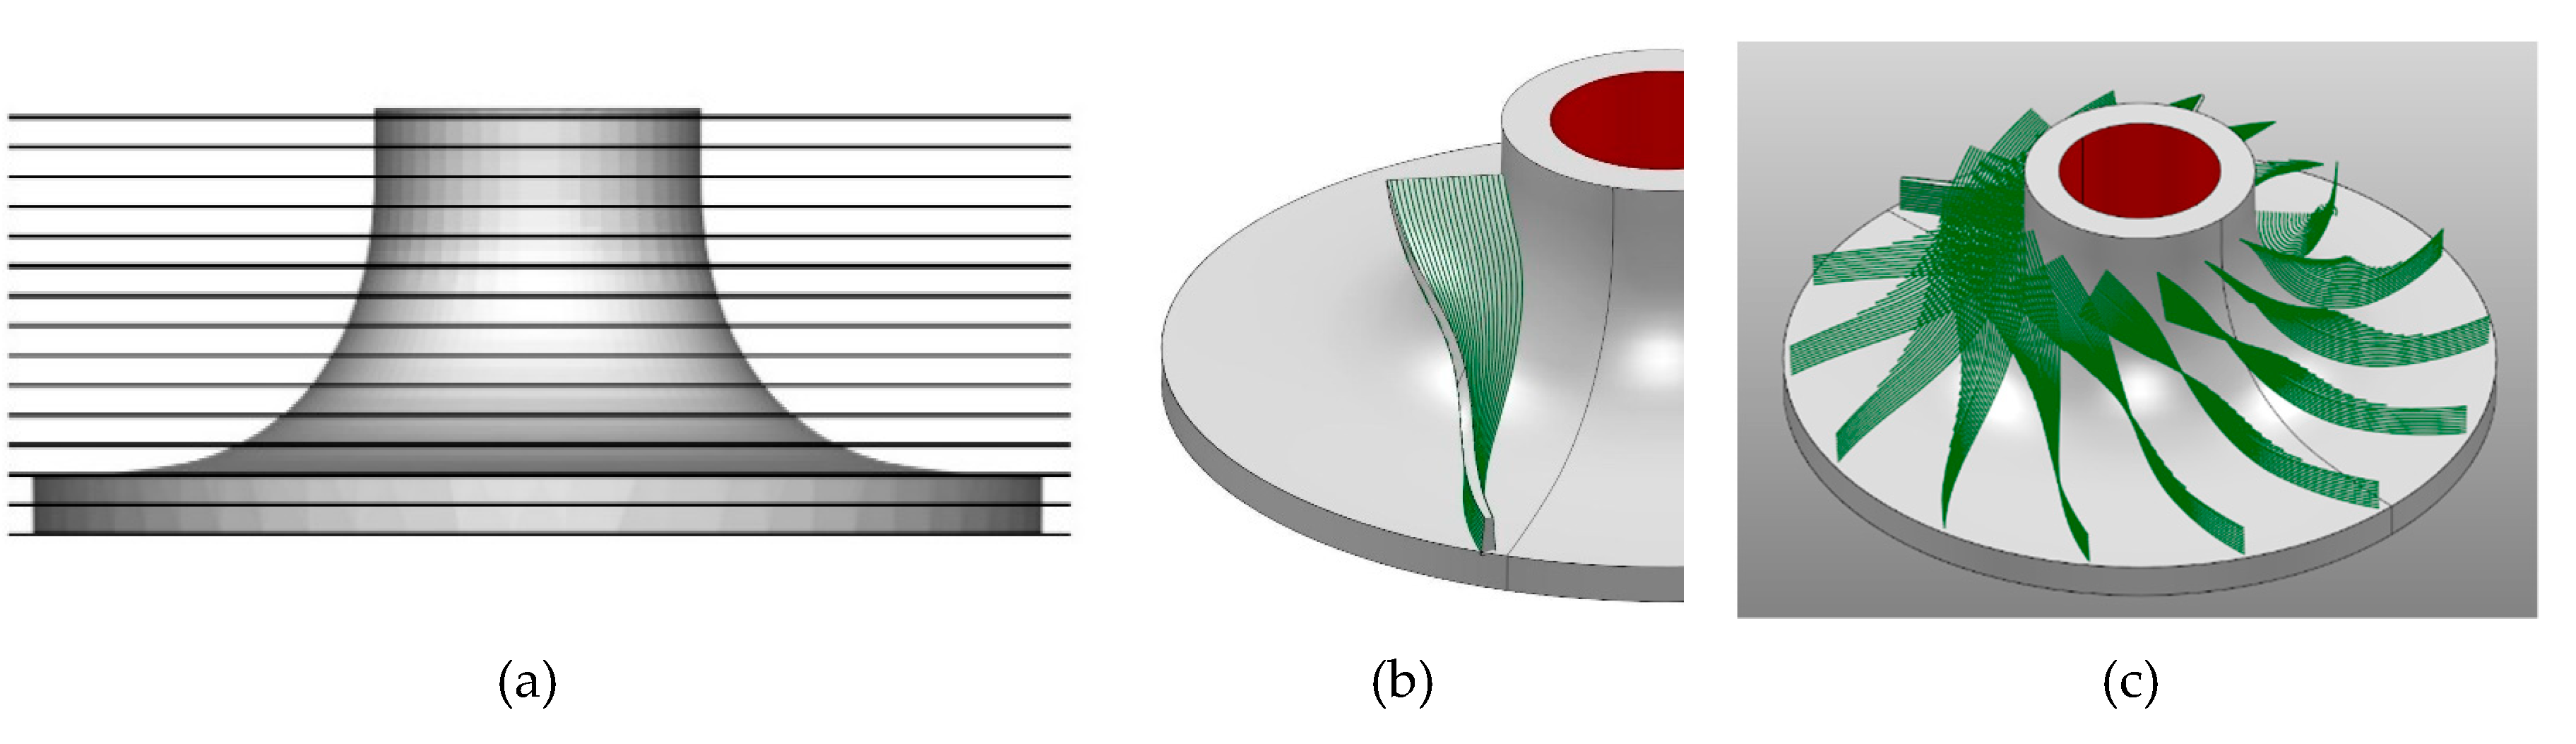
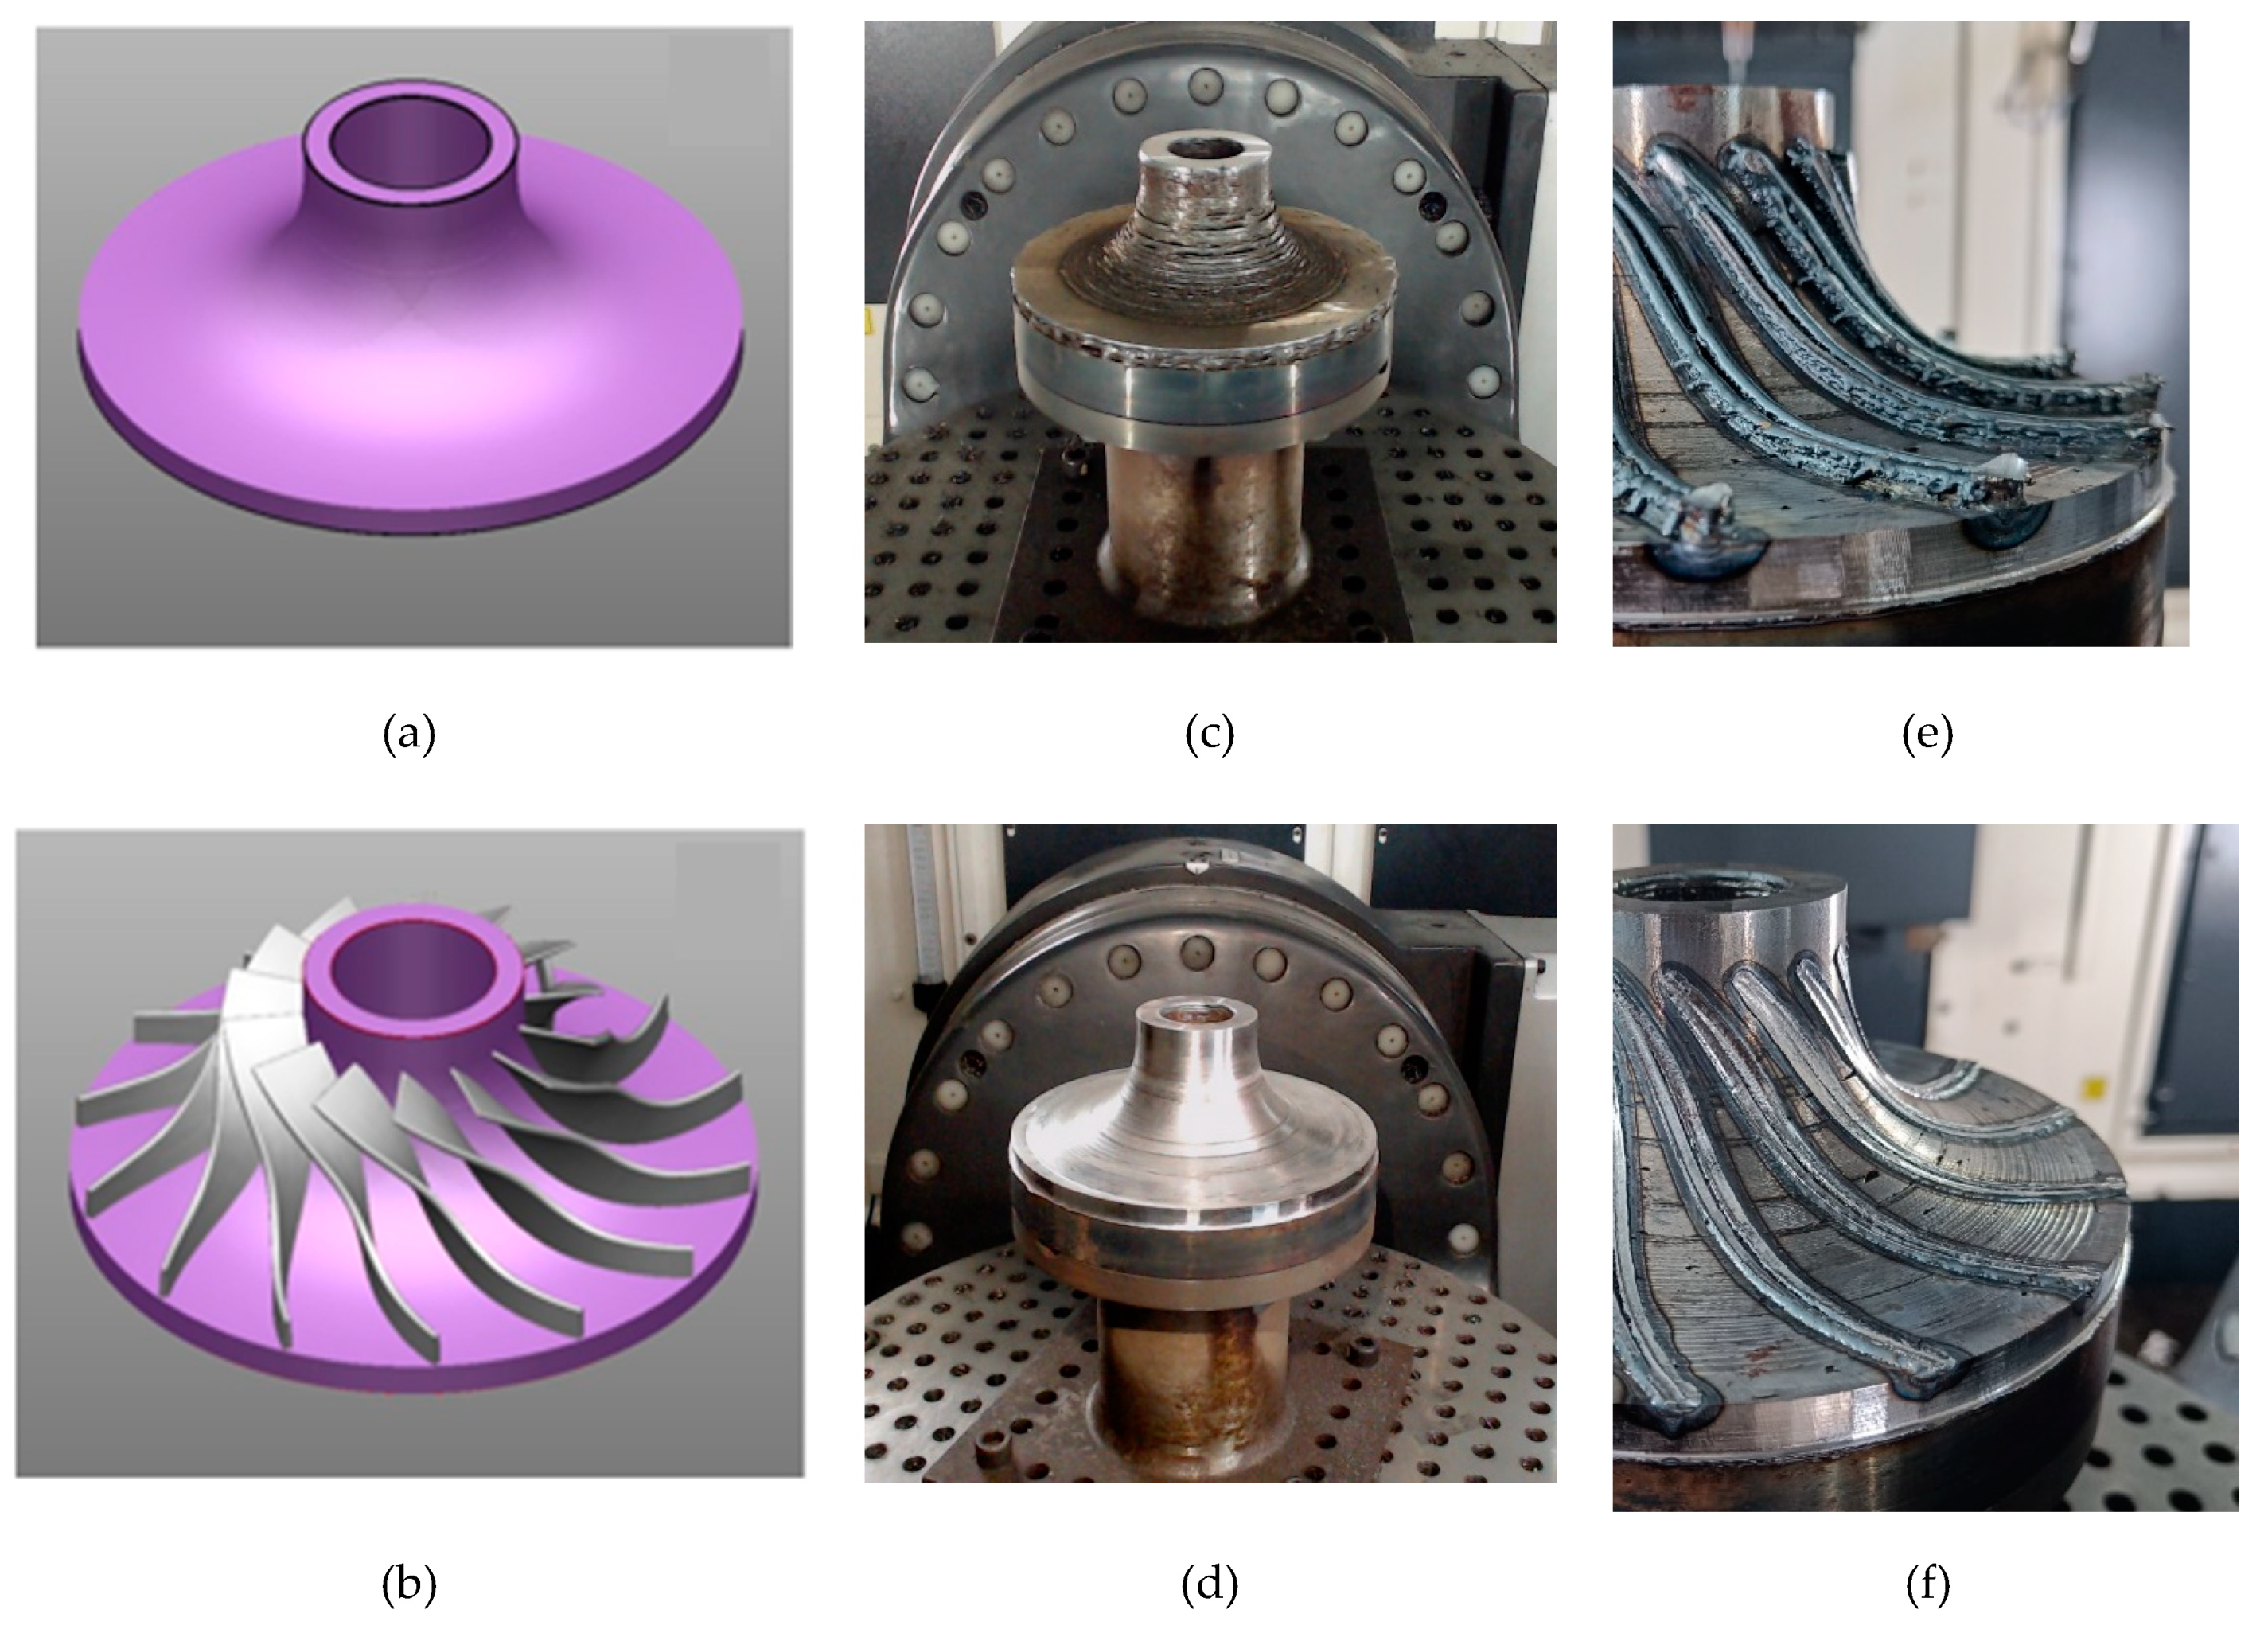
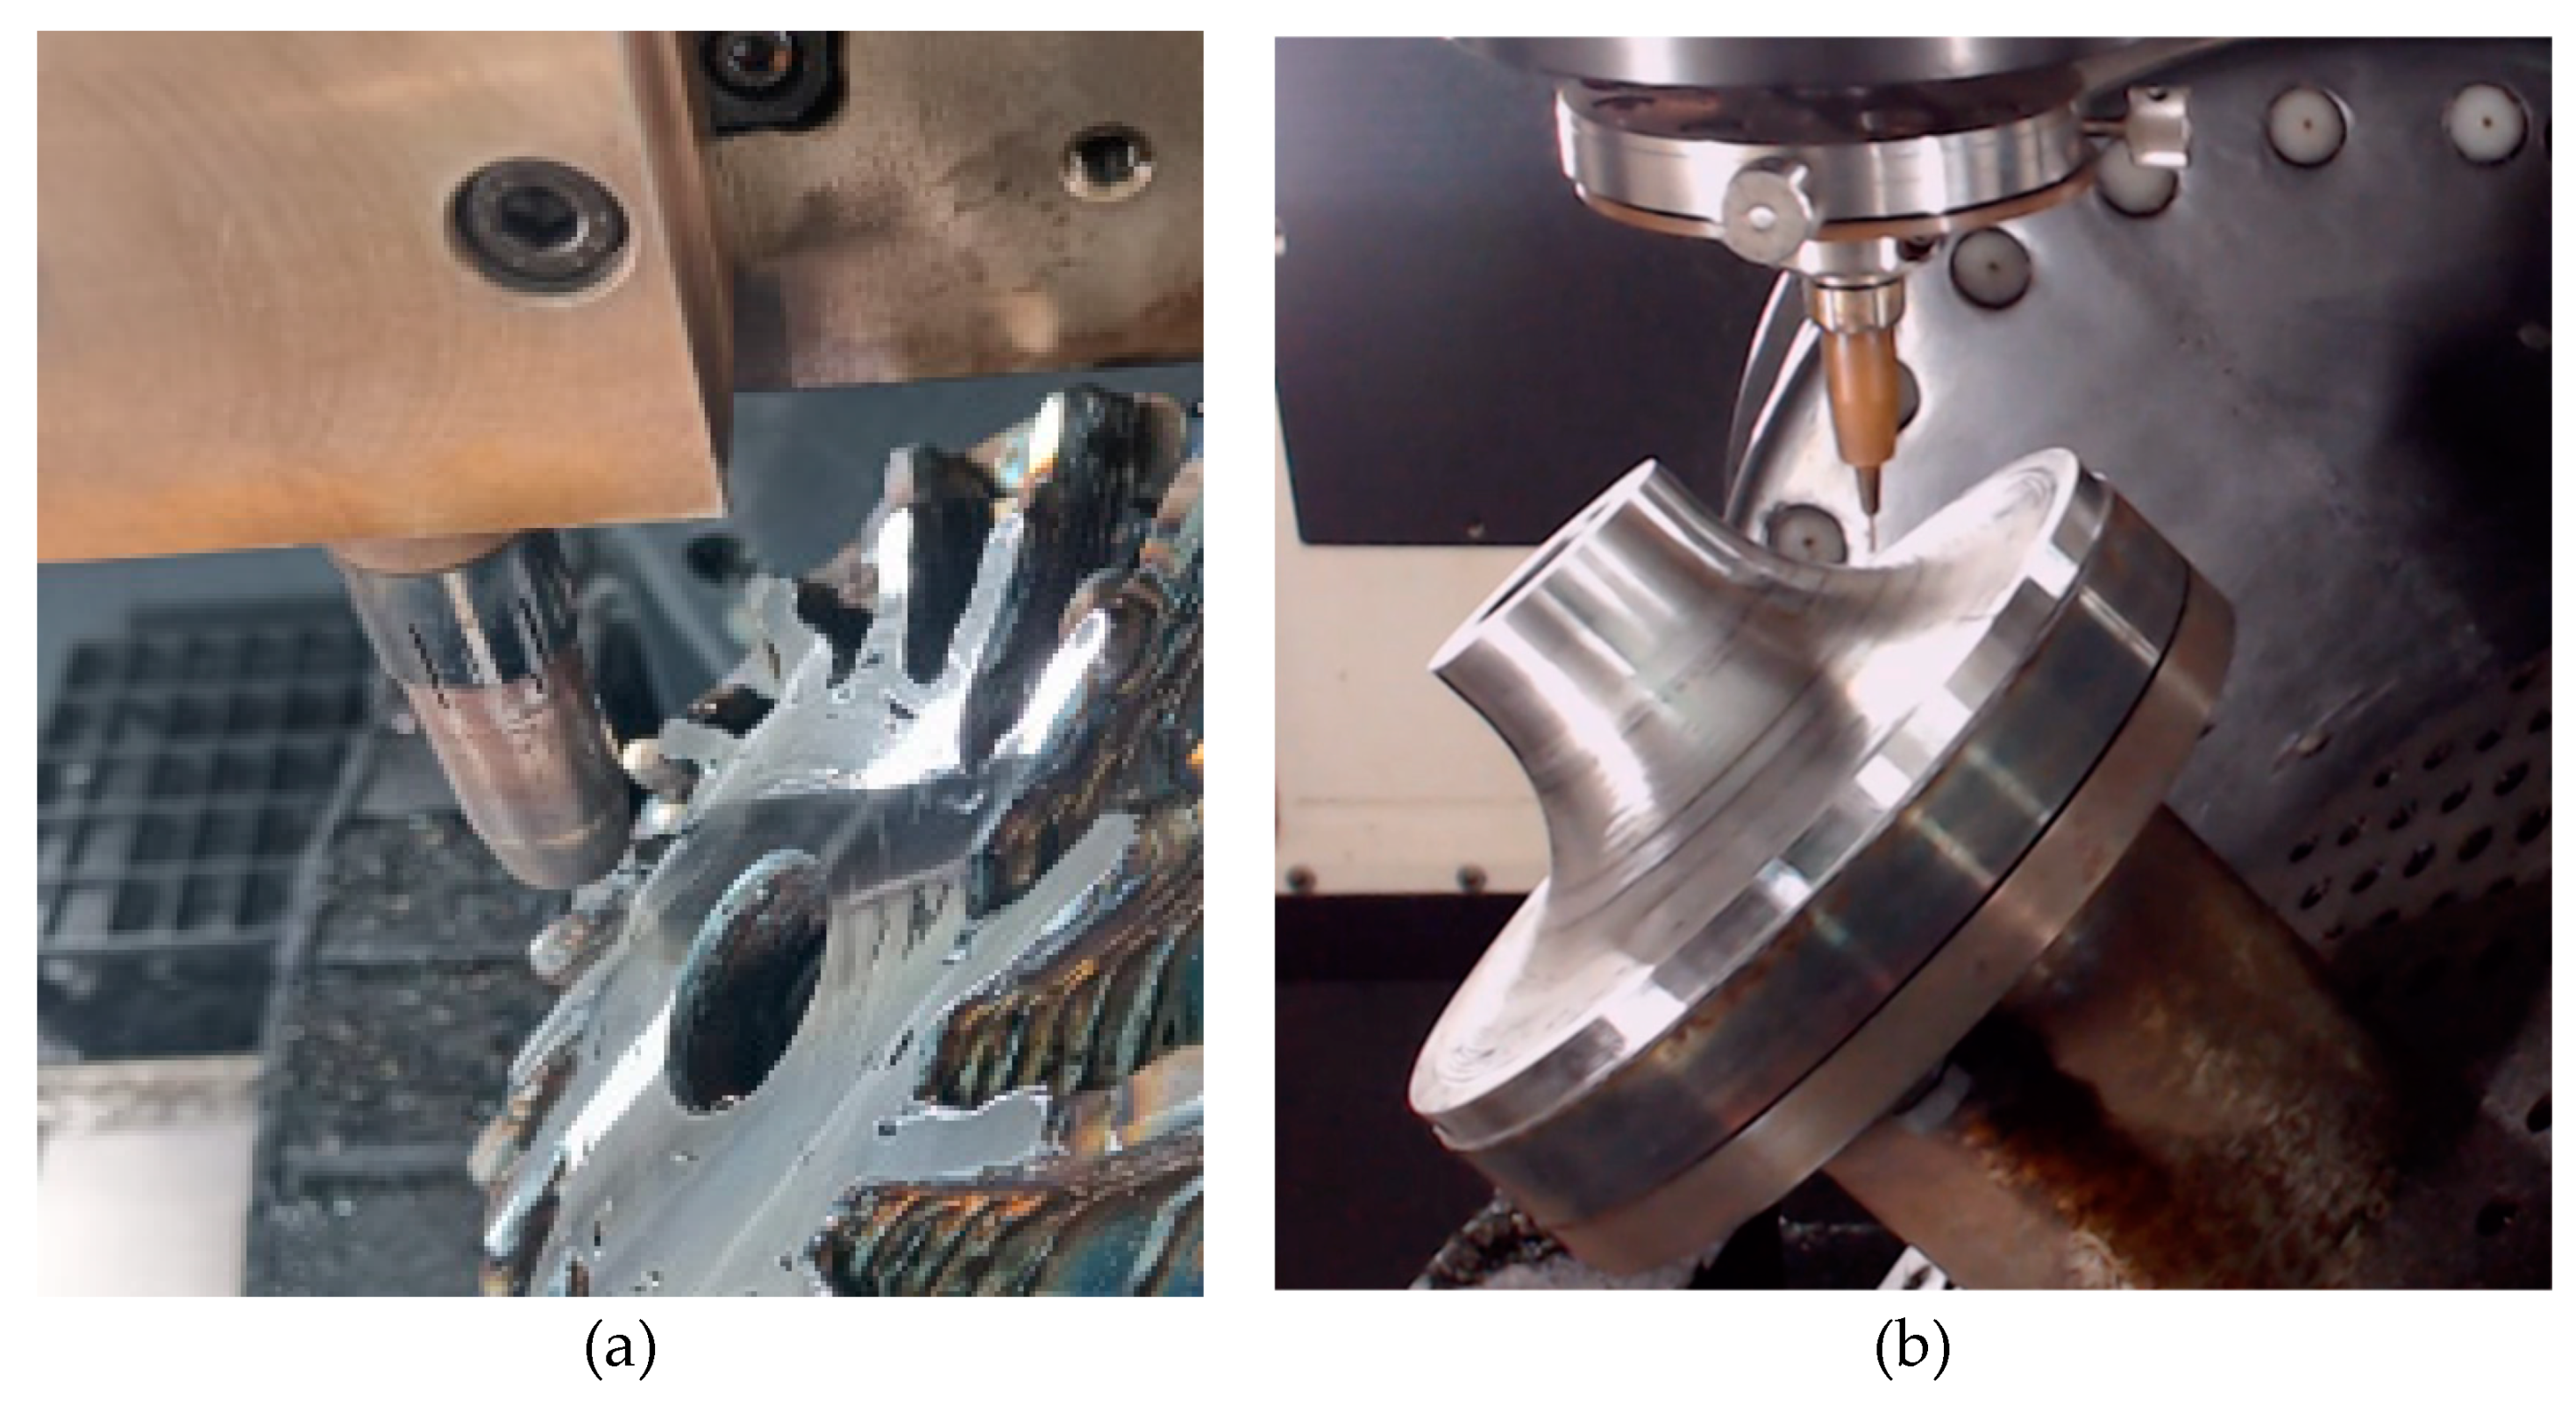
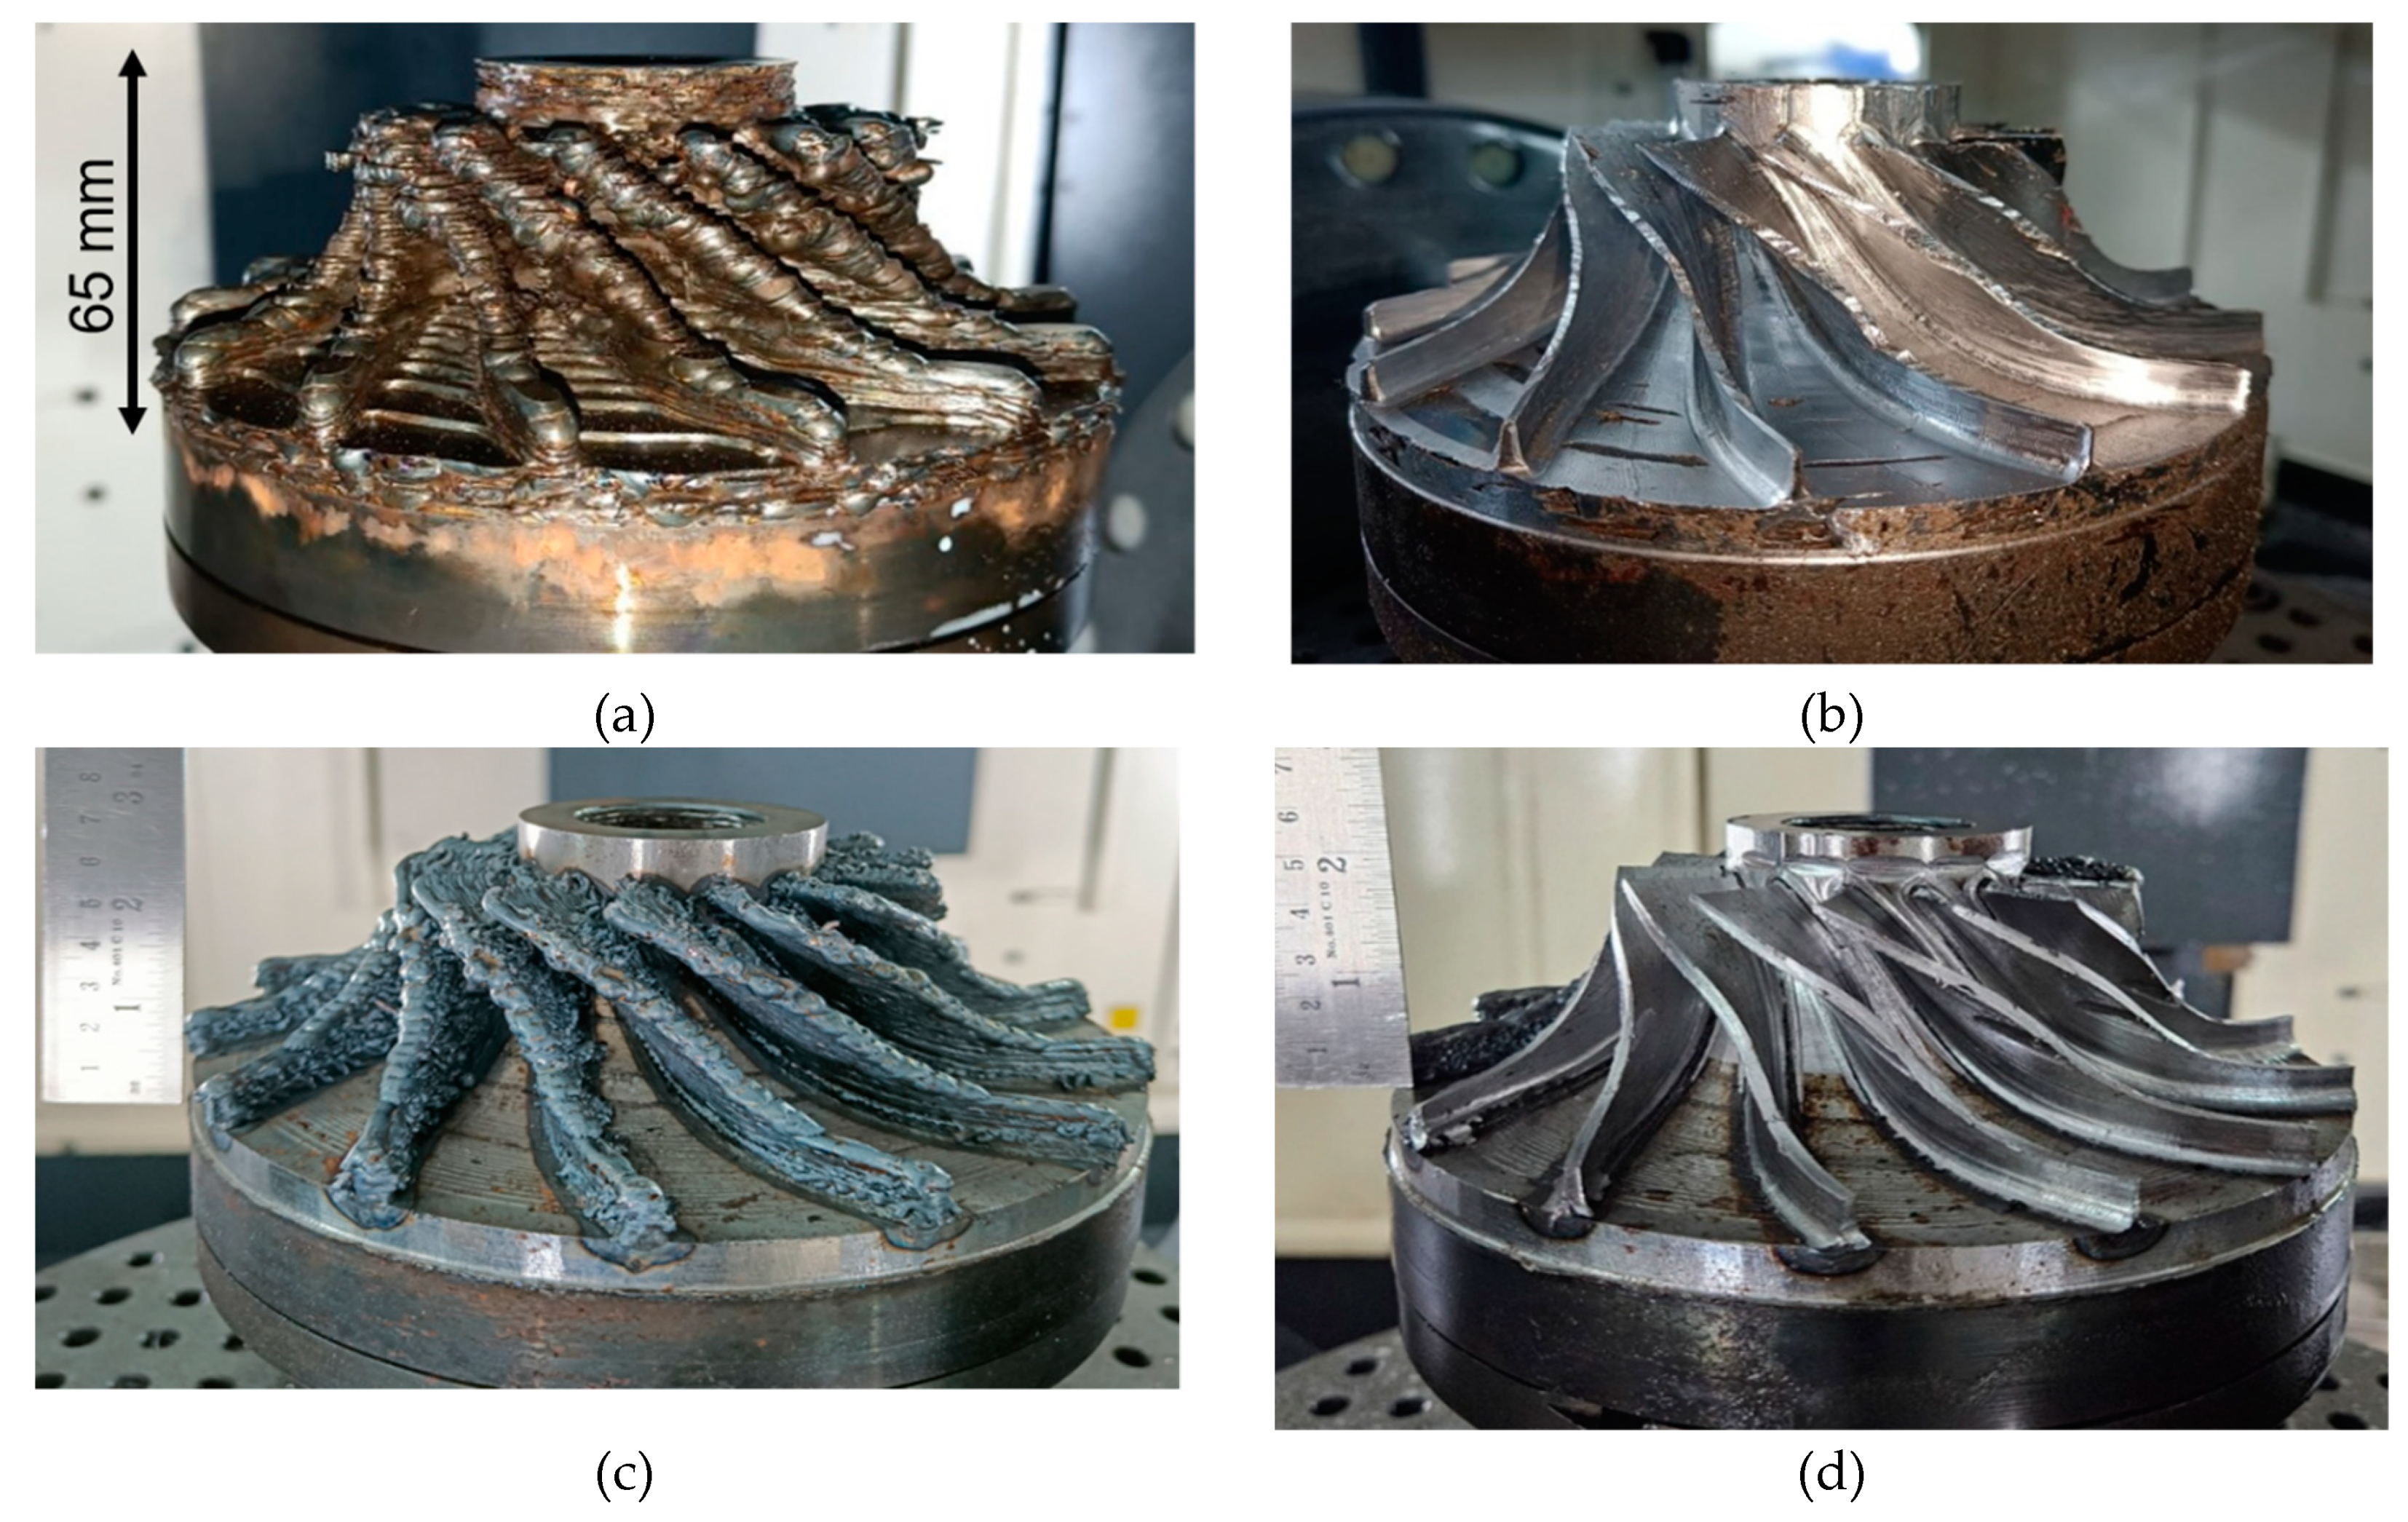

| Material | C | Si | Mn | Cr | Ni | Cu | P | Mo | S | Ti | Fe |
|---|---|---|---|---|---|---|---|---|---|---|---|
| ER70S-6 | 0.06 | 0.94 | 1.64 | 0.02 | 0.02 | 0.02 | 0.013 | 0.005 | 0.016 | 0.004 | Remaining |
| Case study |
Part | Energy Source | Current (A) | Voltage (V) | Power (W) | Wire Feed rate (m/min) | Travel Feed (mm/min) | Stepover (mm) |
|---|---|---|---|---|---|---|---|---|
| Planar 5-axis |
Impeller | MIG | 110 | 11.4 | 1254 | - | 1000 | 2 |
| Conformal | Hub | MIG | 110 | 11.4 | 1254 | - | 1000 | 2 |
| Blades | Laser | - | - | 1500 | 1.25 | 400 | 1.5 |
| Operation | Tool Diameter (mm) | Feed rate (mm/min) | Spindle Speed (rpm) | Depth of Cut (mm) | Stepover (mm) | |
| Roughing | Model area clearance 3-axis | Ø 16 Flat End Mill | 175 | 1150 | 1 | 12 |
| Blade Area clearance 5-axis | Ø 8 Ball Nose | 800 | 2000 | 0.5 | 0.8 | |
| Finishing | Blade Finishing | Ø 6 Ball Nose | 1200 | 3000 | 0.2 | 0.2 |
| Hub Finishing | Ø 6 Ball Nose | 1200 | 3000 | 0.2 | 0.2 | |
| Mechanical properties | Without interlayer machining | With Interlayer machining |
|---|---|---|
| Microhardness (HV) | 152±6 | 178±4 |
| Ultimate tensile stress (Mpa) | 444±3 | 487±2 |
| Method | Strategy | Deposition | Interlayer machining | Roughing | Finishing | Total Time | ||||
| 3-axis | 5-axis | 3-axis | 5-axis | 3-axis | 5-axis | Blade | Hub | |||
| (measured in minutes) | ||||||||||
| Subtractive | Machining | - | - | - | - | 960 | 2212 | 140 | 224 | 3536 |
| HLM | Planar 5-axis |
61 | 194 | 90 | - | - | - | 322 | 224 | 891 |
| Conformal 5-axis | 125 | 170 | 60 | 64 | 10 | - | 140 | 224 | 792 | |
| Method | Strategy | Actual volume of impeller (cm3) | Volume before final machining (cm3) | Change in volume (cm3) |
Material wastage (%) |
|---|---|---|---|---|---|
| Subtractive | Machining | 428849.49 | 1654048.53 | 1225199.04 | 74.07 |
| HLM | Planar 5-axis with MIG Source | 493068.30 | 64,218.81 | 13.02 | |
| Planar hub with MIG and conformal blades with LASER | 472953.20 | 44,103.71 | 9.30 |
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2024 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (http://creativecommons.org/licenses/by/4.0/).