

Submitted:
29 July 2026
Posted:
31 July 2026
You are already at the latest version
Abstract
Nitric acid production is among the most significant industrial point sources of nitrous oxide, which is a greenhouse gas with a global warming potential approximately 298 times that of carbon dioxide, yet the large installed base of legacy dual-pressure plants continues to operate with non-selective catalytic tail gas treatment systems that offer limited greenhouse gas abatement and impose rigid thermal constraints on the gas turbine cycle. A steady-state digital twin of an industrial dual-pressure nitric acid plant producing 52 t per hour of 60 wt.% nitric acid is developed, validated against measured plant data, and used to evaluate two selective catalytic retrofit configurations. The first heats raw tail gas to catalyst ignition temperature using the existing process heater, then raises the purified gas to turbine inlet conditions by mixing with flue gas from a newly installed combustion chamber. The second achieves the required temperature rise internally through catalytic fuel gas oxidation within an additional catalyst shelf in a two-bed reactor, eliminating supplementary combustion equipment entirely. The first configuration reduces total greenhouse gas emissions by 37% in carbon dioxide equivalent terms, eliminates ammonia slip, and enables a 5% production capacity increase worth 5.75 million EUR per year, at a capital cost of 4.77 million EUR and a discounted payback period of 16 months. The second achieves a 43% emissions reduction at a capital cost of 1.34 million EUR, reduces annual utility costs by 1.75 million EUR, and recovers its investment within 2.6 months without increasing electricity demand. The results demonstrate that selective catalytic tail gas treatment retrofit is a value-generating investment rather than a compliance cost. Projected across the global fleet of unabated dual-pressure plants, equivalent adoption could reduce sectoral nitrous oxide emissions by more than 21 Mt of carbon dioxide equivalent per year, representing over half the identified global industry mitigation potential.
Keywords:
nitric acid
; tail gas treatment
; process simulation
; energy saving
; emission reduction
1. Introduction
1.1. State-of-the-Art Analysis
Nitrogen-based fertilisers are indispensable in sustaining modern agricultural productivity, yet their widespread use is a major contributor to environmental degradation, particularly through emissions of reactive nitrogen compounds. The primary concern focuses on nitrous oxide, a potent greenhouse gas with approximately 298 times the global warming potential of carbon dioxide over a 100-year period [1]. Additionally, nitrogen fertilisers contribute to ammonia volatilisation, which affects air quality and leads to secondary particulate formation, and to nitrate leaching, which causes groundwater contamination.
Nitric acid plays a central role in the global production of nitrogen-based fertilisers and is one of the most important commodity chemicals in the industrial sector. Nitric acid is industrially synthesised through three primary process routes, all of which are well-established: the mono-pressure, dual-pressure, and high-pressure processes [2]. Recent simulation-based optimisations using the ProSimPlus process modelling environment have demonstrated significant improvements in the mono-pressure process. These include a 55% reduction in NOx emissions and an 18% increase in nitric acid productivity, primarily achieved through advanced reactor design and refined operating conditions [3]. However, a key limitation of this optimised configuration is its reliance on a cooling water supply maintained at 5 °C to support efficient gas-phase reactions and condensation processes. The generation of such low-temperature cooling water imposes an additional energy burden, thereby partially offsetting the gains in energy efficiency and posing challenges for implementation in regions with limited access to low-cost cooling utilities. The dual pressure process for nitric acid production has the capability to increased yield, achieving higher concentrations [2]. The notable benefit of dual pressure methodology is its operation at a lower oxidation pressure, which diminishes the detrimental effects on the catalyst, a critical factor given the high costs and lower nitric acid concentration at the condenser exit. This enhances the acid’s solubility in water for more efficient absorption processes. Process intensification of NO oxidation at nitric acid plants under different pressures and temperatures was investigated, and the potential for extra heat recovery with reduced investment cost [4].
The manufacture and utilisation of nitric acid raise substantial environmental issues, primarily due to the release of nitrous oxide (N₂O), a highly potent greenhouse gas generated during the catalytic oxidation processes. Industrial nitric acid production facilities rank among the most significant point sources of anthropogenic N₂O emissions worldwide. In response to these concerns, extensive research and financial resources have been allocated toward the development of abatement technologies [5]. These include the implementation of secondary and tertiary catalytic systems designed to capture or decompose N₂O emissions prior to their atmospheric release, thereby mitigating their environmental impact [6]. As reported recently, a reduction of N2O emissions by 690 kilotons per year of CO2 equivalent using a new catalyst [7] and [8]. Catalyst ageing significantly impacts operational expenses and N2O emissions, leading to substantial research initiatives aimed at addressing these challenges [9]. Actually, tail gas treatment in nitric acid production can be treated by extended absorption of NO2, selective catalytic NOx reduction with ammonia [10] and non-selective NOx reduction with hydrogen and natural gas [11]. Different kinds of catalysts were investigated and tested. Three methods for the removal of N2O utilising a promoted Fe-ZSM-5 catalyst have been investigated under conditions that simulate the off gases produced by a nitric acid plant [12]. The pressure elevation is essential, as reported by the researchers, and the most difficult component is methane. The ageing of Fe-zeolite catalysts was investigated, and recommendations for industrial use were proposed [9]. The negative impact of NOx presence in tail gas was investigated using a double-promoted cobalt spinel catalyst, which concluded that even a low concentration of NOx affects it seriously [13]. Uhde EnviNOx technology may achieve N2O removal rates of 98–99% as reported in [14], and a special configuration of the reactor is needed to perform the process. A nickel-based catalyst demonstrated the conversion of N2O to 76% at 400 °C [15]. Measurement and monitoring of emissions have improved with the integration of static chamber methods, eddy covariance systems, and process-based modelling tools. These tools support more accurate emissions inventories and inform mitigation strategies [16].
The investigation of process parameters of a mono-pressure nitric acid plant by process simulation was performed by issuing the comprehensive mathematical model [17]. A comprehensive exergy destruction analysis performed on nitric acid production plants based on the Ostwald process has revealed significant opportunities for enhancing overall energy efficiency [6]. The simulation of the Ostwald process was performed in [18] to understand the process thermodynamics, but the concentration of the final acid reaches 35.3% wt. Exergy analysis, a powerful thermodynamic tool, has also been employed to assess the environmental impacts associated with chemical processes [2]. This approach has been further refined through integration with sustainability metrics, leading to measurable improvements in system performance. For example, optimisation of compressor operating conditions, specifically through pressure adjustments, has demonstrated a 3% increase in exergy efficiency [19]. In parallel, process simulations of nitric acid plants have largely concentrated on identifying optimal operational parameters to improve performance and product yield [20]. These simulations have been carried out using advanced process modelling tools such as Aspen HYSYS [21] and Aspen Plus [22], enabling detailed investigations into parameter variations and their influence on the concentration of nitric acid in the final product stream. In addition to exergy and process simulations, heat integration strategies have also been explored to further optimise plant efficiency. Notably, researchers have applied pinch analysis to redesign the heat exchanger network within nitric acid plants. This methodology has uncovered the potential for utility savings of up to 14%, even when excluding broader process modifications and specific utility adjustments [23]. Collectively, these studies underscore the multifaceted opportunities for improving the energy and environmental performance of nitric acid production through integrated thermodynamic, simulation-based, and process optimisation approaches.
Despite extensive research in nitric acid production, a significant gap remains in the modelling of the entire dual-pressure process, particularly in relation to industrial-scale units. This gap includes a comprehensive examination of various tail gas treatment options and their effects on the overall performance of the process. Addressing this inadequacy is crucial, as the selection and optimisation of tail gas treatment technologies can substantially influence emission reductions, energy efficiency, and economic viability. Therefore, further studies should focus on developing detailed models that integrate these variables, facilitating a deeper understanding of how tail gas management strategies can enhance the performance of dual-pressure nitric acid production.
1.2. Problem Statement
The objective of this study is to identify and develop potential strategies for enhancing the exhaust gas cleaning system associated with the production of nitric acid (60%wt) in dual-pressure power technology units. This initiative is driven by the pressing need to enhance the environmental safety of these industrial processes while concurrently increasing productivity and energy efficiency. The operational units, originally designed and constructed 30 years ago, continue to demonstrate competitive key performance indicators, showing that they still possess significant potential for further improvements. A critical component in the technological framework of these units is the catalytic exhaust gas purification system for nitrogen oxides. This system employs high-temperature catalytic reduction techniques, utilising natural gas as a reducing agent. The use of a non-selective catalyst not only reduces the nitrogen oxides but also harnesses the residual oxygen present in the exhaust gases to elevate the temperature of the exhaust stream to requisite levels. This heated gas is subsequently utilised as a working fluid in the gas turbine of the main drive unit, contributing to the overall energy efficiency of the process. Despite these advancements, the existing exhaust gas cleaning strategy, which relies on traditional non-selective catalysts, is accompanied by several limitations, including:
- Challenges in maintaining a stable exhaust gas temperature prior to reaching the gas turbine, due to the strict dependency of the temperature on the oxygen volume fraction in the exhaust gas.
- The formation of by-products in the treated exhaust gases, such as carbon monoxide and ammonia.
- Significant pressure losses across the catalyst layer.
- Contamination of the purified exhaust gases with nitrogen oxides from the gas turbine cooling system, which is affected by unpurified exhaust emissions.
- The high cost and limited availability of original catalyst materials.
The scientific contribution of this study lies in the investigation of the environmental, energy, and economic performance of tail gas treatment options for the typical dual-pressure nitric acid plant. It emphasises the output parameters of the tail gas treatment unit in conjunction with the overall performance of the plant. The study offers both research findings for specific process simulations and practical results, including opportunities for yield enhancement, reduction of N2O and NOx emissions, and improved energy efficiency.
2. Materials and Methods
2.1. General Framework and Workflow
The approach employed in this study is based on simulating the existing processes of a dual-pressure nitric acid plant and investigating different options for tail gas treatment. This approach aims to investigate how changes to the gas treatment process affect the overall performance, e.g., emissions, energy use and plant throughput. The process changes are supplemented by economic analysis to demonstrate potential commercial attractiveness. The general workflow includes the following process steps:
- Plant data acquisition including plant layout, composition of feedstock, products and utilities, operation modes, equipment configuration and regulation strategy.
- Definition of reaction sets and equations for chemical and thermodynamic equilibria.
- Building the base-case simulation model including the process morphology, recycles and energy recovery.
- Validation of model adequacy based on industrial data.
- Changes in tail gas treatment and approval of the key process parameters.
- Process performance assessment (energy, emissions, yield).
- Economic assessment of the proposed solutions.
- Comparison of base case and proposed gas treatment options.
2.2. Approach Description
Given that the catalysts utilised in the catalytic treatment systems of these units have become outdated, necessitating their replacement with modern, more efficient alternatives, a comprehensive analysis of the unit's operation was conducted. This investigation revealed several areas of potential improvement that could not only enhance the quality of exhaust gas purification but also elevate technical and economic performance while addressing various technical challenges. The non-selective catalysts currently available from leading global manufacturers can effectively mitigate nitrogen oxide emissions, including those of dinitrogen oxide. However, the inherent drawbacks of non-selective catalysts persist. Implementing selective catalysts requires modifications to the exhaust gas cleaning unit's configuration due to differences in operational temperature requirements between selective and non-selective catalysts. Specifically, the purified exhaust gas, which is employed as a working fluid in the gas turbine of the main drive unit, must meet specific parameters to ensure adequate power delivery during expansion. Two strategies to facilitate the integration of selective catalysts in the exhaust gas purification unit of the dual-pressure nitric acid plant have been formulated:
- Option 1. This strategy involves heating the unpurified exhaust gas to the ignition temperature of the selective catalyst using the existing heater. Following this initial purification step, the gas is subsequently raised to the required temperature by mixing it with flue gases in a newly installed combustion chamber, as shown in Figure 1a.
- Option 2. In contrast to Option 1, this strategy heats the purified exhaust gas by oxidising the fuel gas using the residual oxygen present in the exhaust gas. For this purpose, an additional catalyst layer is introduced within the catalytic purification reactor, facilitating the catalytic oxidation of the fuel gas and thereby increasing the temperature of the purified exhaust gas to the desired level (Figure 1b).
2.3. Chemical Reactions
Nitric acid is synthesised from ammonia and oxygen as primary feedstocks, with the chemical conversion represented by the following reaction sequences (Eq. 1-15).
Ammonia conversion
Nitrous gas cooling and absorption of NOx
Tail gas treatment
2.4. Modelling Issues
The phase equilibria in ammonia conversion, nitrous gas cooling and nitrogen dioxide absorption is defined by the extended non-random two-liquid model (extended NRTL), which is better predict the vapor-liquid-liquid equilibria in chemical systems [24]. This model is described by the equation (16) - (18) for component i with mole fraction xi in liquid phase, activity coefficient γi, interaction coefficient gij for components i and j, non-randomness parameter αij and ternary effect on the activity coefficient of the component Δt lnγi.
where parameters can be defined as follows:
The Peng-Robinson-Strijek-Vera [25] equation of state (Eq. 19) was used for calculation of the fluid phase equilibria in the tail gas treatment section. This modification demonstrated improved predictive capability of binary mixtures [26].
where parameters are defined from Eq. 20-24:
The simulation model of the base case and different options of tail gas treatment was implemented in Aspen HYSYS environment version 12 [27]. The main operation units and processes are simulated by the following approaches:
- Ammonia conversion: conversion reactions;
- Nitrous gas cooling: chemical equilibrium and heat transfer;
- Heat exchangers: sizing-based rating;
- Gas washer, absorber and purge: rate-based radfrac model;
- Compressors and turbines: working curve-based rating;
- Tail gas treatment: ranged conversion reactions.
2.5. Mass and Energy Balances
2.6. Economic Assessment
The economic evaluation of the proposed modifications to tail gas treatment was conducted by analysing the capital expenditure (CAPEX) associated with new equipment in Eqs. (27-32) and applying annualization parameters in Eqs. (33-34). Correction factors for temperature, pressure and material were applied for new operation units [28]. The capital costs for the equipment were estimated utilising the Chemical Engineering Indexes [29] and the Marshall & Swift cost indices [30]. It is important to note that the CAPEX for actual projects can exhibit significant variability, influenced by factors such as installation, revamping, and other related expenditures, which can potentially increase total capital costs by a factor of four. The acceptable accuracy for CAPEX evaluations in industrial projects usually adheres to AACE International Recommended Practice No. 18R-97.
where QS is equipment capacity.
The following process utilities are considered in the specific nitric acid plant:
- steam (2.2 MPa);
- electricity;
- cooling water;
- natural gas (97.4% CH4, 2.6% N2);
- N2/H2 mixture (75% H2, 25% N2).
Economic assessment presumes the use of the following economic variables:
| Plant load factor | 95% | |
| Specific CO2 emission (natural gas) | 0.201 kgCO2/kWh | [31] |
| Average life-cycle CO2 equivalent emissions of electricity | 0.490 kgCO2/kWh | [32] |
| Nat. gas price | 0.410 EUR/m3 | [33] |
| NOx to CO2 equivalent | 298 kg/kg | [34] |
| NH3 to CO2 equivalent | 1.69 kg/kg | [34] |
| Electricity price | 0.240 EUR/kWh | [35] |
| Nitric acid price (Europe, 2026) | 270.00 EUR/t | [36] |
| CO2 equivalent price (2026) | 73.90 EUR/t | [37] |
| Steam price | 15.00 EUR/t | [38] |
| Lang factor | 4 | |
| Interest rate | 10% | |
| Project lifetime | 5 |
2.7. Assumptions
The process simulation and performance assessment were conducted under a consistent set of simplifying assumptions to ensure model robustness, numerical stability, and comparability between the base case and the proposed retrofit options. These assumptions reflect standard steady-state modelling practice in simulation software and typical simplifications adopted in nitric acid plant simulations.
The feedstock flow rate was assumed constant during all simulations. Ammonia, air, water, natural gas, and utility streams were assumed to be supplied under steady nominal conditions, corresponding to full-load industrial operation. The model was developed in steady-state mode. Therefore, transient phenomena such as start-up, shutdown, load variations, catalyst ageing, and control system dynamics were not considered. All mass and energy balances represent continuous, stationary operation. Heat losses to the surroundings were neglected. Process equipment and pipelines were assumed to be perfectly insulated unless heat exchange was explicitly defined in the model. This assumption allows clear evaluation of internal heat integration without introducing uncertainties related to ambient heat transfer. Pressure drops in interconnecting pipelines were not considered. Only pressure changes explicitly defined within unit operation models (e.g., compressors, turbines, valves, reactors) were considered. Physical properties of pure components were taken from the Aspen HYSYS database, and binary interaction parameters available in the selected property packages were used without additional regression.
In accordance with standard Aspen HYSYS steady-state simulations, the following assumptions were used:
- Perfect mixing was assumed within equilibrium and conversion reactor models.
- Chemical reactions were modelled using either conversion-based or equilibrium-based approaches with predefined stoichiometry and fixed conversion ratios where applicable.
- No catalyst deactivation or activity loss over time was considered.
- Equipment performance (compressors, turbines, heat exchangers) was based on rating or specified efficiency parameters assumed constant at nominal conditions.
- Thermodynamic equilibrium was assumed to be achieved in the separation and absorption stages, where equilibrium or rate-based RadFrac models were applied.
- No mechanical degradation, fouling, or scaling effects were included in heat transfer calculations.
- Utility systems (steam, electricity, cooling water) were considered available at constant pressure, temperature, and unit cost.
These assumptions are commonly applied in steady-state process simulations and are suitable for comparative assessment of process modifications. Additional assumptions specific to the dual-pressure nitric acid process were adopted:
- The ammonia-to-NO conversion was represented by predefined conversion reactions reflecting industrial selectivity. Side reactions leading to N₂ and N₂O formation were included via fixed conversion fractions consistent with validated plant data. Reactor temperature was determined from the energy balance assuming adiabatic operation.
- Gas-phase oxidation of NO to NO₂ and subsequent absorption were modelled assuming thermodynamic equilibrium in accordance with the extended NRTL model for vapor–liquid equilibria. Mass transfer limitations were not explicitly modelled beyond the rate-based absorber formulation.
- The NO₂ absorption ratio was assumed to correspond to validated plant performance (approximately 99%), and absorber hydraulic limitations were not considered.
- The catalytic reduction of NOx and N₂O was modelled using ranged conversion reactions based on literature data and industrial catalyst performance. Complete and uniform contact between gas and catalyst was assumed. No catalyst aging, poisoning, or deactivation was considered.
- The purified tail gas was assumed to meet the required temperature and composition specifications for turbine operation. Turbine isentropic efficiency was assumed constant, and mechanical losses were incorporated through fixed performance parameters.
- The nitric acid concentration at plant outlet was fixed at approximately 60 wt.% as per industrial design, and variations in product specification were not considered unless explicitly analysed in retrofit scenarios.
- Steam production from waste heat recovery was calculated assuming ideal heat transfer within specified exchangers and no steam leakage or condensate losses.
- The catalyst cost remains unchanged when applying both retrofit options.
These modelling assumptions ensure a consistent and validated representation of the dual-pressure nitric acid plant while maintaining computational tractability. Since identical assumptions were applied to the base case and both retrofit options, the comparative analysis of environmental, energy, and economic performance remains methodologically coherent and reliable.
3. Case study
The nitric acid plant employs a dual-pressure process to produce nitric acid 60%wt as presented in simulation PFD (Figure 2). The ammonia conversion occurs at a pressure of 0.42 MPa, while nitrogen oxide absorption is conducted at a pressure of 1.1 MPa. The valuable by-product of the process is superheated steam generated at a pressure of 4.1 MPa. The primary feedstocks for the process include liquid ammonia, natural gas, cooling and desalinated water, electricity, and atmospheric air. Before processing, the liquid ammonia is vaporized. The heat generated during the scrubbing of nitrous gases before compression serves as the source of heat for ammonia evaporation, facilitating a reduction in the nitrous gas temperature before compression and minimizing the steam required for ammonia evaporation. Following evaporation, gaseous ammonia is purified and subsequently heated using the heat from compressed air, which is delivered to the unit for the purpose of removing dissolved nitrogen oxides from the product nitric acid. The heated ammonia is then directed to the conversion reactor, where it undergoes catalytic oxidation to nitrogen oxide, utilizing atmospheric oxygen as the oxidizing agent. The atmospheric air is pre-filtered to remove mechanical impurities, compressed to the requisite pressure, and supplied to the reactor. The ammonia oxidation process occurs at temperature of approximately 860°C. The heat generated from the nitrous gas produced in the reactor is recovered to generate water vapor and heat demineralized water (Figure 3a).
Subsequently, the nitrous gas is cooled down using cooling water, resulting in the release of some process water in the form of nitric acid condensate. This condensate is used as an absorbent in the absorption process and in the scrubbing of nitrous gas prior to compression. The cooled nitrous gas is then washed with nitric acid condensate to eliminate by-products such as ammonium nitrate, before being compressed to the necessary absorption pressure. The heat generated during the compression and oxidation of nitrous gas is utilised to preheat the feed water supplied for steam generation. Before entering the absorption process, the nitrous gas is cooled with water. During absorption, nitrogen oxides are extracted from the nitrous gas, resulting in the formation of nitric acid. Desalinated water and nitric acid condensate serve as absorbents, while cooling water is used to dissipate the heat of the reaction. The final nitric acid, containing approximately 60% nitric acid by mass, is purified from dissolved oxides through air purging in the purge column. The purge gas is directed for compression alongside the nitrous gas, while the product acid is stored or dispatched to consumers. After the absorption phase, the tail gas is treated to remove aerosols before being subjected to heating. This heating occurs in two stages. In the first stage, the exhaust gas is heated through heat recovery of waste gas from the gas turbine and flue gases from the radiant zone of the fire heater. The second stage involves dosing the exhaust gas into the radiant tubes of the fire heater, with natural gas serving as the fuel. The subsequently heated exhaust gas is then routed for nitrogen oxide purification (Figure 3b).
The purification of the exhaust gas is provided via catalytic reduction of nitrogen oxides, utilising natural gas as the reducing agent. Prior to the reduction process, an exothermic reaction between natural gas and the oxygen present occurs on the catalyst, raising the exhaust gas temperature to 750°C-770°C. The hot, purified exhaust gas is directed into the gas turbine, which is the primary component of the gas turbine drive. Additionally, the gas turbine unit is equipped with a steam backpressure turbine as an auxiliary component. After passing through the gas turbine, the exhaust gas enters the recuperative zone of the exhaust gas heater, where it transfers heat to the unpurified exhaust gas before being released into the atmosphere. The mass balance of the considered nitric acid plant is shown in Table 1.
Capacity factor (QS) of new equipment for tail gas treatment:
- Gas treatment reactor (volume): 40 m3;
- Air compressor (power): 3,155 kW;
- Combustion chamber (volume): 9 m3;
- Ammonia evaporator (heat transfer area): 4 m2;
- Ammonia filter (area): 10 m2;
- Ammonia heater (heat transfer area): 4 m2.
4. Results and Discussion
4.1. Model Validation
The steady-state model developed for the dual-pressure nitric acid plant was validated using measured industrial data under nominal operating conditions. Table 2 compares plant measurements and simulation results for key process parameters, including feed preparation, ammonia oxidation, heat recovery, compression, absorption, tail gas treatment, and utility consumption. The close agreement between measured and simulated values confirms the adequacy of the selected thermodynamic models, reaction schemes, and unit operation configurations.
Minimal deviations are observed in the primary feed and core reaction parameters. The ammonia flow rate differs by −0.1%, and the feed water flow rate deviates by −0.2%. The ammonia-to-air ratio is reproduced with a deviation of 0.1%, while the ammonia conversion ratio matches the measured value at 96.0%. The conversion reactor temperature deviates by −1.0%, which is acceptable given the highly exothermic nature of ammonia oxidation and the sensitivity of temperature to small variations in reaction enthalpy and heat capacity data. These results indicate that the conversion-based reaction model and energy balance formulation provide an accurate description of the oxidation stage.
The waste heat recovery section is accurately represented in the model. The waste-heat outlet gas temperature and medium-pressure steam consumption are reproduced exactly, while the medium-pressure steam temperature deviates by 0.7%. These minor differences result from simplifications in heat exchanger modelling, such as neglecting external heat losses and fouling effects. The air compressor outlet pressure is predicted without deviation; however, the outlet temperature differs by 2.5%, representing one of the largest deviations in the dataset. This discrepancy is attributable to the model's use of constant isentropic efficiency and idealised compressor performance curves, whereas actual industrial compressors operate with variable efficiency due to mechanical and thermal losses. The nitrous gas compression and washing section demonstrates strong agreement between the model and plant data. The nitrous compressor outlet pressure and temperature deviate by 0.0% and −0.2%, respectively. The gas washer top and bottom temperatures show deviations of 2.2% and 0.6%. The higher deviation at the washer top temperature is due to simplifications in rate-based absorption and heat transfer modelling, such as the assumption of ideal insulation and a uniform phase distribution. The predicted NO₂ absorption ratio of 99.1% differs from measured data by only 0.1%, indicating that the extended NRTL thermodynamic framework and absorber configuration reliably represent mass transfer and phase equilibrium.
The tail gas treatment and turbine section maintain acceptable predictive accuracy. The tail gas temperature before the reactor is reproduced exactly, while the temperature after the reactor deviates by −0.9%. This minor difference arises from modelling catalytic conversion with fixed conversion ratios rather than from detailed kinetic expressions. The gas turbine outlet temperature deviates by 1.9%, consistent with the assumption of constant turbine efficiency and the neglect of minor mechanical and heat losses. The exhaust tail gas temperature exhibits the highest deviation at 9.3%, which is due to the combined effects of simplified heat recovery modelling, neglected external heat losses, and the absence of detailed turbine cooling air mixing phenomena. Despite this deviation in absolute exhaust temperature, the emission composition is reproduced accurately.
For environmental performance indicators, the predicted NOx concentration in the exhaust tail gas deviates by −4.7%, which is among the largest composition-related deviations. This difference is acceptable given the sensitivity of NOx formation and reduction to small variations in oxygen concentration, temperature, and catalyst activity, all of which are modelled using conversion-based assumptions rather than detailed kinetic mechanisms. The nitric acid concentration in the product stream deviates by only −0.1%, and the plant yield, expressed as 100% HNO₃ production, differs by 0.4%, confirming the robustness of the overall mass balance.
4.2. Energy Performance and Plant Yield
Modification of the tail gas treatment system significantly influences the overall energy balance of the dual-pressure nitric acid plant. Table 3 shows that the base case operates with a natural gas consumption of 3,528 STD m³/h and requires 221 STD m³/h of the N₂/H₂ mixture for non-selective catalytic reduction. Both retrofit options eliminate the need for the N₂/H₂ mixture, indicating a fundamental change in the reduction mechanism. However, natural gas demand differs between the two scenarios: Option 1 increases consumption to 3,763 STD m³/h, while Option 2 reduces it to 3,379 STD m³/h. This variation reflects the distinct thermal management strategies implemented in each option. In Option 1, additional fuel is required in the newly installed combustion chamber to achieve the target turbine inlet temperature after selective catalytic purification. In contrast, Option 2 utilises residual oxygen in the tail gas for catalytic fuel oxidation within the reactor, enabling temperature control with reduced external fuel input.
Electricity consumption further differentiates the two retrofit solutions. Option 1 requires an additional 3,155 kW due to the installation of a new air compressor supporting the modified gas treatment configuration. In contrast, Option 2 does not increase electrical demand, as the necessary temperature rise is achieved internally within the catalytic reactor. From an energy integration perspective, Option 2 provides a more compact and thermally integrated design. Differences in steam generation and consumption patterns further highlight these distinctions. Option 1 increases steam generation from 64.1 t/h to 70.0 t/h due to enhanced heat recovery associated with higher combustion intensity. Simultaneously, steam consumption decreases from 41.4 t/h to 29.0 t/h, indicating improved internal heat utilization. Option 2 maintains steam generation at the base-case level (64.1 t/h) and slightly reduces steam consumption to 31.5 t/h. Although both options improve the steam balance, the additional electricity requirement in Option 1 partially offsets its thermal advantages when total energy costs are considered.
The impact on plant yield, as shown in Figure 4, provides an additional perspective. Option 1 increases nitric acid production by approximately 5%, which is a significant improvement for a plant operating near its design capacity. This yield enhancement results from more stable tail gas temperature control and improved process conditions, enabling higher throughput without negatively affecting turbine operation. In contrast, Option 2 does not significantly increase plant capacity and maintains production levels similar to the base case. Therefore, although Option 2 achieves superior fuel efficiency, it does not support production intensification to the same extent as Option 1.
A critical assessment of the results indicates that Option 1 prioritises productivity and steam recovery, though at the cost of increased fuel and electricity consumption. In contrast, Option 2 emphasises fuel efficiency and reduced operational energy costs, with minimal effect on throughput. The choice between these alternatives should align with the plant's strategic objectives. If capacity expansion and revenue growth are prioritised, Option 1 may be justified despite its higher utility requirements. Conversely, if minimising energy consumption and operating costs is the primary objective, Option 2 offers a more energy-efficient, thermodynamically integrated solution. Both configurations improve internal heat utilisation compared to the base case, but they differ fundamentally in how they balance energy intensity with production gains.
4.3. Environmental Performance
The environmental performance of the two retrofit options is evaluated on the basis of the direct emissions of greenhouse gases and nitrogen oxides reported at the stack, as summarised in Table 4 and illustrated in Figure 5. The analysis quantifies changes in N₂O, NO, NO₂, CO₂, and NH₃ mass flow rates relative to the base case and interprets the cumulative effect through the CO₂-equivalent metric, applying a global warming potential of N₂O and NOx.
N₂O is the dominant environmental concern in nitric acid production and represents the primary driver for tail gas treatment retrofit. In the base case, the N₂O emission rate reaches 39.2 kg/h, consistent with the typical output of a dual-pressure plant in which tertiary abatement is absent or based on a non-selective catalyst. Both retrofit options achieve substantial N₂O reduction: Option 1 reduces the flow to 13.0 kg/h, corresponding to a 66.8% decrease, while Option 2 achieves 12.4 kg/h, a reduction of 68.4%. The marginal superiority of Option 2 in N₂O abatement reflects its higher reactor operating temperature, sustained by the catalytic oxidation of fuel gas within the reactor itself, which maintains the iron-zeolite catalyst above the threshold for efficient N₂O decomposition across a broader range of load conditions. These reductions are significant in absolute terms: on an annualised basis (8,000 operating hours per year), the N₂O mass flow reductions correspond to approximately 210 t/y and 215 t/y for Options 1 and 2, respectively, equivalent to CO₂ reductions in the range of 62,500–64,000 t CO₂-eq/y from N₂O alone.
The selective catalytic reduction with ammonia, common to both retrofit configurations, reduces total NOx emissions markedly. In the base case, the combined NO and NO₂ emission is 14.9 kg/h. Option 1 reduces this to 10.6 kg/h (−28.9%), and Option 2 achieves the lowest NOx output of 8.8 kg/h (−40.9%). The stronger NOx reduction in Option 2 is consistent with its reactor design: the two-shelf configuration with an additional catalyst layer provides a longer gas residence time in the SCR zone, enabling more complete conversion of residual NOx even at the elevated temperatures characteristic of this variant. The elimination of NH₃ slip from 2.4 kg/h in the base case to 0.0 kg/h in both options is also noteworthy. In the base case, residual ammonia indicates incomplete reaction over the non-selective catalyst and represents a secondary air quality concern; both selective catalyst configurations eliminate this by-product entirely, consistent with the precise stoichiometric NH₃ dosing applied in the SCR stage.
The CO₂ emission profile reflects the contrasting thermal management strategies of the two options. Option 1 increases direct CO₂ emissions from 6,882 kg/h (base case) to 7,475 kg/h (+8.6%), attributable to the higher natural gas consumption in the newly installed combustion chamber required to bring the purified gas to turbine inlet temperature. Option 2, in contrast, reduces CO₂ emissions to 6,750 kg/h (−1.9%) by utilising residual oxygen in the tail gas for internal catalytic oxidation, thereby decreasing net fuel combustion. This fundamental difference underscores the thermodynamic trade-off: Option 1 achieves a greater throughput gain at the cost of higher carbon intensity per unit of production, while Option 2 operates with near-base-case fuel consumption and lower direct CO₂ output.
The total environmental impact, expressed as cumulative CO₂-equivalent emissions and shown in Figure 5c, captures the dominant contribution of N₂O reduction. Despite the modest increase in direct CO₂ under Option 1, both retrofit configurations deliver substantial reductions in total CO₂-equivalent output. Option 1 achieves a 37% reduction and Option 2 a 43% reduction in CO₂-equivalent emissions relative to the base case. The larger relative gain of Option 2 is explained by its combination of lower N₂O residual (12.4 vs. 13.0 kg/h), lower NOx, and reduced CO₂ output. All three greenhouse-relevant species improve simultaneously, without a CO₂ penalty from supplementary combustion.
The N₂O abatement efficiencies reported here of 66.8% and 68.4% for the two options are consistent with the performance range achievable by tertiary selective catalytic systems and fall within the operational envelope of commercially deployed technologies such as the EnviNOx® process, which is reported to achieve N₂O removal rates of 98–99% under optimal conditions [14]. The gap between the values obtained in this study and the upper-bound literature values reflects the specific constraints of the retrofit scenario: the selective catalyst must operate within the thermal window imposed by the existing heater and the turbine inlet temperature requirement, which limits the achievable ignition temperature and therefore the depth of N₂O decomposition. Future plant designs conceived from the outset with tertiary abatement integrated into the heat recovery network could approach the higher removal efficiencies reported in dedicated installations. From a regulatory standpoint, the CO₂-equivalent reductions demonstrated here are directly relevant to the EU Emissions Trading System (EU ETS), under which nitric acid producers are obligated to surrender allowances for N₂O emissions. The emission cost savings of approximately 5.2 and 6.1 million EUR/year estimated for Options 1 and 2 (Table 5) are consistent with the scale of the environmental improvements quantified in Table 4, confirming the internal consistency of the environmental and economic analyses. The results confirm that selective catalytic tail gas treatment, even under the constraints of a retrofit into an existing dual-pressure plant, constitutes a technically effective and environmentally meaningful abatement measure. The choice between options should therefore be informed not only by economic payback criteria but also by the plant operator's specific emission reduction commitments and carbon pricing exposure.
4.4. Economic Performance
The economic evaluation of the two retrofit options is structured around four principal financial components: annualised capital expenditure, changes in utility operating costs, revenue effects arising from changes in plant yield, and savings generated by the reduction of CO₂-equivalent emissions. These components are synthesised in Table 5, which provides the basis for comparing the overall commercial attractiveness of each option. Sensitivity analyses with respect to CAPEX uncertainty, nitric acid market price, and energy price are presented in Figure 6, Figure 7 and Figure 8, respectively. The annualisation of capital costs applies a 10% interest rate over a five-year project lifetime, consistent with Eqs. (33–34) and the economic assumptions defined in Section 2.4.
The CAPEX estimates reflect the different scope and complexity of the two retrofit configurations. Option 1, which requires a new combustion chamber, an additional air compressor, an ammonia evaporator, an ammonia filter, and an ammonia heater, carries a total capital cost of 4,771,557 EUR, annualised to 1,258,725 EUR/year. Option 2 introduces only an additional catalyst shelf within the reactor vessel, together with the associated ammonia dosing equipment, resulting in a substantially lower CAPEX of 1,340,663 EUR, annualised to 353,664 EUR/year. The capital cost ratio between the two options is approximately 3.6:1, a difference that is decisive in determining the relative payback performance and reflects the inherent advantage of the thermally integrated, reactor-internal approach adopted in Option 2. Both estimates were derived using the correlations of Peters, Timmerhaus, and West [30], with Chemical Engineering Plant Cost Index corrections [29] and a Lang factor of 4 applied to account for installation, interconnecting piping, instrumentation, and civil works, in accordance with AACE International Recommended Practice No. 18R-97.
The modification of utility consumption introduced by each option translates directly into operating cost changes, as summarised in Table 3 and monetised in Table 5. Option 1 incurs an additional utility cost of +4,794,569 EUR/year, driven by three simultaneous effects: (i) an increase in natural gas consumption from 3,528 to 3,763 STD m³/h (+235 STD m³/h), attributable to the combustion chamber fuel requirement; (ii) additional electricity demand of 3,155 kW from the new air compressor; and (iii) the cost of ammonia supply (127 STD m³/h) as SCR reductant. These are partially offset by the elimination of the N₂/H₂ mixture (221 STD m³/h) previously required for non-selective catalytic reduction, and by improved steam generation (from 64.1 to 70.0 t/h) combined with a reduction in steam consumption (from 41.4 to 29.0 t/h). In aggregate, however, the increased fuel and electricity demand outweighs the steam-side savings, producing a net utility cost penalty for Option 1. In contrast, Option 2 achieves a utility cost reduction of 1,750,090 EUR/year. The internal catalytic oxidation of fuel gas within the two-shelf reactor eliminates the need for a combustion chamber and the associated air compressor, reduces natural gas consumption to 3,379 STD m³/h (−149 STD m³/h relative to the base case), and requires no additional electricity. Together with the elimination of the N₂/H₂ mixture cost, Option 2 delivers a strictly favourable operating cost outcome at the utility level.
The 5% increase in nitric acid production achieved by Option 1, enabled by more stable tail gas temperature control and improved process conditions, generates an additional revenue of +5,752,166 EUR/year, calculated at the prevailing European nitric acid market price of 230 EUR/t (2024) [36]. This revenue contribution is the single largest positive cash flow item for Option 1 and is decisive in offsetting its utility cost penalty. Option 2, which does not significantly alter plant throughput, produces a negligible capacity-related revenue change of −112,347 EUR/year, reflecting minor process interactions rather than a structural throughput effect. The contrast between the two options on this dimension is fundamental: Option 1 is essentially a combined production-expansion and abatement investment, whereas Option 2 is a pure abatement measure with an improved energy cost profile.
Both retrofit options generate significant savings under the EU ETS, where N₂O emissions are accounted for at the current allowance price of 80.50 EUR/t CO₂-equivalent [37]. The reduction in N₂O, NOx, and NH₃ emissions quantified in Section 4.3 translates into emission cost savings of 5,227,499 EUR/year for Option 1 and 6,113,216 EUR/year for Option 2. The higher emission savings for Option 2 are consistent with its marginally superior greenhouse gas abatement performance (43% vs 37% total CO₂-equivalent reduction). Table 5 presents the payback period without accounting for emission cost savings, to isolate the purely operational and production-side economics from the regulatory incentive component. When emission savings are excluded, the payback periods are 16 months for Option 1 and 2.6 months for Option 2. When emission savings are incorporated, both payback periods shorten substantially, reinforcing the commercial case for both investments under current EU carbon pricing conditions.
The overall economic picture that emerges from Table 5 differentiates the two options sharply. Option 2 presents the stronger financial case by every metric: lower CAPEX (1,340,663 vs. 4,771,557 EUR), reduced utility operating costs (saving 1,750,090 EUR/year vs. a penalty of 4,794,569 EUR/year), and higher emission cost savings (6,113,216 vs. 5,227,499 EUR/year), yielding a payback period of 2.6 months an exceptionally short horizon for industrial retrofit investments. Option 1, despite its higher capital and operating costs, is made viable by the revenue contribution from the 5% capacity increase (5,752,166 EUR/year), which no other mechanism in Option 2 can replicate. The payback period for Option 1 of 16 months remains commercially attractive, particularly for operators whose primary objective is throughput expansion and who are positioned to benefit from nitric acid market pricing.
The robustness of the payback conclusions was assessed across three dimensions. Figure 6 presents the sensitivity of payback period to CAPEX variation for each option. Since CAPEX estimates at the AACE Class 4–5 level can vary by a factor up to four, this sensitivity is particularly relevant. For Option 2, the payback period remains below 12 months across the full range of capital cost scenarios considered, confirming its strong economic resilience to cost estimation uncertainty. For Option 1, the payback period is more sensitive to CAPEX increases due to the larger absolute investment but remains within commercially acceptable bounds provided the capacity revenue is realised. Figure 7 shows the dependence of economic performance on the nitric acid market price. Option 1 is more exposed to price volatility because its positive net cash flow is predicated on the revenue from the additional 5% production capacity. A sustained decline in nitric acid prices would lengthen the payback period of Option 1 disproportionately relative to Option 2, which is substantially insulated from product price risk by its operating cost savings structure. Figure 8 illustrates the impact of energy price variation. Given that Option 1 carries a net increase in natural gas and electricity costs, it is adversely affected by energy price increases. Option 2, conversely, benefits from higher energy prices, as its utility cost savings are proportionately amplified, further shortening an already short payback period.
The economic analysis confirms that both retrofit options offer commercially viable pathways for tail gas treatment upgrade in dual-pressure nitric acid plants. Option 2 is the superior choice from a purely financial standpoint, offering minimal capital outlay, reduced operating costs, and a near-immediate payback, making it immediately attractive to investors and plant owners seeking rapid returns. Option 1 is the appropriate choice when capacity expansion is the strategic priority, with its higher CAPEX and utility costs justified by the substantial incremental revenue from increased production. Under current EU carbon pricing, the emission cost savings reinforce the financial case for both options, and carbon price scenarios above the 80.50 EUR/t CO₂-eq baseline assumed here would further improve the economics of both configurations, particularly Option 2.
4.5. Global Impact on the Fertiliser Industry
Nitric acid is the essential intermediate in nitrogen-based fertiliser production, with global output reaching approximately 60 million tonnes per year in 2023 across roughly 500 production plants worldwide. Around 80% of this volume feeds the manufacture of ammonium nitrate, a critical nitrogen source for agricultural productivity [10]. The fertiliser industry as a whole is responsible for approximately 1.4% of annual global CO₂-equivalent emissions, broadly comparable to the total national emissions of a major European economy [11]. Within this, nitric acid manufacturing represents the dominant point-source of industrial N₂O, with total sectoral N₂O emissions estimated at 36.1 Mt CO₂-equivalent in 2020. Crucially, an estimated 63% of this total, some 22.5 Mt CO₂-equivalent, originates from plants operating without effective tertiary abatement and therefore constitutes a readily addressable mitigation potential [21].
The present study demonstrates that selective catalytic tail gas treatment applied to an existing dual-pressure nitric acid plant reduces the plant-level N₂O emission factor from 0.75 to approximately 0.24 kg N₂O per tonne of HNO₃ produced; a reduction of 66–68% depending on the retrofit configuration. Extending this performance to the global fleet of unabated plants requires contextualisation with IPCC-referenced emission factors. Medium-pressure dual-pressure plants without tertiary abatement typically operate with emission factors in the range of 5–7 kg N₂O per tonne HNO₃, with high-pressure plants reaching up to 12 kg N₂O per tonne [20]. Applying the 67% reduction efficiency demonstrated here to a conservative scenario in which 30% of global production, approximately 18 Mt HNO₃ per year, is subject to similar retrofit, yields a N₂O abatement potential of approximately 72 kt N₂O per year, equivalent to 21.5 Mt CO₂-equivalent per year. This represents approximately 60% of the total estimated unabated N₂O emission potential from the nitric acid sector globally. Under current EU ETS allowance pricing of 80.50 EUR per tonne CO₂-equivalent, this abatement potential carries an economic value of approximately 1.7 billion EUR per year, a figure that grows substantially as carbon prices tighten in line with EU climate policy trajectories. Even at a 10% global adoption rate, aggregate annual savings would reach 2.1 Mt CO₂-equivalent and generate approximately 170 million EUR in emission cost avoidance per year. These estimates are consistent with the order of magnitude of recently reported commercial deployments: the Clariant EnviCat® N₂O-S catalyst alone is reported to reduce emissions by 690 kt CO₂-equivalent per year at a single large-scale nitric acid complex in China [7], and by a further 275 kt CO₂-equivalent per year at a second facility [8], underscoring the material scale of per-plant impact from modern tertiary abatement systems.
The long-term transformation of the fertiliser industry extends beyond incremental abatement of existing plants to structural decarbonisation of the upstream ammonia supply chain. Green ammonia, produced via electrolysis of water using renewable electricity to generate hydrogen, followed by the Haber–Bosch synthesis, currently commands a production cost of USD 700–1,400 per tonne, compared to approximately USD 300–450 per tonne for conventionally produced grey ammonia. However, this premium is projected to narrow substantially: IRENA and IEA modelling indicates that with renewable electricity costs below USD 20 per MWh, green ammonia becomes cost-competitive with grey ammonia without carbon pricing, with production costs expected to converge toward USD 310–480 per tonne by 2030–2050. The IEA Sustainable Development Scenario projects that direct CO₂ emissions from the ammonia industry can be reduced by over 70% by 2050 relative to today, while a Net Zero Emissions trajectory requires a 95% reduction. Near-zero emission production capacity of approximately 8 Mt per year is scheduled to come online by 2030. The significance of these trajectories for nitric acid and fertiliser producers is twofold. First, decarbonised ammonia feedstock would substantially reduce the upstream Scope 1 and Scope 2 footprint of nitric acid synthesis, complementing the tail gas abatement measures examined in the present study. Second, ammonia is gaining traction as an e-fuel and hydrogen energy carrier, with the International Maritime Organisation projecting that ammonia could supply approximately 25% of the global shipping fuel mix by 2050. This dual role, as fertiliser precursor and as carbon-free fuel, is expected to drive global ammonia demand to 350 million tonnes per year by 2050, up from approximately 185 million tonnes today. Nitric acid plants operating with green ammonia feedstock and equipped with selective catalytic tail gas treatment would approach near-zero lifecycle N₂O and CO₂ emission profiles, consistent with the decarbonisation requirements of the EU's Farm to Fork Strategy and the broader Fit for 55 regulatory frameworks.
4.6. Limitations
The process model was developed exclusively in steady-state mode. Transient phenomena inherent to industrial operation, including plant start-up, scheduled and unscheduled shutdowns, load-following behaviour, and control system response, were not captured. In practice, N₂O and NOx emission rates are sensitive to transient conditions, particularly during catalyst warm-up and ammonia burner campaigns, and peak emissions during these periods may deviate substantially from the nominal values reported here. Dynamic modelling would be required to quantify these effects and to validate the stability of the proposed retrofit configurations under real operational variability.
The catalytic reduction of N₂O and NOx in the tail gas treatment reactor was modelled using fixed conversion fractions derived from literature data and validated plant measurements, rather than from detailed reaction kinetics. This approach captures steady-state performance at the design operating point but cannot represent the dependence of conversion efficiency on inlet concentration fluctuations, temperature gradients across the catalyst bed, or the spatial distribution of reactants. Furthermore, no catalyst deactivation, poisoning, or ageing was considered. Industrial iron-zeolite and vanadium-titania catalysts experience progressive activity loss over service lifetimes of several years, and the economic case for retrofit is sensitive to catalyst replacement frequency and cost factors not reflected in the current model.
Heat losses from process equipment and interconnecting pipelines were neglected by assuming perfect insulation throughout. Pressure drops in connecting piping were not considered. While these simplifications are standard in steady-state comparative assessments and are unlikely to alter the relative ranking of options, they introduce positive bias into energy recovery estimates and may cause modest overestimation of turbine power output and steam generation. The exhaust tail gas temperature, which showed the largest validation deviation at 9.3%, reflects these combined simplifications and should be noted when interpreting absolute emission concentrations.
Capital cost estimates were generated using equipment-scaling correlations from Peters, Timmerhaus, and West [30] with a Lang factor of 4, consistent with AACE Class 4–5 accuracy (expected accuracy: −30% to +50%). Actual project costs for revamping existing plants may deviate significantly from these estimates due to site-specific constraints, structural modifications, and installation complexity not captured by the correlations. The economic analysis used single-point values for energy prices, carbon prices, and the nitric acid market price, all of which are volatile. Sensitivity analyses presented in Figure 6, Figure 7 and Figure 8 partially address this, but do not account for correlated price scenarios or long-term structural shifts in the EU ETS.
The study investigates one specific dual-pressure plant configuration under nominal full-load conditions. The generalisability of the results to plants of different capacity, pressure configuration, or geographic and regulatory context is limited. The global impact extrapolations presented in Section 4.5 rely on literature-derived industry-average emission factors and should be regarded as indicative rather than predictive. Validation of the retrofit options on additional plant configurations and under part-load conditions would strengthen the basis for broader recommendations.
4.7. Future Works
The present work evaluates tail gas treatment options within the existing thermal infrastructure of the plant, treating the heat exchanger network as fixed. A combined approach, simultaneously redesigning the heat recovery system and the tail gas treatment configuration using pinch analysis or mathematical programming, would likely reveal additional energy savings not captured here. Prior work on heat integration in nitric acid plants has identified utility savings of up to 14% through network retrofit alone [23]. Synergistic optimisation with selective catalytic abatement could amplify this potential, particularly for Option 1, where the combustion chamber introduces a significant high-temperature heat source that could be further exploited.
Option 1 increases steam generation from 64.1 to 70.0 t/h while reducing steam consumption to 29.0 t/h, creating a substantial exportable steam surplus that was not fully optimised in the current study. A detailed investigation of steam turbine performance, including off-design efficiency curves, back-pressure regulation, and the potential for additional power generation, could enhance the energy and economic case for Option 1. This is particularly relevant at sites where electricity prices are high or where cogeneration incentives apply.
Nitric acid plants typically operate as part of integrated fertiliser complexes producing ammonium nitrate or other downstream products. The utility streams identified in this study, including surplus steam, hot tail gas, and recoverable heat from the combustion chamber, represent potential inputs to adjacent process units such as ammonium nitrate evaporators or granulation systems. Integration at the site level could improve overall energy efficiency and reduce total utility consumption beyond what is achievable within the boundary of the nitric acid unit alone.
As noted in Section 4.6, the steady-state model does not capture transient behaviour during start-up, shutdown, load variation, or catalyst ageing. A dynamic simulation model would enable investigation of control strategies for maintaining stable catalyst ignition temperature under variable load, quantification of peak emission events during transient periods, and identification of operational bottlenecks that limit performance under off-design conditions. This is of direct industrial relevance given that regulatory emission limits apply continuously, not only at nominal load.
The progressive substitution of conventional grey ammonia with green ammonia, produced via electrolysis-based hydrogen and renewable electricity, would substantially reduce the upstream carbon intensity of nitric acid synthesis. Combined with the tail gas treatment measures demonstrated in this study, a green ammonia feedstock pathway offers a route to near-zero lifecycle N₂O and CO₂ emissions. A techno-economic assessment of this integrated pathway, including sensitivity to renewable electricity cost and carbon pricing, would provide the quantitative basis needed to support investment decisions aligned with sustainable development goals [39]. Policy instruments such as the EU's Farm to Fork Strategy and climate-smart agriculture programmes increasingly incentivise such transitions, but region-specific economic analysis and reliable emissions data remain prerequisites for widespread adoption.
5. Conclusion
The principal contribution of this study is demonstrating that retrofitting selective catalytic tail gas treatment into a mature dual-pressure nitric acid plant is an economically self-funding decarbonisation measure, in which the financial returns from emission cost avoidance, utility savings, and production gains are sufficient to recover the capital investment within months, not years. This finding shifts the framing of tail gas abatement from a regulatory compliance cost to a value-generating retrofit, with implications for how operators, policymakers, and investors approach emission reduction in the nitrogen fertiliser sector.
The two retrofit configurations studied reveal a fundamental design principle that extends beyond the specific plant investigated: there is no universal optimum between thermal integration and throughput expansion. Option 2, which achieves temperature control through internal catalytic oxidation of fuel gas in a two-shelf reactor, shows that a purely thermodynamic retrofit can deliver a 43% reduction in CO₂-equivalent emissions and a 2.6-month payback period at a capital cost below 1.35 million EUR, without requiring additional electricity or supplementary combustion infrastructure. Option 1, by contrast, sacrifices energy economy to unlock a 5% increase in plant throughput, worth 5.75 million EUR per year in additional revenue, making it the rational choice when production capacity is the strategic constraint. The coexistence of two commercially viable yet strategically distinct solutions within the same plant boundary confirms that the selection of abatement technology cannot be decoupled from the operator's production and investment objectives, a finding absent from prior single-option assessments in the literature.
From a thermodynamic standpoint, the results challenge a persistent assumption in nitric acid process design: that tail gas treatment is thermally parasitic on the gas turbine cycle. Both retrofit options demonstrate that selective catalytic reduction, when properly integrated, either preserves or enhances the steam balance of the plant: Option 1 increases steam generation by 9% while reducing consumption by 30%, and Option 2 maintains the base-case steam surplus. The non-selective catalytic systems that these options replace imposed a strict thermal constraint through their dependence on residual oxygen content for temperature control. Selective catalysts, by decoupling purification chemistry from combustion thermodynamics, restore degrees of freedom in the energy system that have been underutilised in the legacy plant design for three decades.
The N₂O emission factors achieved, 0.25 and 0.24 kg N₂O per tonne HNO₃ for Options 1 and 2 respectively, approach or meet the best-practice crediting threshold of 0.2 kg N₂O per tonne HNO₃ established under the UNFCCC Article 6.4 mechanism and fall significantly below the IPCC default emission factor of 7 kg N₂O per tonne for unabated medium-pressure plants. Applied across the global fleet of unabated dual-pressure plants, representing conservatively 30% of the 60 Mt per year global production base, retrofit at equivalent performance would reduce sectoral N₂O emissions by approximately 21.5 Mt CO₂-equivalent per year, more than half the estimated total unabated industry mitigation potential of 22.5 Mt CO₂-equivalent identified for 2020. This places selective catalytic tail gas treatment among the highest-leverage, lowest-cost mitigation opportunities available to the industrial sector in the near term.
The wider significance of this work lies in its evidence that decarbonisation and industrial competitiveness are not in tension at the plant level; they are structurally aligned. The barriers to adoption of proven abatement technology in the global nitric acid industry are therefore not technical or economic, but institutional: variability in carbon pricing, absence of mandatory tertiary abatement requirements in many jurisdictions, and insufficient integration of tail gas treatment into plant-level energy optimisation frameworks. Closing these gaps, through binding emission standards, carbon market expansion, and the kind of integrated digital-twin-based design methodology applied here, holds the potential to deliver emission reductions at a scale and speed that significantly exceed what agricultural and land-use interventions can achieve in the same timeframe, at a fraction of the systemic cost.
Nomenclature
| Latin symbols: | |
| a, b, α | coefficients |
| hin | mass enthalpy of inlet process stream, kJ/kg |
| hout | mass enthalpy of outlet process stream, kJ/kg |
| i | component in liquid phase of chemical mixture |
| κ | function of the acentric factor and reduced temperature, n/d |
| κ0 | function of the acentric factor and reduced temperature, n/d |
| κ1 | parameter of pure component, n/d |
| Min | mass flow of inlet streams, kg/h |
| Mout | mass flow of outlet streams, kg/h |
| Mlosses | mass losses, kg/h |
| p | pressure, Pa |
| PC | critical pressure, Pa |
| QS | capacity factor of new equipment |
| R | gas constant, J/(mole K) |
| T | absolute temperature, °C |
| TC | critical temperature, °C |
| Vm | molar volume, m3/mole |
| xi | mole fraction of component i |
| Greek symbols: | |
| α | temperature function |
| αij | non-randomness parameter |
| ω | acentric factor, n/d |
| γI | activity coefficient |
| gij | interaction coefficient for components i and j |
| Chemical symbols: | |
| C | carbon |
| CH4 | methane |
| CO | carbon monoxide |
| CO2 | carbon dioxide |
| H2 | hydrogen |
| H2O | water |
| HNO3 | nitric acid |
| N2 | nitrogen |
| NO | nitrogen monoxide |
| NO2 | nitrogen dioxide |
| N2O4 | nitrogen tetroxide |
| N2O | nitrous oxide |
| NH3 | ammonia |
| O2 | oxygen |
| Abbreviations: | |
| PFD | process flow diagram |
| NRTL | non-random two-liquid |
| CAPEX | capital expenditure |
| AACE | association for the advancement of cost engineering |
| STD | standard |
| EUR | Euro |
References
- Vallero, D.A. Chapter 8 - Air Pollution Biogeochemistry. In Air Pollution Calculations; Vallero, D.A., Ed.; Elsevier: Netherlands, 2019; pp. 175–206.
- Kirova-Yordanova, Z. Application of the Exergy Method to the Environmental Impact Estimation: The Nitric Acid Production as a Case Study. Energy 2011, 36, 3733–3744.
- Nascimento, G.R.O.; Dangelo, J.V.H. Operating Parameters Analysis of a Nitric Acid Plant to Increase Production and Reduce NOx Gases Emission. Chem. Eng. Process. - Process Intensif. 2024, 196, 109662. [CrossRef]
- Grande, C.A.; Andreassen, K.A.; Cavka, J.H.; Waller, D.; Lorentsen, O.-A.; Øien, H.; Zander, H.-J.; Poulston, S.; García, S.; Modeshia, D. Process Intensification in Nitric Acid Plants by Catalytic Oxidation of Nitric Oxide. Ind. Eng. Chem. Res. 2018, 57, 10180–10186. [CrossRef]
- Pérez-Ramı́rez, J.; Kapteijn, F.; Schöffel, K.; Moulijn, J.A. Formation and Control of N2O in Nitric Acid Production. Appl. Catal. B Environ. 2003, 44, 117–151. [CrossRef]
- Inger, M.; Moszowski, B.; Ruszak, M.; Rajewski, J.; Wilk, M. Two-Stage Catalytic Abatement of N2O Emission in Nitric Acid Plants. Catalysts 2020, 10, 987. [CrossRef]
- Clariant EnviCat N2O-S Catalyst to Cut CO2eq by 690,000 Tonnes/y at Hengli’s Nitric Acid Plant in China. Focus Catal. 2024, 2024, 6. [CrossRef]
- Clariant EnviCat N2O-S Catalyst Expected to Cut 275,000 Tonnes/y CO2eq at Sichuan Lutianhua Nitric Acid Plant. Focus Catal. 2025, 2025, 5. [CrossRef]
- Buttignol, F.; Rentsch, D.; Alxneit, I.; Garbujo, A.; Biasi, P.; Kröcher, O.; Ferri, D. Aging of Industrial Fe-Zeolite Based Catalysts for Nitrous Oxide Abatement in Nitric Acid Production Plants. Catal. Sci. Technol. 2022, 12, 7308–7321. [CrossRef]
- van den Brink, R.W.; Booneveld, S.; Verhaak, M.J.F.M.; de Bruijn, F.A. Selective Catalytic Reduction of N2O and NOx in a Single Reactor in the Nitric Acid Industry. Catal. Today 2002, 75, 227–232. [CrossRef]
- European Commission. Best Available Techniques for the Manufacture of Large Volume Inorganic Chemicals - Ammonia, Acids and Fertilisers. 2007.
- van den Brink, R.W.; Booneveld, S.; Pels, J.R.; Bakker, D.F.; Verhaak, M.J.F.M. Catalytic Removal of N2O in Model Flue Gases of a Nitric Acid Plant Using a Promoted Fe Zeolite. Appl. Catal. B Environ. 2001, 32, 73–81. [CrossRef]
- Inger, M.; Rajewski, J.; Ruszak, M.; Wilk, M. The Influence of NOx Presence on the Catalytic N2O Decomposition over the Supported Double-Promoted Cobalt Spinel Catalyst. Chem. Pap. 2019, 73, 1979–1986. [CrossRef]
- Groves, M.C.E.; and Sasonow, A. Uhde EnviNOx® Technology for NOX and N2O Abatement: A Contribution to Reducing Emissions from Nitric Acid Plants. J. Integr. Environ. Sci. 2010, 7, 211–222. [CrossRef]
- Qi, J.; Qi, X.; Pan, Y.; Cui, J.; Xiong, Y.; Shan, W.; Yu, H. Sm Doped NiO Catalysts with Excellent H2O Resistance for N2O Decomposition under Simulated Nitric Acid Plant Exhaust Condition. Appl. Surf. Sci. 2023, 611, 155657. [CrossRef]
- Capała, P.; Ruszak, M.; Rudawska, A.; Inger, M.; Wilk, M. The Technology of Tail Gases Purifying in Nitric Acid Plants and Design of deN2O and deNOx Reactors—Review. Appl. Sci. 2023, 13, 7492. [CrossRef]
- Chatterjee, I.B.; Joshi, J.B. Modeling, Simulation and Optimization: Mono Pressure Nitric Acid Process. Chem. Eng. J. 2008, 138, 556–577. [CrossRef]
- Yadav, D.R.K. Study of Simulation of Nitric Acid Production Using HYSYS Simulation Software. International Journal of Engineering, Science and Mathematics. 2017, 6, 288-294.
- Abbasian Hamedani, E.; Abdalisousan, A.; Khoshgard, A.; Nazari, M. Energy, Exergy, and Sustainability Analysis of an Industrial Nitric Acid Plant. Energy Sources Part Recovery Util. Environ. Eff. 2023, 45, 10952–10970. [CrossRef]
- Chatterjee, I.B.; Joshi, J.B. Modeling, Simulation and Optimization: Mono Pressure Nitric Acid Process. Chem. Eng. J. 2008, 138, 556–577. [CrossRef]
- Abbasian Hamedani, E.; Hamidzadeh, Z.; Mousavi, S.A.; Kariman, A.; Mahnesaei, A. Simulation of a Nitric Acid Production Unit in Aspen Hysys. In Proceedings of 9th International Conference on Technology and Energy Management, Behshahr, Mazandaran, Iran, 14-15 February, 2024.
- Mukhitdinov, D.; Sattarov, O.; Akhmatov, A.; Abdullayeva, D.; Bekchanov, E. Computer Simulation and Optimization of the Oxidation Process in the Production of Nitric Acid in the Aspen Plus Environment. E3S Web Conf. 2023, 417, 05004. [CrossRef]
- Ivaniš, G.; Lazarevic, M.; Radovic, I.; Kijevcanin, M. Energy Integration of Nitric Acid Production Using Pinch Methodology. Hem. Ind. 2014, 69, 39–39. [CrossRef]
- Steltenpohl, P.; Graczová, E. Application of Extended NRTL Equation for Ternary Liquid-Liquid and Vapor-Liquid-Liquid Equilibria Description. Chem. Pap. 2010, 64, 310–317. [CrossRef]
- Stryjek, R.; Vera, J.H. PRSV: An Improved Peng—Robinson Equation of State for Pure Compounds and Mixtures. Can. J. Chem. Eng. 1986, 64, 323–333. [CrossRef]
- Abu-Eishah, S.I. Modification of the Predictive Capability of the PRSV-2 Equation of State for Critical Volumes of Binary Mixtures. Fluid Phase Equilibria 1999, 157, 1–16. [CrossRef]
- Aspen HYSYS, Process Simulation Software, AspenTech. Available online: https://www.aspentech.com/en/products/engineering/aspen-hysys (accessed on 18 March 2026).
- Smith R. Chemical Process Design and Integration, 2nd Edition, Wiley: Chichester, UK.
- Plant Cost Index Archives Available online: https://www.chemengonline.com/site/plant-cost-index/ (accessed on 18 March 2026).
- Peters, M.S.; Timmerhaus, K.D.; West, R.E. Plant Design and Economics for Chemical Engineers; 5th ed.; McGraw-Hill: New York, US, 2003.
- Quaschning, V. Specific Carbon Dioxide Emissions of Various Fuels. Available online: https://www.volker-quaschning.de/datserv/CO2-spez/index.php (accessed on 18 March 2026).
- Sims, R.E.H.; Schock, R.N.; Adegbululgbe, A.; Fenhann, J.; Konstantinaviciute, I.; Moomaw, W.; Nimir, H.B.; Schlamadinger, B.; Torres-Martínez, J.; Turner, C.; Uchiyama, Y.; Vuori, S.J.V.; Wamukonya, N.; Zhang, X. 2007: Energy supply. In Climate Change 2007: Mitigation. Contribution of Working Group III to the Fourth Assessment Report of the Intergovernmental Panel on Climate Change; B. Metz, O.R. Davidson, P.R. Bosch, R. Dave, L.A. Meyer Eds.; Cambridge University Press: Cambridge, United Kingdom and New York, NY, USA.
- Natural Gas Rates. Available online: https://www.kitchenerutilities.ca/en/rates/natural-gas-rates.aspx (accessed on 18 March 2026).
- CO2 Equivalents. Climate Change Connection. Available online: https://climatechangeconnection.org/emissions/co2-equivalents/ (accessed on 18 March 2026).
- Electricity Price Statistics. Available online: https://ec.europa.eu/eurostat/statistics-explained/index.php?title=Electricity_price_statistics (accessed on 18 March 2026).
- Business analytiq. Nitric Acid Price Index. Available online: https://businessanalytiq.com/procurementanalytics/index/nitric-acid-price-index/(accessed on 19 June 2026).
- Sandbag. Carbon Price Viewer. Available online: https://sandbag.be/carbon-price-viewer/ (accessed on 18 March 2026).
- Sun, L.; Doyle, S.; Smith, R. Understanding Steam Costs for Energy Conservation Projects. Appl. Energy 2016, 161, 647–655. [CrossRef]
- Neumann, N.C.; Baumstark, D.; López Martínez, P.; Monnerie, N.; Roeb, M. Exploiting Synergies between Sustainable Ammonia and Nitric Acid Production: A Techno-Economic Assessment. J. Clean. Prod. 2024, 438, 140740. [CrossRef]
Figure 1.
Process flow diagram (PFD) of the examined selective gas treatment options: (a) Option #1; (b) Option #2. 1 – gas treatment reactor; 2 – air compressor; 3 – combustion chamber; 4 – ammonia evaporator; 5 – ammonia filter; 6 – ammonia heater.
Figure 1.
Process flow diagram (PFD) of the examined selective gas treatment options: (a) Option #1; (b) Option #2. 1 – gas treatment reactor; 2 – air compressor; 3 – combustion chamber; 4 – ammonia evaporator; 5 – ammonia filter; 6 – ammonia heater.
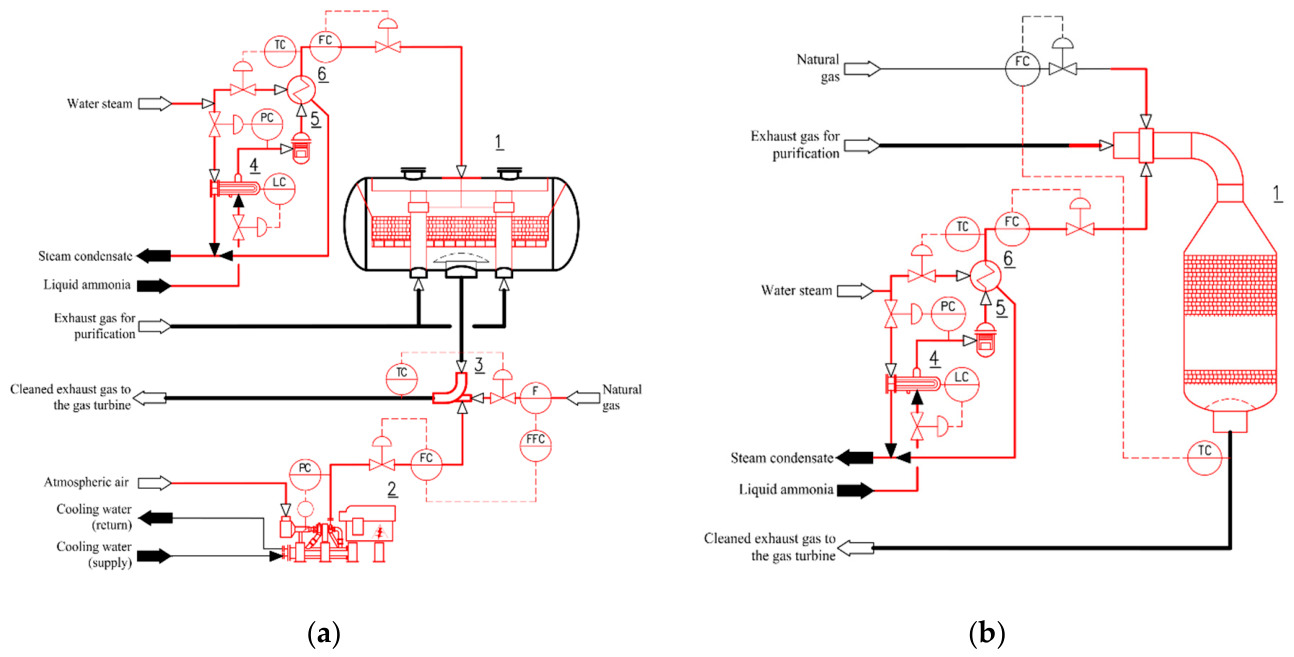
Figure 2.
Simulation PFD of the existing dual-pressure nitric acid plant. A – adjustment of parameters; CW – cooling water; E – heat exchanger; MIX – stream mixer; TEE – stream splitter; P – pump; Q – electricity; R – reactor; RCL – process recycle; S – parameter set; T – sub-flowsheet.
Figure 2.
Simulation PFD of the existing dual-pressure nitric acid plant. A – adjustment of parameters; CW – cooling water; E – heat exchanger; MIX – stream mixer; TEE – stream splitter; P – pump; Q – electricity; R – reactor; RCL – process recycle; S – parameter set; T – sub-flowsheet.
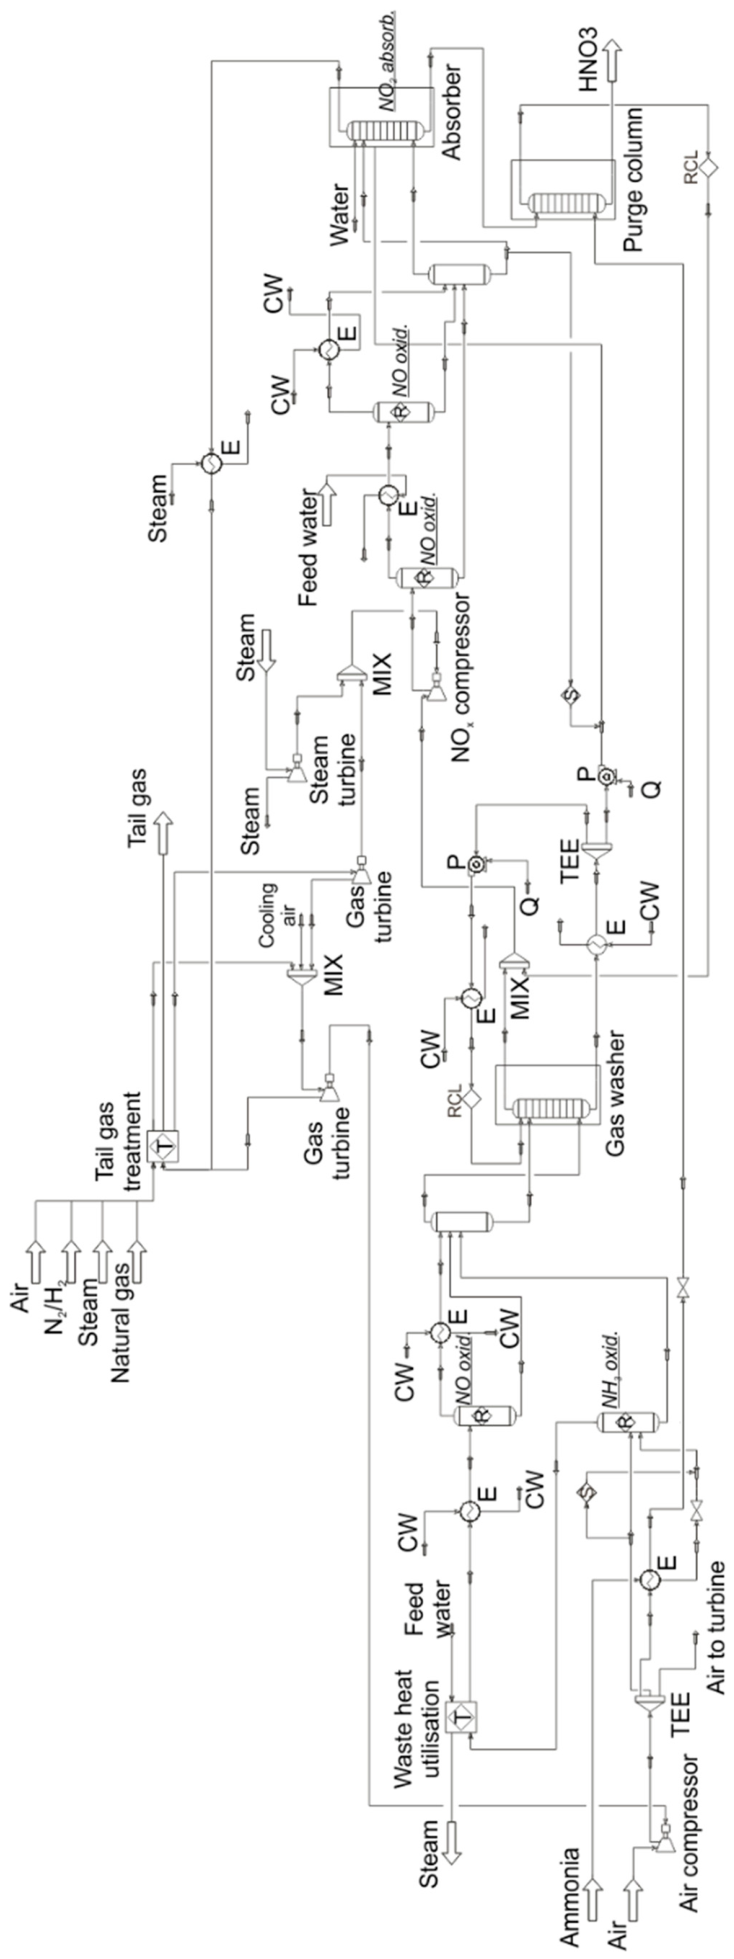
Figure 3.
Simulation PFDs of the existing waste heat utilisation (a) and tail gas treatment (b). A – adjustment of parameters; E – heat exchanger; MIX – stream mixer; TEE – stream splitter; P – pump; Q – electricity; R – reactor.; S – gas-liquid separator.
Figure 3.
Simulation PFDs of the existing waste heat utilisation (a) and tail gas treatment (b). A – adjustment of parameters; E – heat exchanger; MIX – stream mixer; TEE – stream splitter; P – pump; Q – electricity; R – reactor.; S – gas-liquid separator.
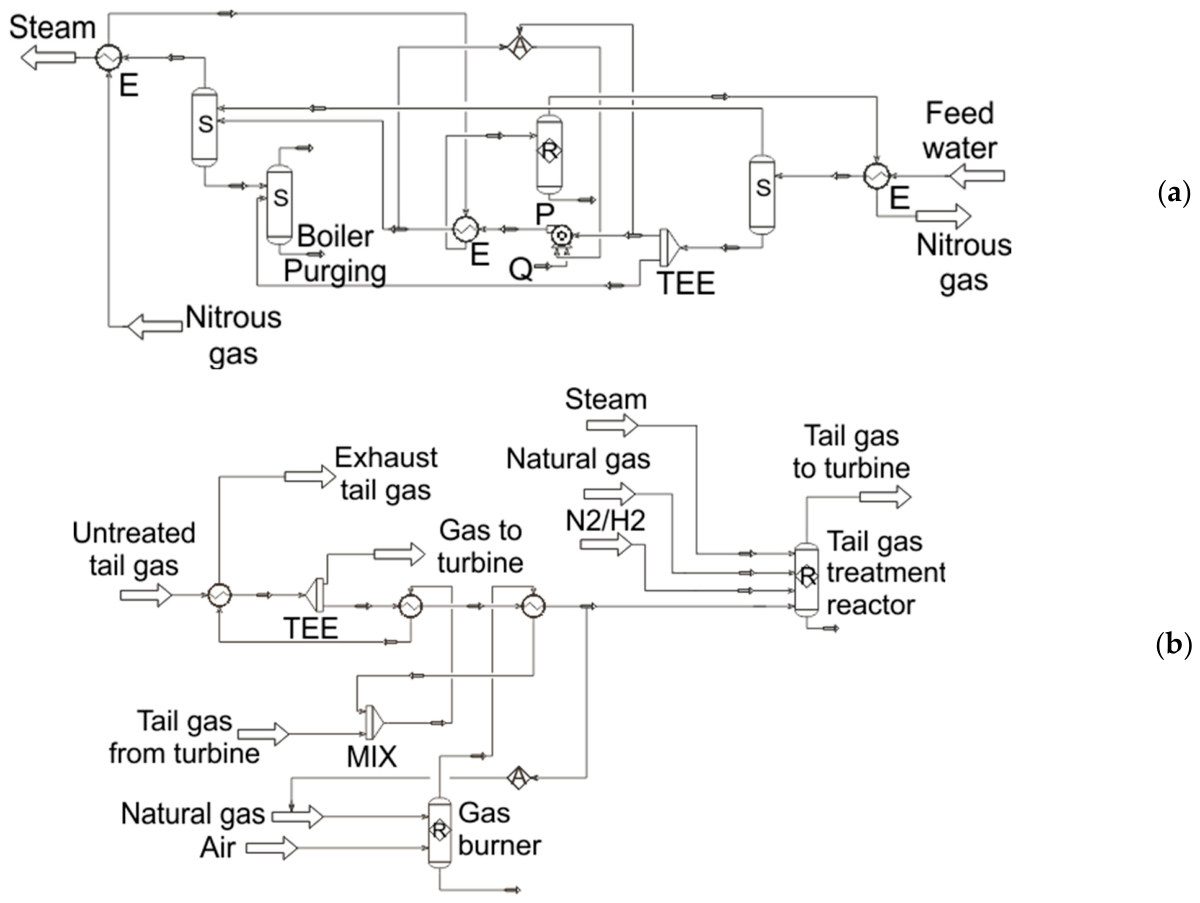
Figure 4.
Impact of tail gas treatment on plant yield.
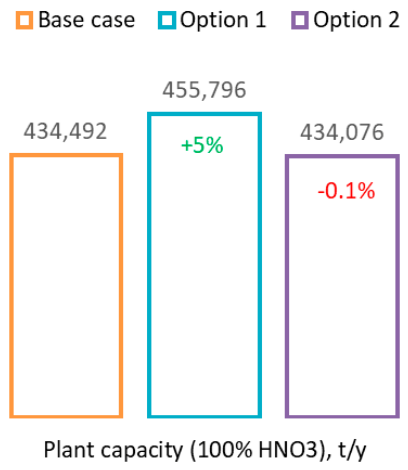
Figure 5.
Emissions for different options of tail gas treatment. a) direct nitrogen oxides emission; b) direct carbon dioxide emissions; c) total cumulative CO2 equivalent.
Figure 5.
Emissions for different options of tail gas treatment. a) direct nitrogen oxides emission; b) direct carbon dioxide emissions; c) total cumulative CO2 equivalent.
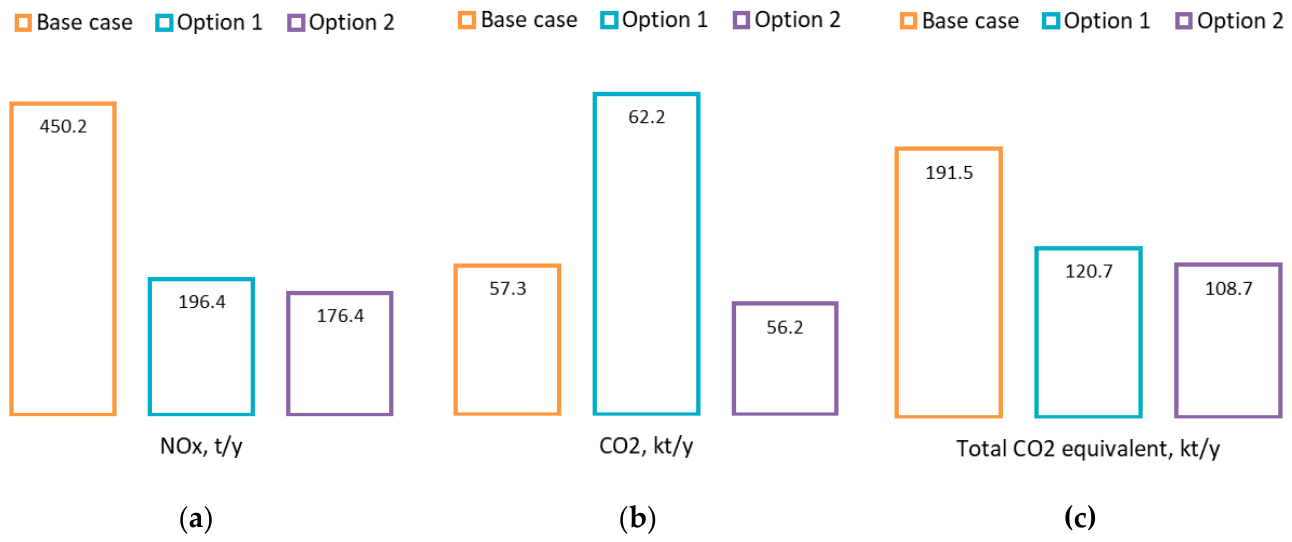
Figure 6.
Capex impact on economic performance for proposed tail gas treatment retrofit. (a) option #1; (b) option #2.
Figure 6.
Capex impact on economic performance for proposed tail gas treatment retrofit. (a) option #1; (b) option #2.
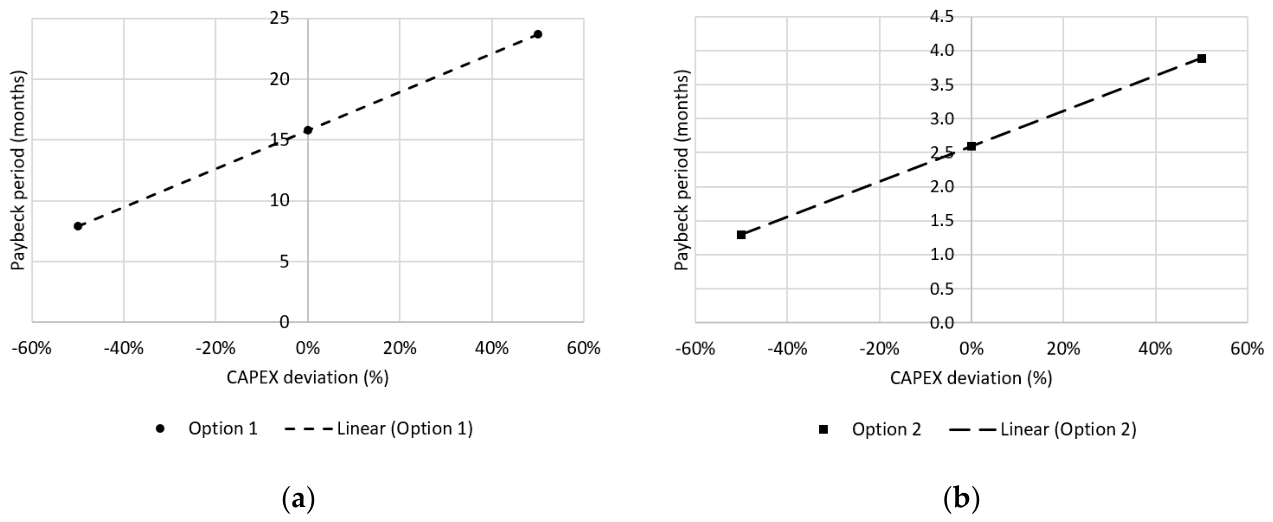
Figure 7.
Nitric acid price impact on economic performance for proposed tail gas treatment retrofit. (a) option #1; (b) option #2.
Figure 7.
Nitric acid price impact on economic performance for proposed tail gas treatment retrofit. (a) option #1; (b) option #2.
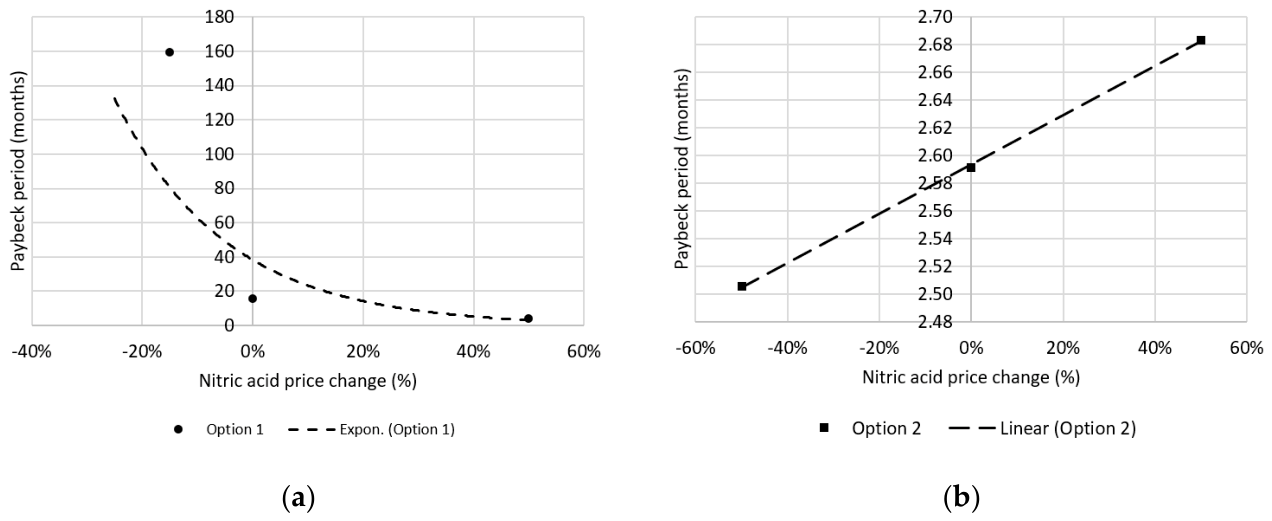
Figure 8.
Energy price impact on economic performance for proposed tail gas treatment retrofit. (a) option #1; (b) option #2.
Figure 8.
Energy price impact on economic performance for proposed tail gas treatment retrofit. (a) option #1; (b) option #2.
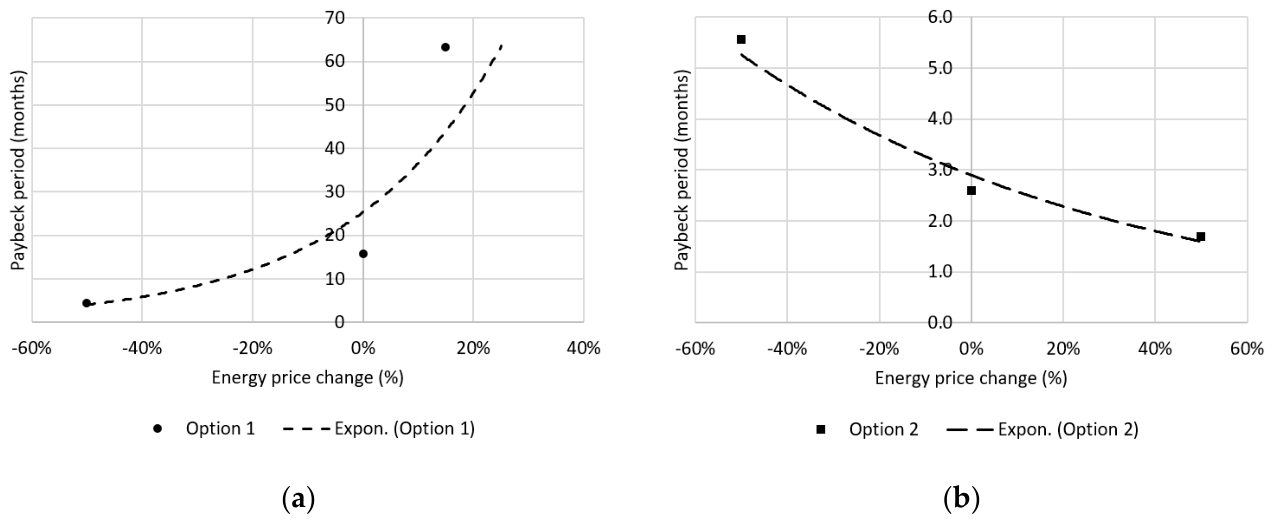

Table 1.
Mass balance of the simulated nitric acid plant.
| Feed streams (kg/h) | |
| Ammonia | 14,801 |
| Air to conversion reactor | 261,850 |
| Water to absorption column | 18,742 |
| Feed water | 74,800 |
| Natural gas to fire heater | 1,140 |
| Air to burning | 22,237 |
| N2/H2 mixture to gas treatment | 80 |
| Steam for gas treatment | 10,000 |
| Natural gas to gas treatment | 1,280 |
| Steam to turbine (2 MPa) | 31,400 |
| Total | 436,331 |
| Product streams (kg/h) | |
| Nitric acid (60%wt.) | 88,094 |
| Steam (4 MPa) | 64,134 |
| Boiler purging | 10,666 |
| Cooling air to turbines | 5,075 |
| Steam condensate | 31,400 |
| Total | 436,331 |
Table 2.
Measured and simulated process parameters of nitric acid plant (base case).
| Process parameters | Measured plant data | Simulation results | Deviation (%) | |
|---|---|---|---|---|
| Ammonia flow rate (kg/h) | 14,810 | 14,801 | -0.1% | |
| Feed water flow rate (kg/h) | 84,200 | 84,000 | -0.2% | |
| Conversion reactor temperature (°C) | 868 | 859 | -1.0% | |
| Ammonia/air ratio (% vol.) | 9.90 | 9.91 | 0.1% | |
| Ammonia conversion ratio (% mol.) | 96.0 | 96.0 | 0.0% | |
| Waste heat outlet gas temperature (°C) | 268.0 | 268.0 | 0.0% | |
| MP steam temperature(°C) | 447 | 444 | -0.7% | |
| Air compressor outlet pressure (kPa) | 418 | 418 | 0.0% | |
| Air compressor outlet temperature (°C) | 198 | 203 | 2.5% | |
| Nitrous compressor outlet pressure (kPa) | 1,072 | 1,072 | 0.0% | |
| Nitrous compressor outlet temperature (°C) | 195.0 | 194.7 | -0.2% | |
| Gas washer top temperature (°C) | 58.0 | 59.3 | 2.2% | |
| Gas washer bottom temperature (°C) | 63.0 | 63.4 | 0.6% | |
| NO2 absorption ratio (% mol.) | 99.0 | 99.1 | 0.1% | |
| Absorber top oxygen content (% mol.) | 2.40 | 2.40 | 0.0% | |
| Absorber top temperature (°C) | 28.0 | 28.0 | 0.0% | |
| Absorber bottom temperature (°C) | 45.0 | 44.8 | -0.4% | |
| Tail gas temperature before reactor (°C) | 529 | 529 | 0.0% | |
| Tail gas temperature after reactor (°C) | 777 | 770 | -0.9% | |
| Gas turbine outlet temperature (°C) | 418 | 426 | 1.9% | |
| Steam turbine outlet temperature (°C) | 291 | 291 | 0.0% | |
| MP steam consumption (t/h) | 31.4 | 31.4 | 0.0% | |
| NOx in the exhaust tail gas (ppm) | 190 | 181 | -4.7% | |
| Exhaust tail gas temperature (°C) | 237 | 259 | 9.3% | |
| HNO3 concentration (% mass.) | 59.20 | 59.17 | -0.1% | |
| Plant yield (t/h 100% HNO3) | 51.90 | 52.12 | 0.4% |
Table 3.
Utility consumption for different tail gas treatment options.
| Utility | Base case | Option 1 | Option 2 |
|---|---|---|---|
| Natural gas, STD m3/h | 3,528 | 3,763 | 3,379 |
| N2/H2 mixture, STD m3/h | 221.0 | 0.0 | 0.0 |
| NH3, STD m3/h | - | 127.0 | 123.0 |
| Additional electricity, kW | - | 3,155 | 0.0 |
| Steam generation, t/h | 64.1 | 70.0 | 64.1 |
| Steam consumption, t/h | 41.4 | 29.0 | 31.5 |
Table 4.
The content of greenhouse gases in the exhaust tail gas (kg/h).
| Greenhouse gases | Base case | Option #1 | Option #2 |
|---|---|---|---|
| N2O | 39.2 | 13.0 | 12.4 |
| NO | 14.2 | 10.0 | 8.5 |
| NO2 | 0.7 | 0.6 | 0.3 |
| CO2 | 6,882 | 7,475 | 6,750 |
| NH3 | 2.4 | 0.0 | 0.0 |
Table 5.
Economic results of different tail gas treatment options.
| Economic parameter | Base case | Option #1 | Option #2 |
|---|---|---|---|
| CAPEX for retrofit, EUR | - | 4,771,557 | 1,340,663 |
| Discounted retrofit cost, EUR/y | - | 1,258,725 | 353,664 |
| Emission cost reduction1, EUR/y | - | 5,227,499 | 6,113,216 |
| Utility cost change, EUR/y | - | +4,794,569 | -1,750,090 |
| Revenue on capacity change, EUR/y | - | +5,752,166 | -112,347 |
| Discounted payback period, months (not accounting for emission cost) | - | 16 | 2.6 |
1 According to the EU Emissions Trading System
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2026 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (http://creativecommons.org/licenses/by/4.0/).
Copyright: This open access article is published under a Creative Commons CC BY 4.0 license, which permit the free download, distribution, and reuse, provided that the author and preprint are cited in any reuse.