

Submitted:
12 September 2025
Posted:
16 September 2025
You are already at the latest version
Abstract
This study investigates the tensile strength performance of titanium-polylactic acid (PLA) composites fabricated via fused deposition modeling (FDM) compared to pure PLA under identical manufacturing conditions. The aim is to identify whether surface integration and material combination strategies enhance the load-bearing capacity of polymer components. PLA filaments of 1.75mm diameter were used, and the Taguchi Design of Experiments (DOE) with an orthogonal L9 array was employed to assess the impact of process parameters such as printing temperature, bed temperature, and layer height on the Ultimate Tensile Strength (UTS). Surface treatments, including laser structuring and sandblasting, were applied to selected titanium surfaces to study their effect on interfacial adhesion. Tensile tests were performed using a Universal Testing Machine, and statistical analysis was conducted using SPSS software. The results revealed a statistically significant difference in strength between the two materials, with titanium-PLA composites exhibiting significantly higher strength than pure PLA. The material type significantly influenced strength, with 98.2% of the variance in strength attributable to the material type. However, the material type did not significantly affect strength across the parameters of printing temperature, bed temperature, and layer height. The findings support the development of stronger and more reliable hybrid structures for structural and lightweight applications.
Keywords:
1. Introduction
2. Materials and Methods
2.1. Printing Materials
2.2. Design of Experiment (DOE)
2.3. Specimen Printing

| Name of parameter | Value |
|---|---|
| Model | Raise 3D |
| Working area (mm) | 330mm x 340mm x4mm |
| Nozzle diameter (mm) | 0.4 |
| Infill pattern | Grid |
| Infil percentages (%) | 100 |
| Shell | 2 |
| Fan speed | 100% |
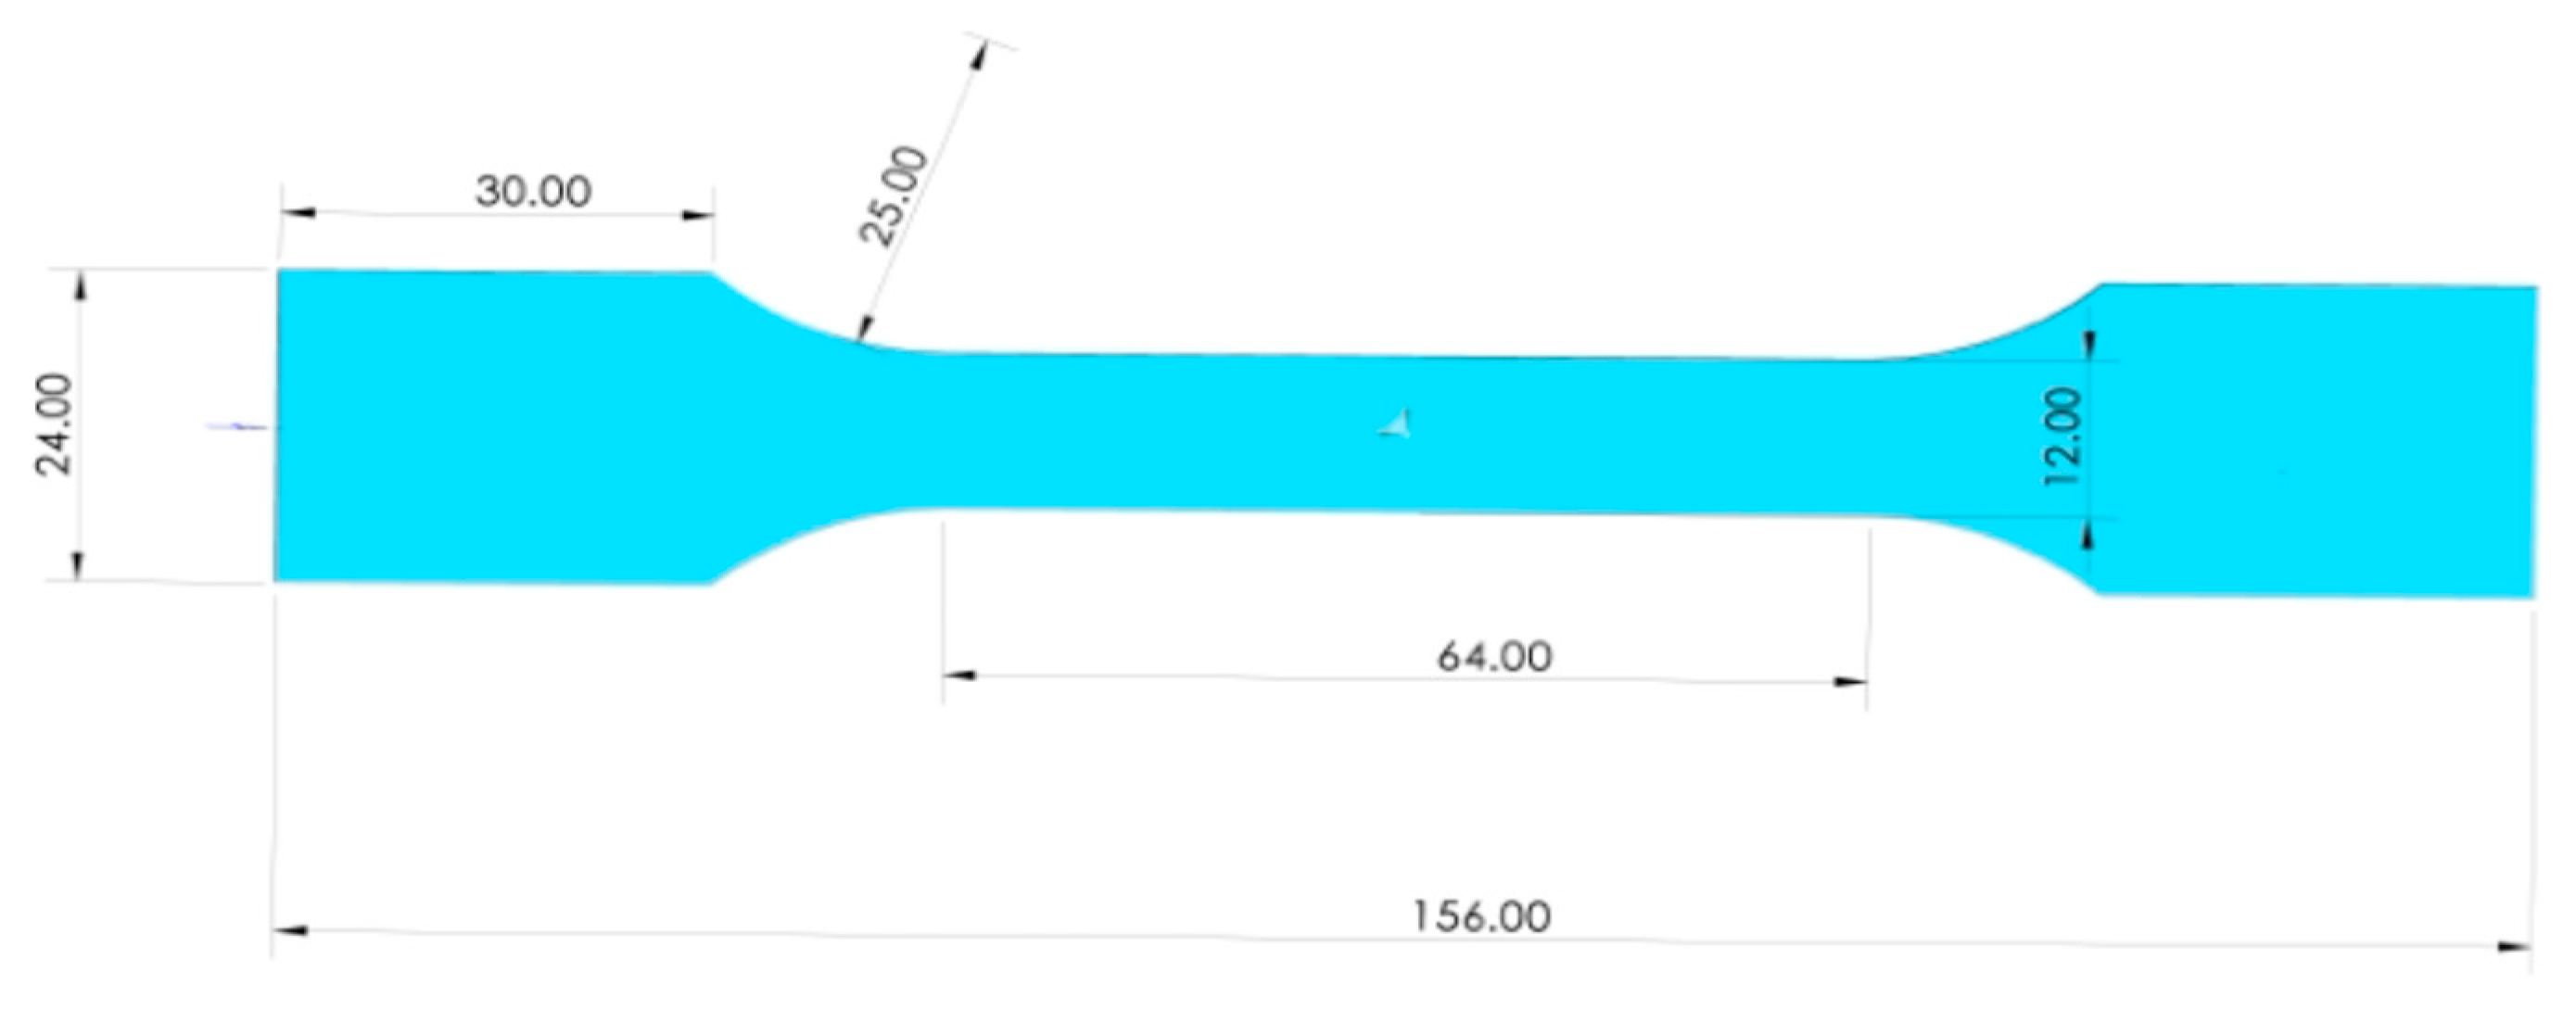
2.4. Tensile Test
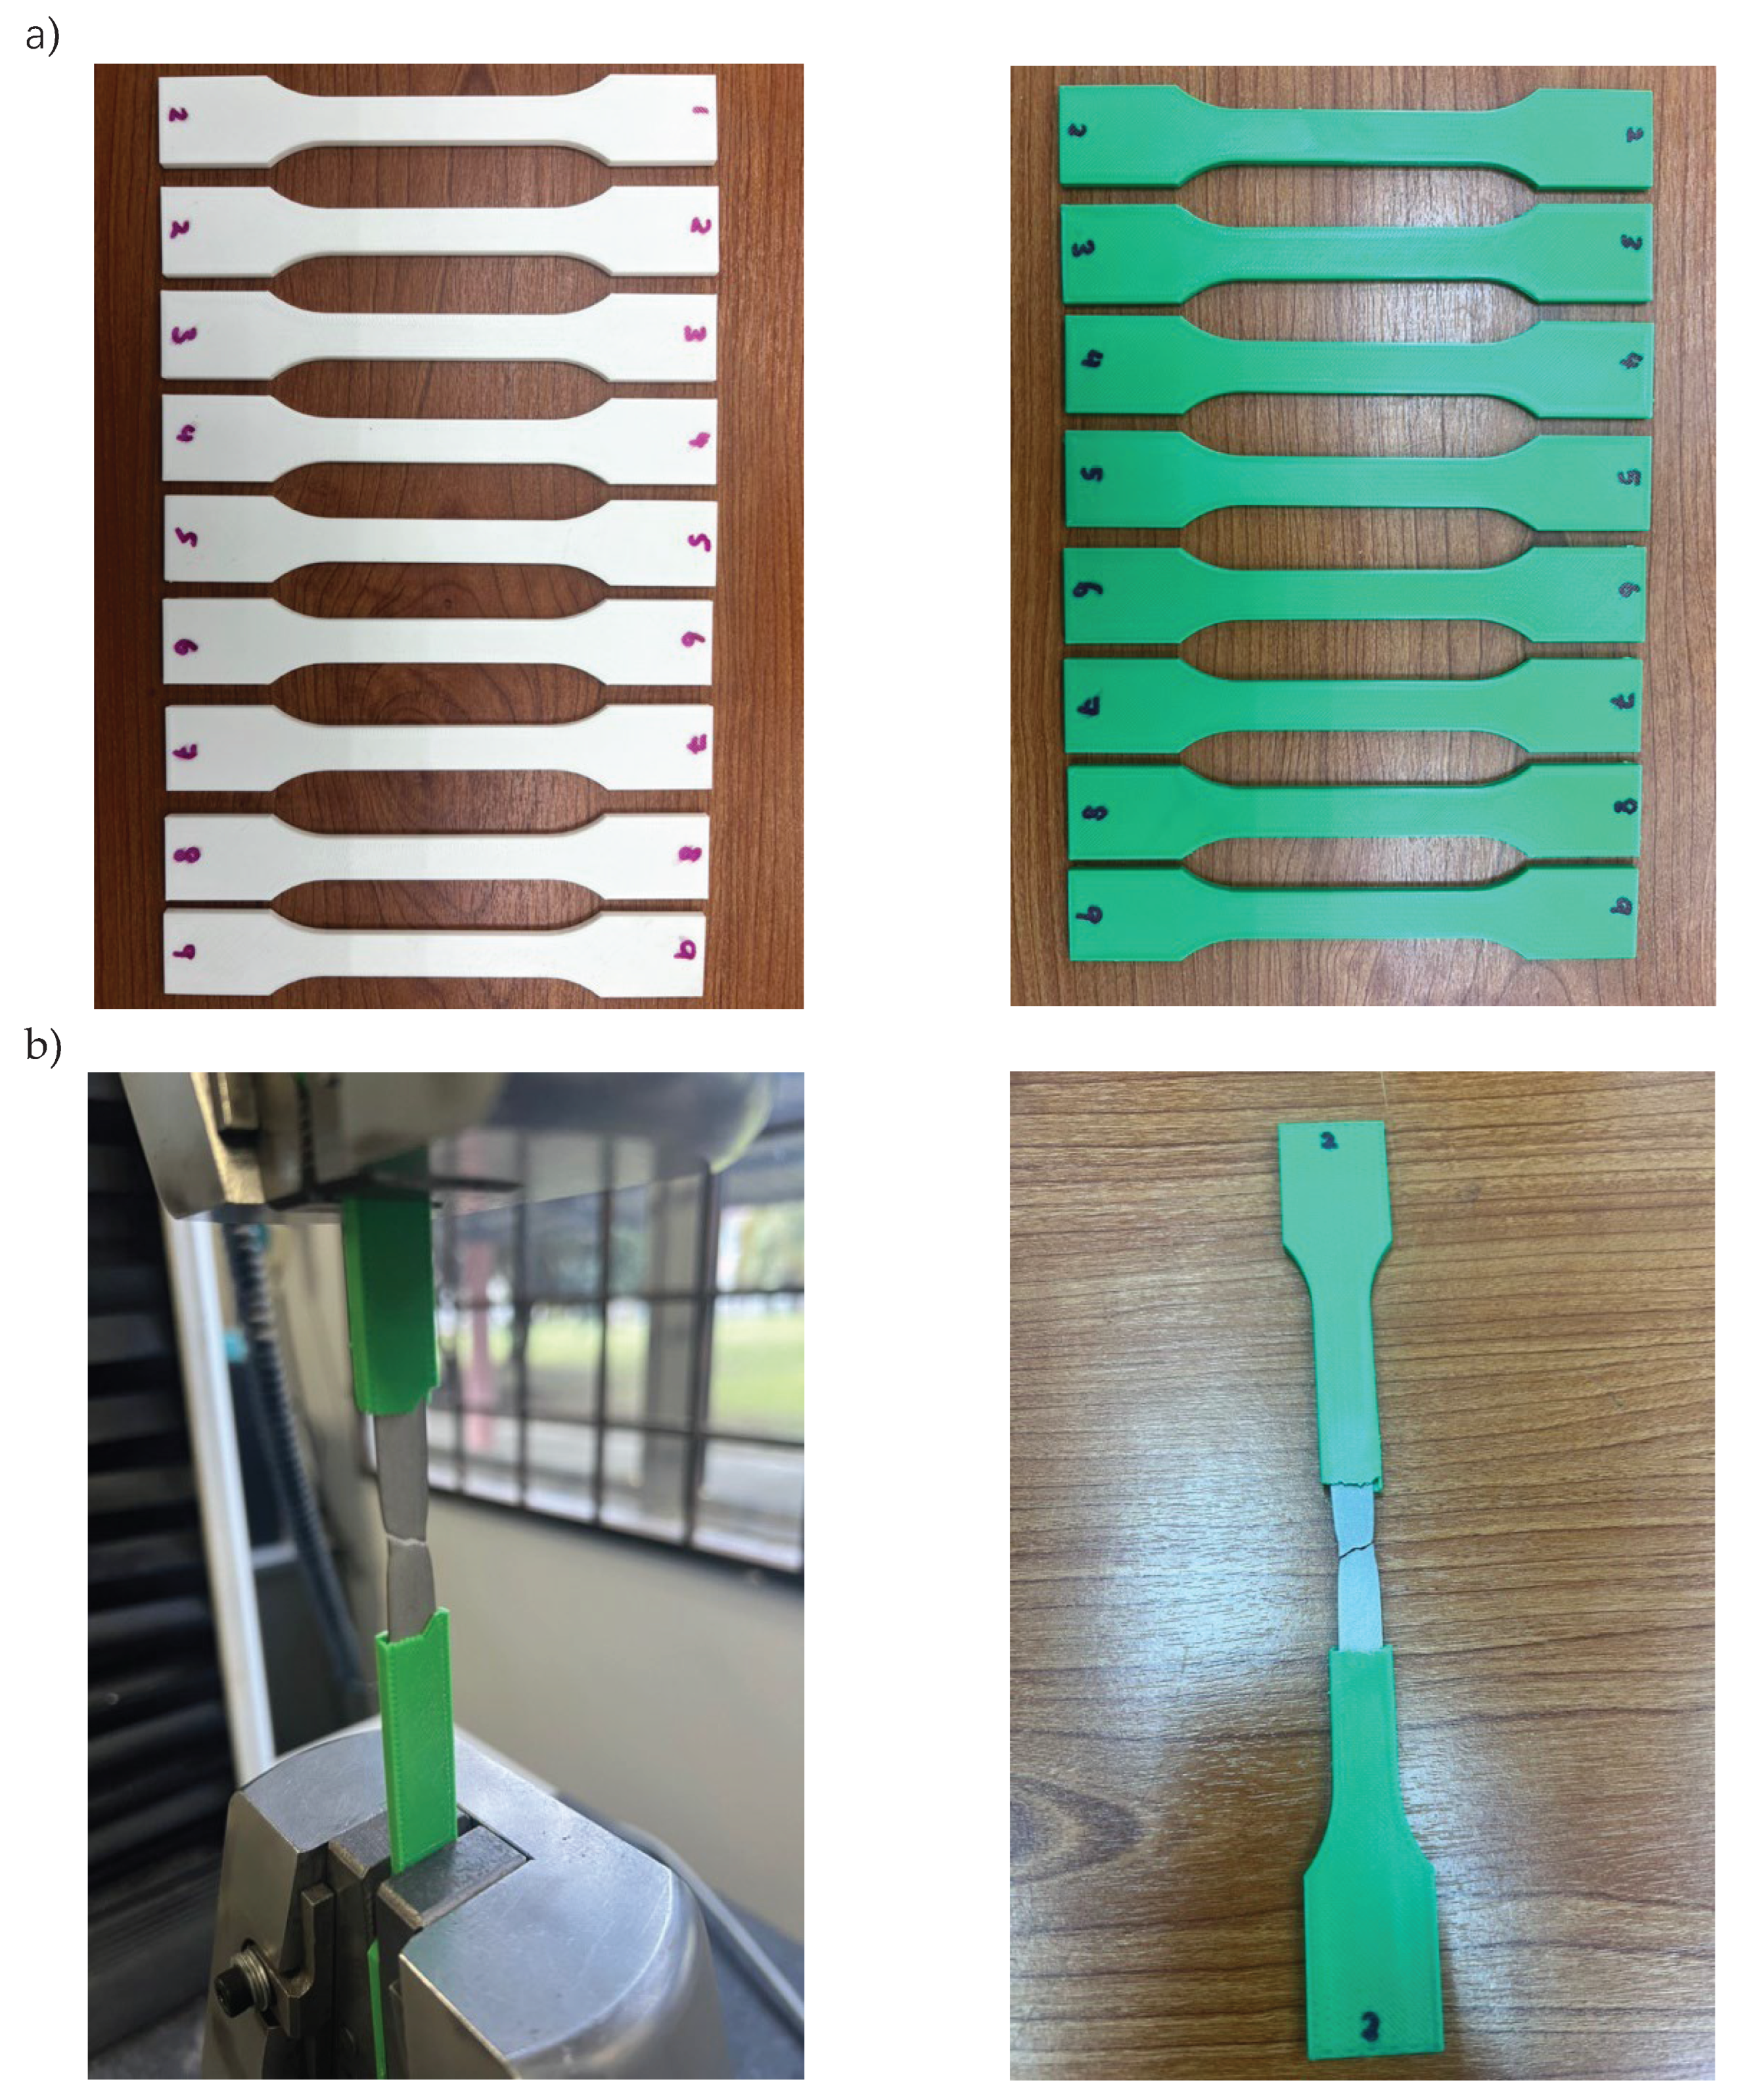
3. Results and Discussions
3.1. Experimental Result
| No | Parameter | Tensile | |||
| A | B | C | D | ||
| 1 | 50 | 180 | 50 | 0.1 | 0 |
| 2 | 50 | 200 | 60 | 0.15 | 95.29 |
| 3 | 50 | 220 | 70 | 0.2 | 108.86 |
| 4 | 50 | 180 | 60 | 0.2 | 104.58 |
| 5 | 50 | 200 | 70 | 0.1 | 107.83 |
| 6 | 50 | 220 | 50 | 0.15 | 104.69 |
| 7 | 50 | 180 | 70 | 0.15 | 125.5 |
| 8 | 50 | 200 | 50 | 0.2 | 118.72 |
| 9 | 50 | 220 | 60 | 0.1 | 109.85 |
| No | Parameter | Tensile | |||
| A | B | C | D | ||
| 1 | 50 | 180 | 50 | 0.1 | 34.35 |
| 2 | 50 | 200 | 60 | 0.15 | 34.73 |
| 3 | 50 | 220 | 70 | 0.2 | 36.72 |
| 4 | 50 | 180 | 60 | 0.2 | 36.15 |
| 5 | 50 | 200 | 70 | 0.1 | 35.32 |
| 6 | 50 | 220 | 50 | 0.15 | 36.55 |
| 7 | 50 | 180 | 70 | 0.15 | 29.69 |
| 8 | 50 | 200 | 50 | 0.2 | 29.51 |
| 9 | 50 | 220 | 60 | 0.1 | 32.31 |
3.2. Descriptive statistics
| Material | N | Mean Strength | Std.Deviation |
|---|---|---|---|
| PLA | 7 | 34.470 | 2.654 |
| CMT | 7 | 107.117 | 7.045 |
3.3. Independent Sample T-Test
| T-test for Equality of Means | t | df | Sig.(2-tailed) | Mean Difference | 95% CI (Lower) | 95% CI (Upper) |
|---|---|---|---|---|---|---|
| 25.529 | 12 | <.001 | 72.647 | 66.035 | 79.258 |
3.4. One Way ANOVA
| Comparison | Material | df (Between, Within) | F | p-value (Sig) | ∏2(Effect Size) | Significance (p<0.05) |
|---|---|---|---|---|---|---|
| PT | PLA | (2,12) | 0.567 | 0.607 | 0.2208 (large effect) | NOT SIGNIFICANT |
| CMT | (2,12) | 0.055 | 0.948 | 0.0266(small effect) | NOT SIGNIFICANT | |
| BT | PLA | (2,12) | 0.539 | 0.621 | 0.2121 (large effect) | NOT SIGNIFICANT |
| CMT | (2,12) | 0.869 | 0.486 | 0.3028 (large effect) | NOT SIGNIFICANT | |
| LH | PLA | (2,12) | 0.206 | 0.822 | 0.0934 (medium effect) | NOT SIGNIFICANT |
| CMT | (2,12) | 1.935 | 0.258 | 0.492 (large effect) | NOT SIGNIFICANT |
4.5. One Way ANOVA for material comparison
| Factor | Material | N | Mean | Std.Deviation | Df (Between/Within) | F-value | P-value | Effect Size (Cohen’s) | Significant | Conclusion |
|---|---|---|---|---|---|---|---|---|---|---|
| Material Comparison | PLA | 7 | 34.470 | 2.654 | (1,12) |
651.173 | <.001 | 0.982 (large effect) | Significant | PLA has lower strength |
| CMT | 7 | 107.117 | 7.045 | CMT has highest strength |
4. Conclusion
Author Contributions
References
- Ahmed, B. A. , Nadeem, U. , Hakeem, A. S., Ul-Hamid, A., Khan, M. Y., Younas, M., & Saeed, H. A. Printing Parameter Optimization of Additive Manufactured PLA Using Taguchi Design of Experiment. Polymers 2023, 15. [Google Scholar] [CrossRef]
- Alhmoudi, A. , Sheikh-Ahmad, J. , Almaskari, F., & Bojanampati, S. Joining of polymer to metal using material extrusion additive manufacturing. International Journal of Advanced Manufacturing Technology 2023, 129, 3303–3319. [Google Scholar] [CrossRef]
- Barakat, A. A. , Darras, B. M., Nazzal, M. A., & Ahmed, A. A. A Comprehensive Technical Review of the Friction Stir Welding of Metal-to-Polymer Hybrid Structures. Polymers 2023, 15. [Google Scholar] [CrossRef]
- Kolzunova, L. G. , Shchitovskaya, E. V, Lubimyi, N. S., Polshin, A. A., Gerasimov, M. D., Tikhonov, A. A., Antsiferov, S. I., Chetverikov, B. S., Ryazantsev, V. G., Brazhnik, J., & Ridvanov, I. (2022). Justification of the Use of Composite Metal-Metal-Polymer Parts for Functional Structures. [CrossRef]
- Kumaresan, R. , Samykano, M, Kadirgama, K., Ramasamy, D., Keng, N. W., & Pandey, A. K. 3D Printing Technology for Thermal Application: A Brief Review. Journal of Advanced Research in Fluid Mechanics and Thermal Sciences 2021, 83, 84–97. [Google Scholar] [CrossRef]
- Li, G. , Wang, Y., Liang, Y., Gao, P., Liu, X., Xu, W., & Yang, D. Microstructure and mechanical properties of laser welded Ti-6Al-4V (TC4) titanium alloy joints. 2024, 170. Optics and Laser Technology 2024, 170. [Google Scholar] [CrossRef]
- Maggiore, S. , Pedemonte, M., Bazurro, A., Stagnaro, P., Utzeri, R., & Luciano, G. Characterization of the effect of an epoxy adhesive in hybrid FSW-bonding aluminium-steel joints for naval application. International Journal of Adhesion and Adhesives 2020, 103. [Google Scholar] [CrossRef]
- Manola, M. S. , Singh, B., Singla, M. K., Chohan, J. S., Kumar, R., Kumar, R., Bisht, Y. S., Kumar, R., Alkahtani, M. Q., Islam, S., Ammarullah, M. I., Ammarullah, M. I., & Ammarullah, M. I. Investigation of melt flow index and tensile properties of dual metal reinforced polymer composites for 3D printing using machine learning approach: Biomedical and engineering applications. AIP Advances 2024, 14. [Google Scholar] [CrossRef]
- Ozlati, A. , Movahedi, M, Tamizi, M., Tartifzadeh, Z., & Alipour, S. An alternative additive manufacturing-based joining method to make Metal/Polymer hybrid structures. Journal of Manufacturing Processes 2019, 45, 217–226. [Google Scholar] [CrossRef]
- Pang, R. , Lai, M. K., Ismail, K. I., & Yap, T. C. Characterization of the Dimensional Precision, Physical Bonding, and Tensile Performance of 3D-Printed PLA Parts with Different Printing Temperature. Journal of Manufacturing and Materials Processing 2024, 8. [Google Scholar] [CrossRef]
- Plamadiala, I. , Croitoru, C., Pop, M. A., & Roata, I. C. Enhancing Polylactic Acid (PLA) Performance: A Review of Additives in Fused Deposition Modelling (FDM) Filaments. Polymers 2025, 17. [Google Scholar] [CrossRef]
- Rivera-López, F. , Pavón, M. M. L., Correa, E. C., & Molina, M. H. Effects of Nozzle Temperature on Mechanical Properties of Polylactic Acid Specimens Fabricated by Fused Deposition Modeling. Polymers 2024, 16. [Google Scholar] [CrossRef]
- Shahrjerdi, A. , Karamimoghadam, M., & Bodaghi, M. Enhancing Mechanical Properties of 3D-Printed PLAs via Optimization Process and Statistical Modeling. Journal of Composites Science 2023, 7. [Google Scholar] [CrossRef]
- Shanbhag, G. , Wheat, E., Moylan, S., & Vlasea, M. Effect of specimen geometry and orientation on tensile properties of Ti-6Al-4V manufactured by electron beam powder bed fusion. Additive Manufacturing 2021, 48. [Google Scholar] [CrossRef]
- Syrlybayev, D. , Zharylkassyn, B., Seisekulova, A., Akhmetov, M., Perveen, A., & Talamona, D. Optimisation of strength properties of FDM printed parts—A critical review. Polymers 2021, 13. [Google Scholar] [CrossRef]
- Vakharia, V. S. , Kuentz, L., Salem, A., Halbig, M. C., Salem, J. A., & Singh, M. Additive manufacturing and characterization of metal particulate reinforced polylactic acid (Pla) polymer composites. Polymers, 2021; 13. [Google Scholar] [CrossRef]
- Yeh, R. Y. , & Hsu, R. Q. Improving the adhesion of plastic/metal direct bonding by injection moulding using surface modifications. Advances in Materials and Processing Technologies 2016, 2, 21–30. [Google Scholar] [CrossRef]
| Property | Value |
|---|---|
| Diameter | 1.75 mm |
| Density | 1.22 g/cm3 |
| Melt Flow Index | 6 g/10min |
| Glass Transition temperature | 62°C |
| Melting Temperature | 150 °C |
| Tensile Strength | 36.5 + 0.6 Mpa |
| Young Modulus | 2633 + 117.4 Mpa |
| Parameter |
Level 1 (Low) |
Level 2 (Medium) |
Level 3 (High) |
| Printing Speed (˚C ) | 50 | 50 | 50 |
| Printing temperature (˚C ) | 180 | 200 | 220 |
| Bed temperature (˚C ) | 50 | 60 | 70 |
| Layer thickness (mm) | 0.1 | 0.15 | 0.2 |
| No. of samples/Factors | A | B | C | D |
|---|---|---|---|---|
| 1 | 50 | 180 | 50 | 0.1 |
| 2 | 50 | 200 | 60 | 0.15 |
| 3 | 50 | 220 | 70 | 0.2 |
| 4 | 50 | 180 | 60 | 0.2 |
| 5 | 50 | 200 | 70 | 0.1 |
| 6 | 50 | 220 | 50 | 0.15 |
| 7 | 50 | 180 | 70 | 0.15 |
| 8 | 50 | 200 | 50 | 0.2 |
| 9 | 50 | 220 | 60 | 0.1 |
Disclaimer/Publisher’s Note: The statements, opinions and data contained in all publications are solely those of the individual author(s) and contributor(s) and not of MDPI and/or the editor(s). MDPI and/or the editor(s) disclaim responsibility for any injury to people or property resulting from any ideas, methods, instructions or products referred to in the content. |
© 2025 by the authors. Licensee MDPI, Basel, Switzerland. This article is an open access article distributed under the terms and conditions of the Creative Commons Attribution (CC BY) license (http://creativecommons.org/licenses/by/4.0/).